With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Activated carbon granule material handling systems are specialized industrial equipment designed to efficiently transport and manage granular activated carbon in various applications. These systems are crucial for processes such as water treatment, air purification, and chemical processing, where activated carbon's high surface area and adsorption capacity are leveraged to remove impurities and contaminants. The primary objective of these systems is to ensure the smooth, reliable, and safe movement of activated carbon from storage to processing units, minimizing operational downtime and maximizing overall efficiency. By addressing the unique challenges associated with handling granular materials, these systems contribute significantly to the productivity and effectiveness of industrial facilities.
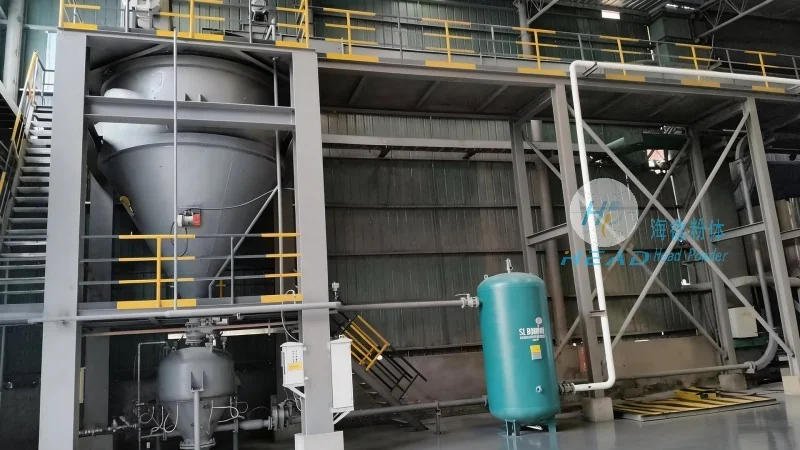
The operation of activated carbon granule material handling systems is based on several fundamental principles that govern their functionality. The choice of conveyor technology is a critical factor, as different systems are optimized for specific material characteristics and operational requirements. Screw conveyors, for instance, are commonly used for horizontal or slight incline transport due to their ability to handle bulk materials without complex mechanisms. They are particularly suitable for activated carbon granules with moderate to high bulk density, as the rotating screw pushes the material forward, reducing the risk of clogging. Belt conveyors are ideal for longer horizontal distances and larger material volumes, utilizing a continuous belt to transport granules. Pneumatic conveying systems offer a distinct approach, using air pressure to move granules through pipes, which is advantageous for vertical transport or when the material needs to be transferred over significant distances. The selection of the appropriate conveyor type is essential to maintain the integrity of the activated carbon granules, as excessive friction or impact can degrade their surface area and, consequently, their adsorption efficiency. Additionally, systems often incorporate control mechanisms, such as variable speed drives and material flow sensors, to regulate the transport process and prevent overloading or blockages.
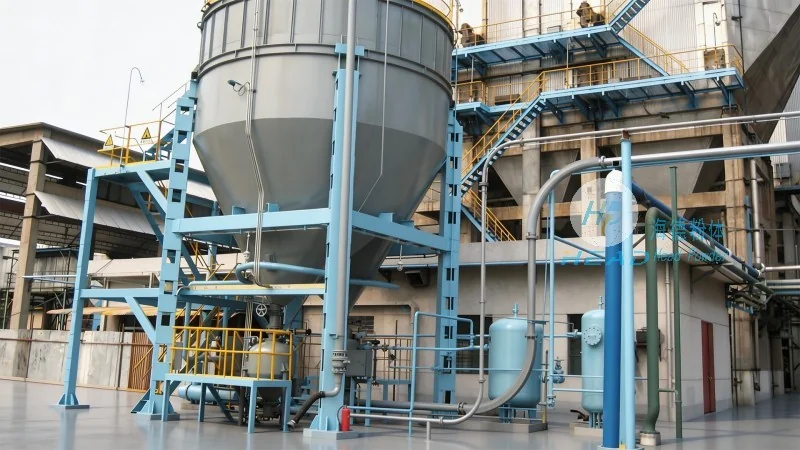
The working scene characteristics of activated carbon granule material handling systems vary widely based on the industrial environment in which they are deployed. In water treatment plants, these systems are integral to the filtration process, ensuring that activated carbon is efficiently transferred from storage silos to the filtration units. The systems must be capable of handling large volumes of granules and maintaining consistent flow rates to support continuous water treatment operations. In air purification systems, the equipment facilitates the movement of activated carbon to adsorption towers, where it plays a vital role in removing pollutants from industrial emissions. The working scene also includes considerations for safety and environmental compliance, as activated carbon is often used in processes that require strict adherence to regulatory standards. Additionally, in chemical processing plants, the systems are used in solvent recovery and waste treatment applications, where the precise handling of activated carbon is essential to achieve optimal results. The adaptability of these systems to different operational conditions, such as varying temperatures and humidity levels, further enhances their suitability for a broad range of applications, from food and beverage processing to pharmaceutical manufacturing. For example, in the power generation industry, activated carbon is used to treat flue gas emissions, and the material handling systems must be robust enough to handle the abrasive nature of the granules and the high temperatures involved.
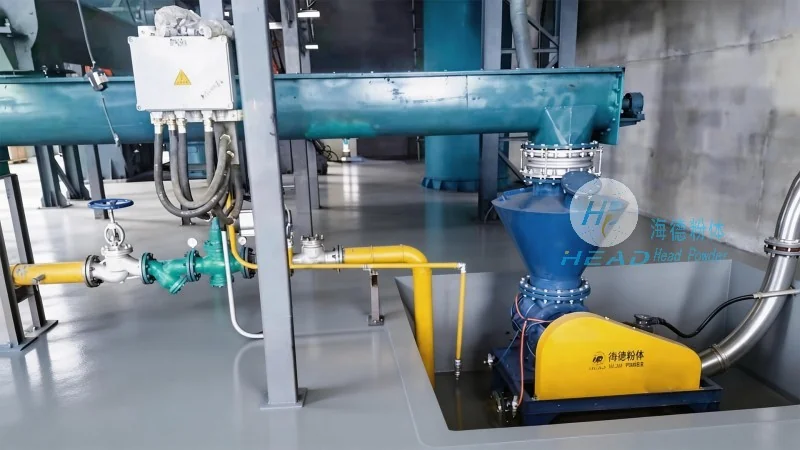
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is a prominent manufacturer specializing in activated carbon material handling solutions. The company has established itself as a leader in the industry by leveraging extensive technical expertise and a commitment to innovation. HeadPowder's team of engineers and technicians work closely with clients to understand their specific operational needs and design customized systems that meet their requirements. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and rigorous quality control processes, ensuring that each system is built to the highest standards of performance and durability. HeadPowder's focus on customer-centric solutions has enabled the company to deliver reliable and efficient activated carbon granule material handling systems that enhance operational efficiency and contribute to the success of industrial processes. By prioritizing quality and adaptability, HeadPowder continues to serve a diverse clientele across various industries, providing them with the tools necessary to optimize their material handling operations. The company's experience in the field, combined with its dedication to research and development, ensures that their products remain at the forefront of industry standards, meeting the evolving demands of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top