With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the principles and operational characteristics of fertilizer granular material conveying is crucial for optimizing industrial processes in agricultural and chemical sectors. This article delves into the core mechanisms behind efficient material handling, focusing on the technical aspects and practical applications that define modern conveying solutions.
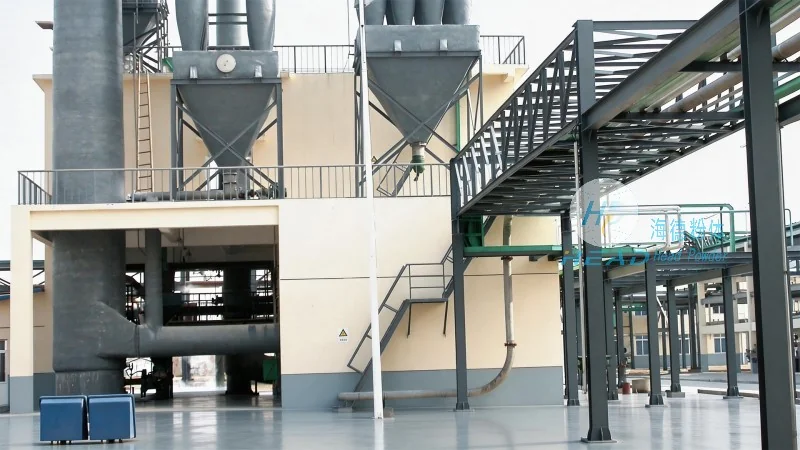
The fundamental principle of fertilizer granular material conveying involves the movement of solid particles through a system of pipes, belts, or other transport mechanisms. Key factors such as particle size, density, and moisture content significantly influence the choice of conveying method. For instance, headpowder, a leading provider in the field, emphasizes the importance of selecting appropriate equipment based on these material properties to ensure reliable and efficient transport.
Industrial applications of fertilizer granular material conveying span various environments, from large-scale fertilizer production facilities to agricultural storage and distribution centers. The working scene characteristics vary based on the scale of operation, the type of fertilizer (e.g., nitrogen, phosphorus, potassium), and the specific processing steps involved. In manufacturing plants, for example, conveying systems must handle high volumes of granular materials while maintaining product integrity and minimizing dust generation. At storage facilities, the focus shifts to efficient bulk handling and distribution to meet market demands.
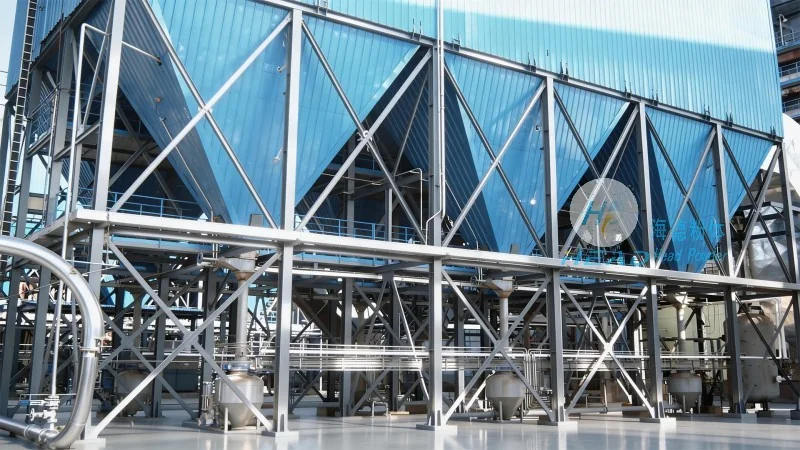
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in designing and implementing advanced conveying systems tailored to the unique needs of fertilizer industries. The company’s expertise lies in integrating mechanical, pneumatic, and hydraulic technologies to create customized solutions that enhance productivity and reduce operational costs. Their systems are engineered to handle diverse granular materials, ensuring consistent performance under varying operational conditions.
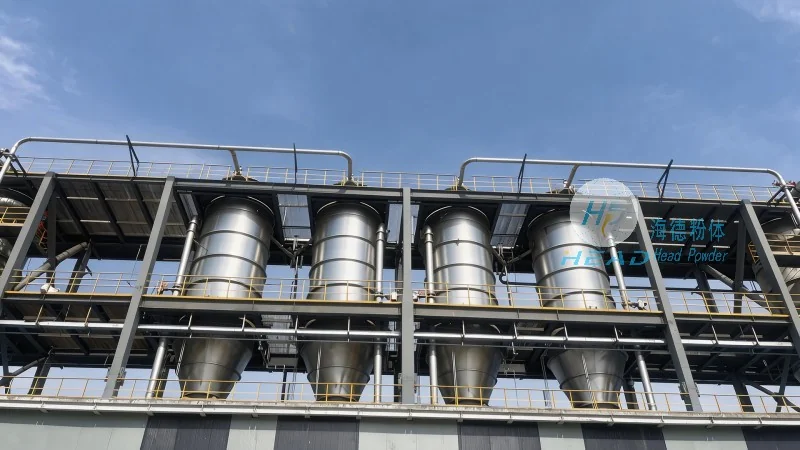
Contemporary fertilizer granular material conveying systems offer several advantages over traditional methods. These include improved energy efficiency, reduced maintenance requirements, and enhanced safety features. For instance, pneumatic conveying systems, which use air pressure to move materials, are particularly effective for handling fine granules and minimizing dust exposure. Belt conveyors, on the other hand, are ideal for transporting larger, heavier particles over longer distances. headpowder’s solutions often combine these technologies to achieve optimal performance, balancing speed, capacity, and reliability.
As the fertilizer industry continues to evolve, the importance of efficient granular material conveying cannot be overstated. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in advancing these technologies, ensuring that modern agricultural practices remain sustainable and productive. By understanding the principles and working scene characteristics of conveying systems, stakeholders can make informed decisions that enhance operational efficiency and support long-term growth in the sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top