

Principles and Working Scene Characteristics of Eco-friendly Powder Conveying Machines
As industrial processes evolve, the demand for efficient and sustainable material handling solutions has grown significantly. Among these, eco-friendly powder conveying machines have emerged as a crucial technology for transporting bulk materials while minimizing environmental impact. This article explores the fundamental principles behind these machines and highlights their key working scene characteristics, providing insights into how they contribute to modern industrial operations.
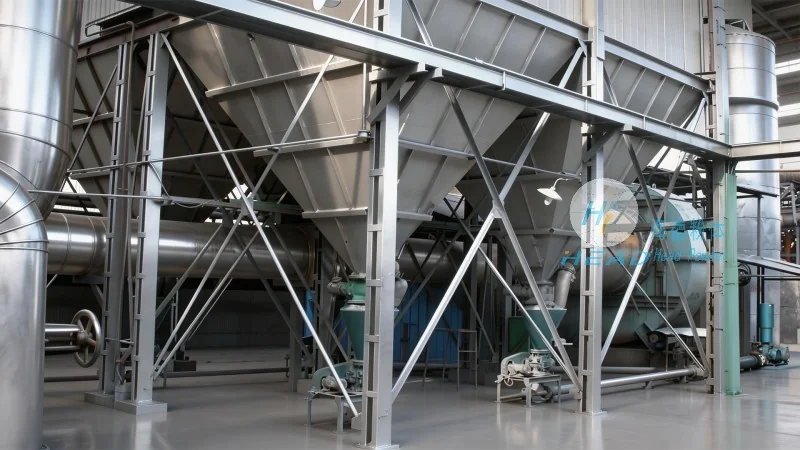
Principles of Eco-friendly Powder Conveying Machines
The core principle of eco-friendly powder conveying machines is to transport bulk powders and granules with minimal energy consumption and reduced emissions. Unlike traditional methods that may rely on high-pressure air or mechanical systems with significant energy losses, these machines often utilize advanced technologies such as vacuum or pressure differential systems. By optimizing air flow and material movement, they achieve efficient material transfer while maintaining low operational costs. The design focuses on energy efficiency, reducing the carbon footprint associated with material handling processes. This is achieved through features like variable speed drives, intelligent control systems, and energy recovery mechanisms, which help in conserving power and enhancing overall operational sustainability.
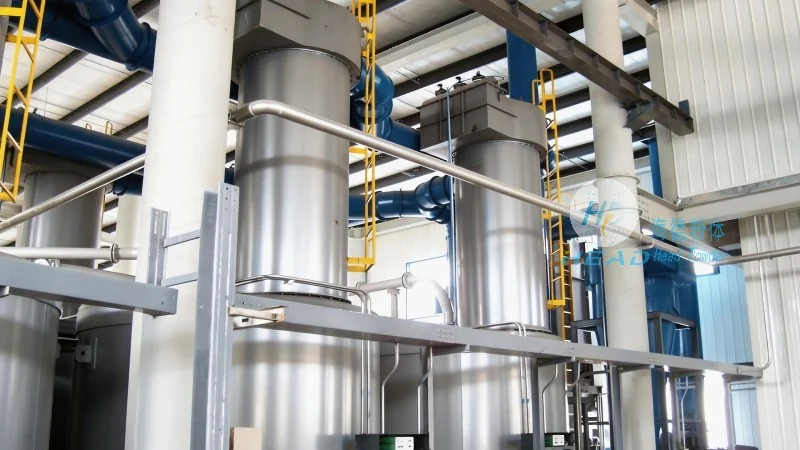
Key Working Scene Characteristics
Eco-friendly powder conveying machines are versatile and can be applied in various industrial settings. Their adaptability makes them suitable for different material types, including fine powders, bulk solids, and granules. The working scene characteristics include high efficiency in material transfer, low maintenance requirements, and compatibility with different production scales. These machines are commonly used in sectors such as pharmaceuticals, food processing, chemical manufacturing, and mining. In pharmaceutical production, for instance, the machines ensure sterile and contamination-free powder handling, which is critical for maintaining product quality and safety. In food processing, they help in transferring ingredients without compromising hygiene standards. The ability to handle diverse materials and operate in different environments makes them a preferred choice for industries that require reliable and sustainable material handling solutions.
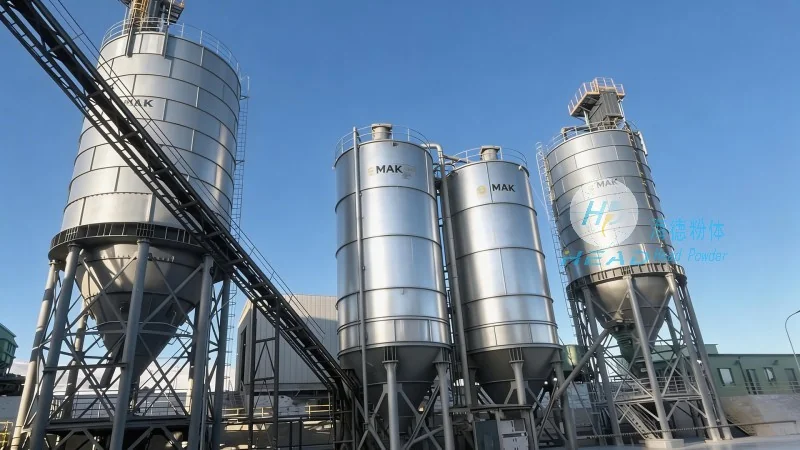
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing and supplying advanced eco-friendly powder conveying systems. With a strong commitment to sustainability and innovation, the company has established itself as a trusted partner for industries seeking efficient and environmentally responsible material handling solutions. HeadPowder's products are designed to meet the stringent requirements of modern manufacturing processes, ensuring high performance and reliability. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver cutting-edge technology to global markets. By focusing on research and development, HeadPowder continuously improves its product line to address the evolving needs of industrial applications, providing tailored solutions that enhance operational efficiency and reduce environmental impact.