With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of advanced air-pneumatic conveying systems tailored for the efficient handling of fine sand and stone materials. These systems represent a sophisticated solution for industries that require reliable, dust-free, and low-maintenance material transport solutions.
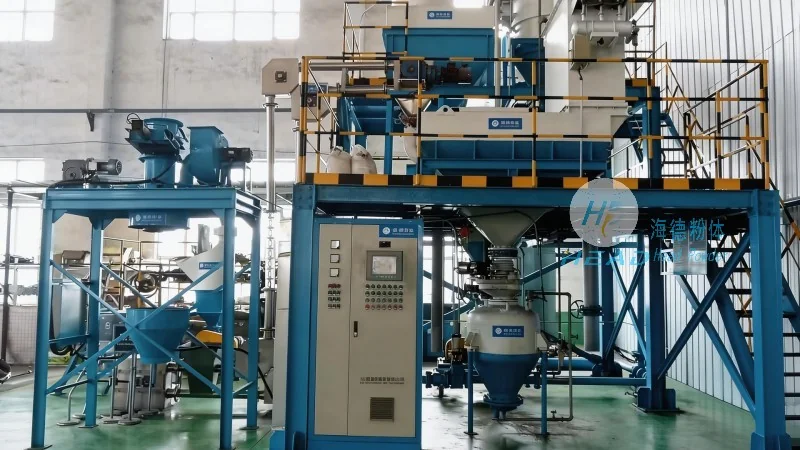
The core of the air-pneumatic conveying system lies in its ability to transport bulk materials using a combination of air pressure and vacuum. The system operates by creating a flow of air through a pipeline, which draws the fine sand and stone particles into the system. The process typically involves a series of components, including a hopper for material storage, a rotary valve for controlled discharge, a conveyor line with air ducts, and a receiver for material collection. The air flow is generated by a blower or vacuum pump, which ensures that the material is suspended and transported efficiently through the pipeline. The system can operate under positive pressure (blowing air into the system) or negative pressure (sucking air out of the system), depending on the specific application requirements. The design of the pipeline and the velocity of the air are critical factors that determine the efficiency and effectiveness of the material transport. Proper air velocity ensures that the particles are fully suspended, preventing blockages and ensuring smooth flow. The system also incorporates features such as pulse jets or rotary airlocks to maintain consistent material flow and prevent material buildup in the pipeline.
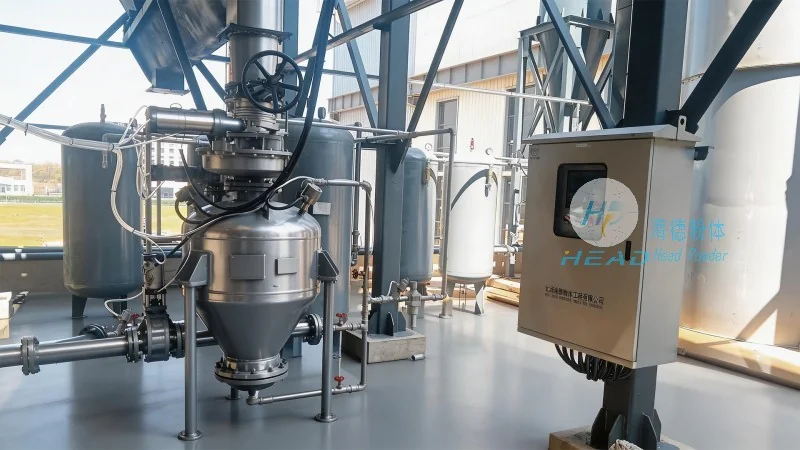
HeadPowder's air-pneumatic conveying systems for fine sand and stone materials are characterized by several distinct features that enhance performance and reliability. First, the system is designed for dust-free operation, which is essential for maintaining a clean working environment and complying with environmental regulations. The enclosed pipeline and sealed components prevent dust emissions, making it suitable for indoor or controlled outdoor applications. Second, the system offers high efficiency in material transport, with the ability to handle large volumes of fine sand and stone with minimal energy consumption. The use of positive or negative pressure allows for flexible operation, adapting to different site conditions and material characteristics. Third, the system is equipped with advanced control systems that enable precise regulation of material flow rates, pressure levels, and air velocity. This allows operators to adjust the system parameters in real-time, optimizing performance based on specific production needs. Fourth, the components are constructed from durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of fine sand and stone particles. This ensures long-term reliability and reduces maintenance costs over the system's lifespan. Additionally, the system is designed for easy integration with existing production lines, with modular components that can be customized to fit specific plant layouts and operational requirements.
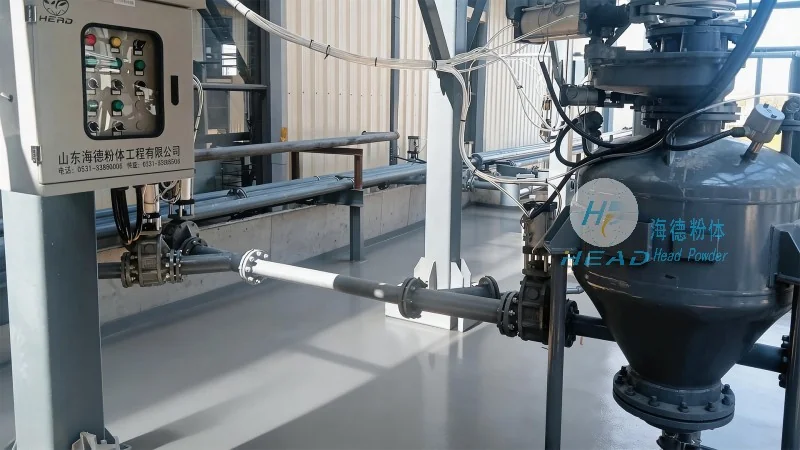
The air-pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers numerous advantages for industries dealing with fine sand and stone materials. One of the primary benefits is the elimination of manual handling, which reduces labor costs and improves workplace safety. The system also minimizes material loss and contamination, as the enclosed pipeline prevents spillage and exposure to external elements. This is particularly important for materials that are sensitive to moisture or air exposure. The system's ability to operate in both positive and negative pressure modes provides flexibility for various applications, such as transporting materials from multiple sources to a central processing unit or moving materials between different stages of production. The system is widely used in construction, mining, and manufacturing industries, where fine sand and stone are essential raw materials. For example, in the construction industry, the system can transport sand and gravel from storage silos to mixing plants, ensuring a consistent supply of materials for concrete production. In the mining industry, the system can transport crushed stone from processing facilities to storage areas, improving operational efficiency and reducing transportation costs. The system's low maintenance requirements and long service life also contribute to its cost-effectiveness, making it a preferred choice for businesses looking to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top