

Working Principle and Features of Stone Aggregate Material Handling Equipment
For industries dealing with stone aggregates, efficient material handling is crucial for maintaining operational efficiency and productivity. The stone aggregate material handling system, as provided by Shandong HeadPowder Engineering Co., Ltd., is designed to streamline the transportation and processing of these materials. This system is engineered to meet the demands of various applications, from construction sites to industrial processing facilities.
Working Principle of the Stone Aggregate Material Handling System
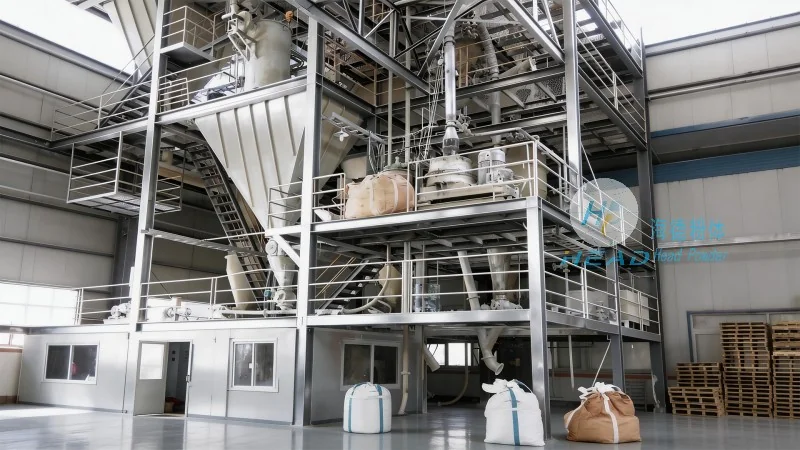
The core of the stone aggregate material handling system lies in its integrated components that work in tandem to ensure smooth material flow. The system typically begins with the intake of raw stone aggregates, which are then fed into a primary conveyor or hopper. From there, the material is transported through a series of mechanisms, including belt conveyors, screw conveyors, or bucket elevators, depending on the specific design. The system’s control panel allows for precise regulation of speed and direction, ensuring that the material is moved efficiently from the intake point to the processing or storage area. The design incorporates features such as adjustable speed controls and material flow sensors to optimize performance and prevent blockages.
Key Features of the Stone Aggregate Material Handling System
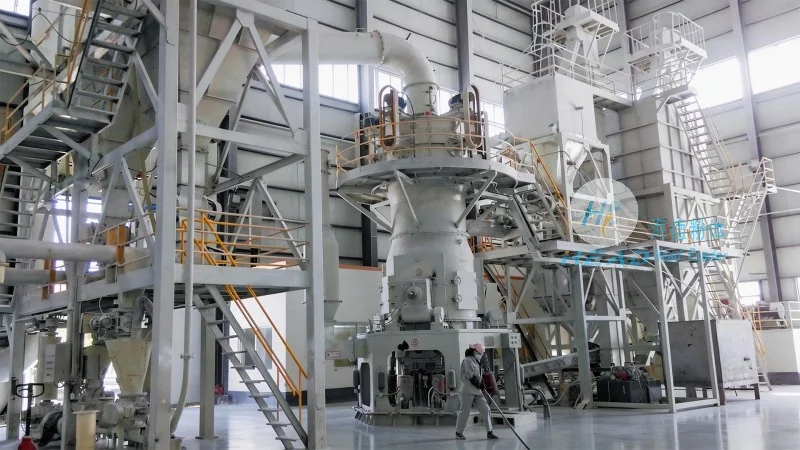
Shandong HeadPowder Engineering Co., Ltd. offers several key features that enhance the functionality and reliability of the stone aggregate material handling system. One of the primary features is the robust construction, built to withstand the heavy loads and abrasive nature of stone aggregates. The system utilizes high-quality materials, such as stainless steel and reinforced polymers, to ensure durability and longevity. Another notable feature is the modular design, which allows for easy customization and expansion to accommodate changing operational needs. The system also includes advanced safety features, including overload protection and emergency stop mechanisms, to safeguard both the equipment and personnel. Additionally, the integration of energy-efficient components helps reduce operational costs while maintaining high performance.
Applications and Benefits
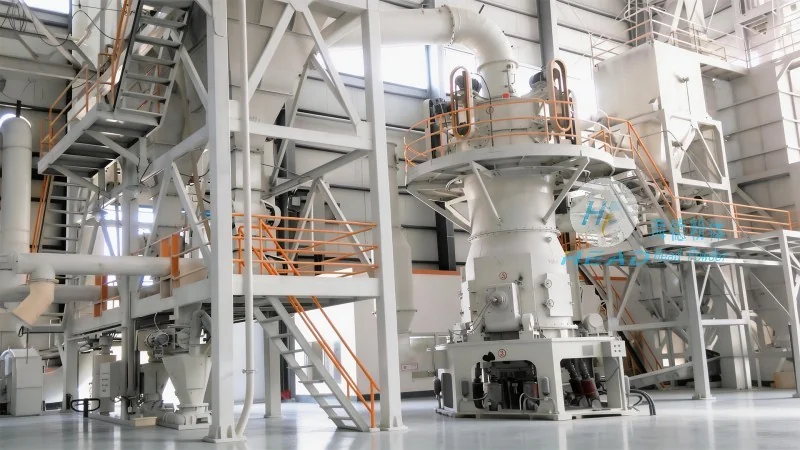
The stone aggregate material handling system is widely used in various industries, including construction, mining, and manufacturing. Its ability to handle large volumes of material efficiently makes it ideal for projects that require continuous material supply. The system’s reliability and low maintenance requirements contribute to reduced downtime and increased productivity. Furthermore, the system’s adaptability allows it to be integrated into existing production lines, minimizing the need for major infrastructure changes. The benefits of using this system extend beyond operational efficiency, as it also helps improve workplace safety by reducing manual handling of heavy materials.