

Working Principle and Features of Rare Earth Mineral Powder Material Conveying Lines
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced conveying systems tailored for the transportation of rare earth mineral powders. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for industries reliant on efficient and reliable powder handling equipment. This article delves into the working principles and key features of rare earth mineral powder material conveying lines, highlighting how these systems enhance operational efficiency and safety in industrial applications.
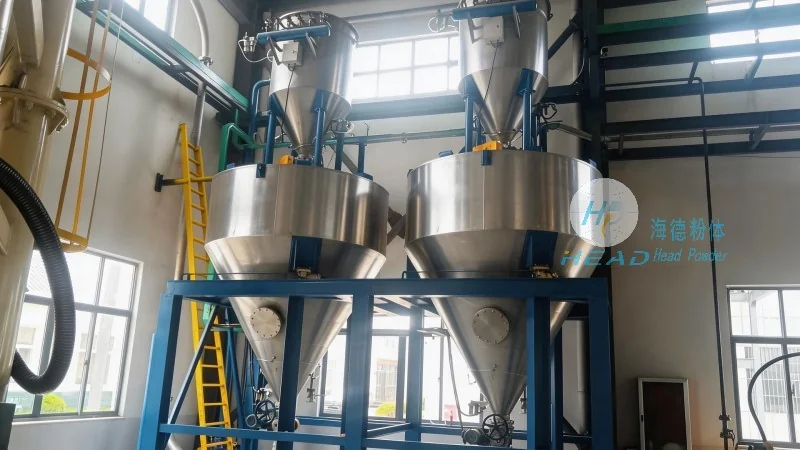
Overview of Rare Earth Mineral Powder Conveying Systems
Rare earth mineral powder conveying lines are engineered to transport fine powders, such as those derived from rare earth ores, with precision and minimal loss. These systems are typically integrated into larger industrial processes, ensuring that the material is moved from one processing stage to another without degradation or contamination. The design of these lines often incorporates specialized components to address the unique challenges posed by rare earth powders, including their fine particle size, hygroscopic nature, and potential for dust generation.
The Working Principle of Rare Earth Mineral Powder Conveying Lines
The core of a rare earth mineral powder conveying line involves a combination of mechanical and control systems that work in tandem to ensure smooth material flow. At the heart of the system is the feeding mechanism, which may include hoppers or feeders designed to regulate the flow of powder into the conveyor. This is followed by the conveyor itself, which can take various forms depending on the application—such as belt conveyors, screw conveyors, or pneumatic conveying systems. The choice of conveyor type is critical, as it must accommodate the specific properties of the rare earth powder, such as its density, flowability, and potential for caking.
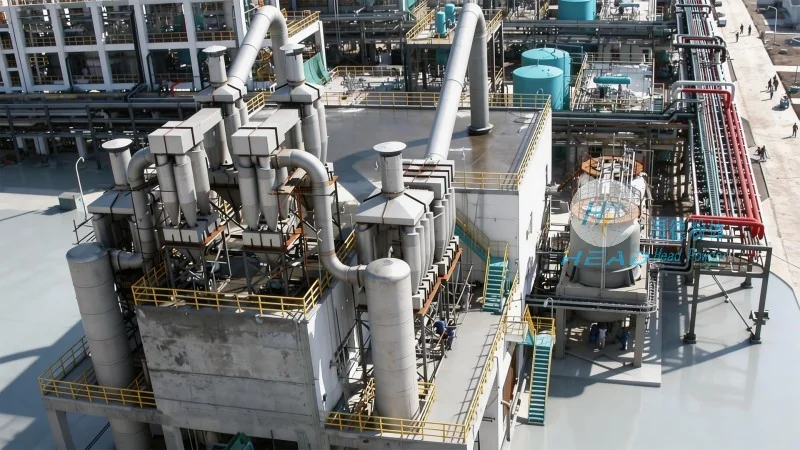
Control systems play a vital role in maintaining the efficiency of the conveying line. Sensors and monitoring devices are integrated to detect changes in flow rate, pressure, or temperature, allowing for real-time adjustments to the operation. For example, if the conveyor experiences a blockage or a drop in flow, the control system can automatically trigger alarms or adjust the feeding rate to prevent system downtime. Additionally, advanced control algorithms may be employed to optimize energy consumption and reduce operational costs, making the system both efficient and cost-effective.
Key Features of Rare Earth Mineral Powder Conveying Lines
Efficiency and reliability are paramount in rare earth mineral powder conveying lines, and several key features contribute to their performance. One of the most notable features is the ability to handle fine powders with minimal segregation or degradation. The design of the conveyor components, such as the belt or screw, is optimized to prevent particle separation, which is crucial for maintaining the quality of the rare earth material. Additionally, the systems are often equipped with dust suppression and containment measures to ensure compliance with environmental regulations and to protect personnel from exposure to fine powders.
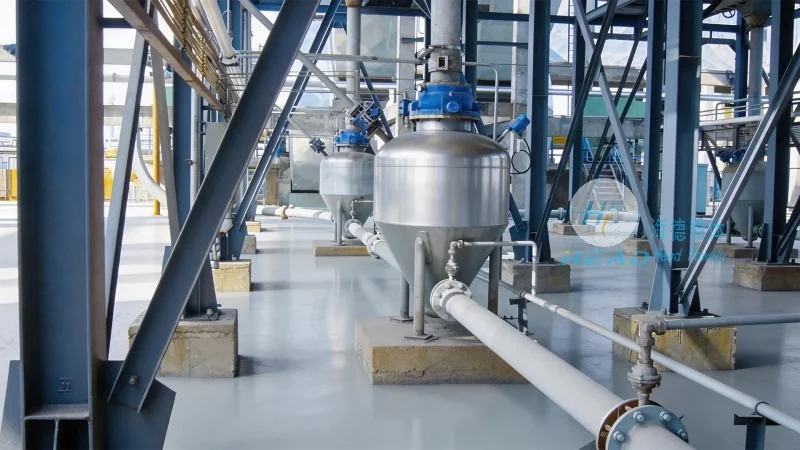
Another critical feature is the adaptability of the conveying line to different processing requirements. Many systems are modular, allowing for easy customization and expansion as production needs evolve. This flexibility enables companies to scale their operations without the need for extensive system overhauls. Furthermore, the use of corrosion-resistant materials in the construction of the conveyor components ensures durability and longevity, even when handling materials that may be chemically aggressive.
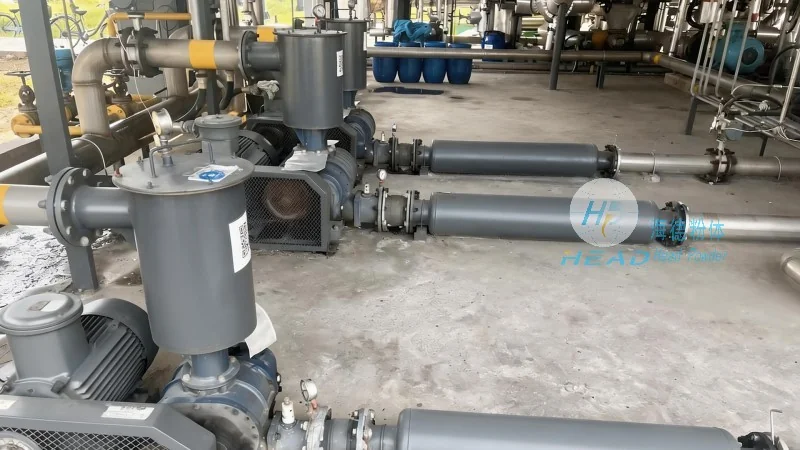
Safety is also a top priority in the design of these systems. Advanced safety features, such as emergency stop buttons, interlocks, and protective enclosures, are integrated to prevent accidents and ensure the well-being of operators. The control systems are also designed to detect and respond to potential hazards, such as overloads or overheating, thereby minimizing the risk of equipment failure or personal injury.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for rare earth mineral powder material conveying lines, combining advanced technology with robust engineering to meet the demands of modern industrial applications. By understanding the working principles and key features of these systems, industries can enhance their operational efficiency, reduce costs, and ensure the safe handling of rare earth materials. With a strong commitment to quality and customer satisfaction, HeadPowder continues to be a leader in the material handling sector, delivering reliable and efficient conveying solutions for a wide range of applications.