With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design and manufacturing of advanced conveying systems for industrial applications. The company's focus on precision and efficiency is evident in its purified powder conveying equipment, which is engineered to handle a wide range of powders with minimal contamination and optimal performance. This article explores the working principle and key features of these conveyors, providing insights into how they enhance operational efficiency in various industrial sectors.
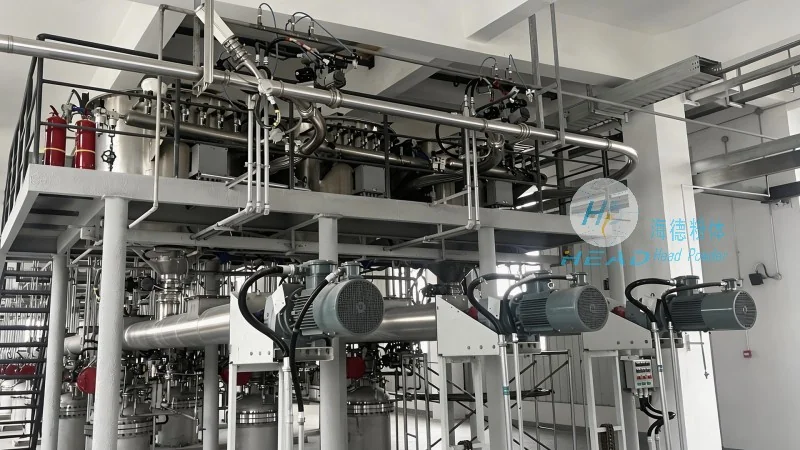
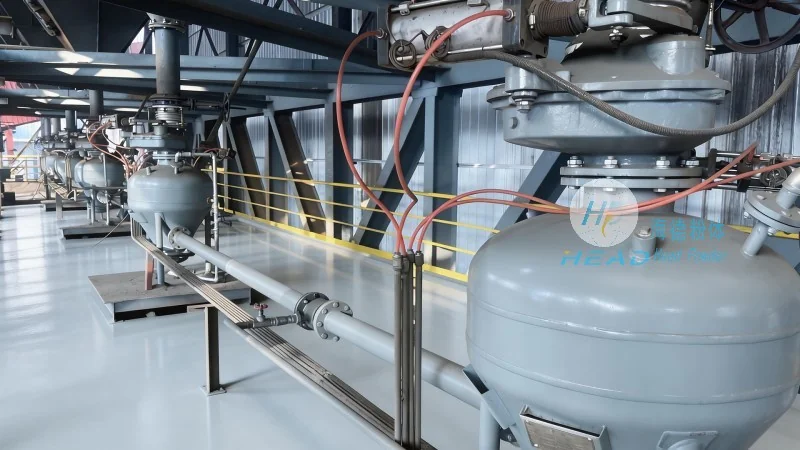
The working principle of purified powder conveyors by Shandong HeadPowder Engineering Co., Ltd. is centered on a closed, contamination-free system that ensures the integrity of the conveyed material. The system typically operates through one of two primary mechanisms: positive pressure or negative pressure. In positive pressure systems, a motor-driven blower or pump forces air (or a carrier gas) through the pipeline, carrying the powder particles along with it. This method is effective for conveying powders over longer distances and at higher capacities. Conversely, negative pressure systems use a vacuum pump to create a suction effect, drawing the powder into the pipeline. This approach is often preferred for applications requiring minimal air emissions and for handling fine powders that are prone to clogging. The conveyor components, including the pipeline, valves, and fittings, are constructed from materials such as stainless steel, PTFE, or food-grade plastics, which are resistant to corrosion and easy to clean. The sealed design of the system prevents any external contaminants from entering the material stream, ensuring that the powder remains pure throughout the conveying process. Additionally, the system is equipped with filters and traps to capture any residual particles, further enhancing the purity of the conveyed material. This combination of mechanisms and materials ensures that the conveyor operates efficiently while maintaining the highest standards of product quality.
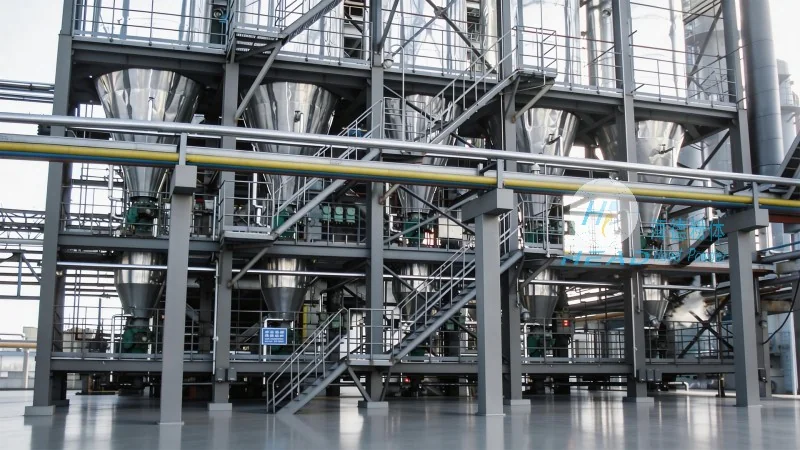
HeadPowder's purified powder conveyors are distinguished by several key features that enhance their performance and usability. One of the most notable features is the integration of advanced control technology, which allows for precise regulation of flow rates, pressure, and temperature. This level of control is crucial for maintaining consistent product quality and optimizing the conveying process. The equipment is also designed with modular components, enabling easy installation, maintenance, and customization to meet specific operational requirements. For example, the conveyor can be configured with different types of feeders, such as rotary valves or star feeders, to handle various powder characteristics and flow rates. Another important feature is the inclusion of safety mechanisms, such as pressure relief valves and emergency stop buttons, which protect both the equipment and the operators from potential hazards. The conveyors are also equipped with monitoring systems that provide real-time data on system performance, including flow rate, pressure, and temperature, allowing for proactive maintenance and troubleshooting. These features collectively contribute to the reliability, efficiency, and safety of the equipment, making it a trusted solution for industries that demand high standards of performance and product integrity.
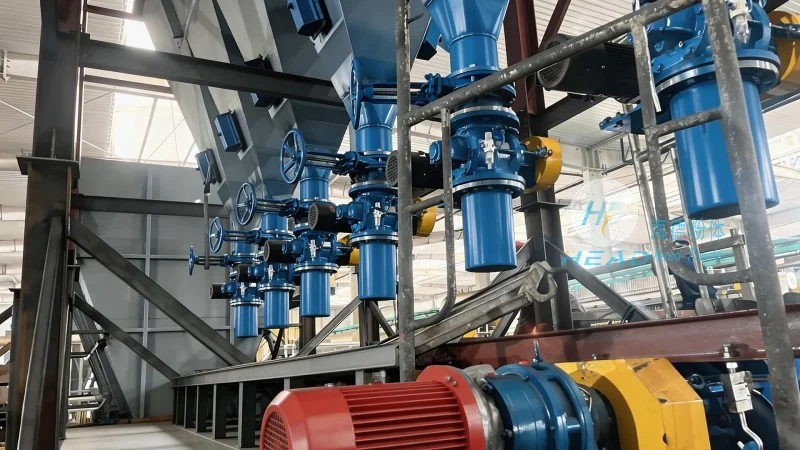
The adoption of purified powder conveyors by Shandong HeadPowder Engineering Co., Ltd. brings significant benefits to industrial operations, particularly in sectors where product purity and operational efficiency are critical. By maintaining a closed system, the conveyors minimize product contamination, which is essential in industries such as pharmaceuticals, where even trace amounts of contaminants can affect product efficacy and safety. The sealed design also reduces dust emissions, contributing to a cleaner and safer working environment and helping companies comply with environmental regulations. Furthermore, the efficient operation of the conveyors leads to lower energy consumption and reduced operational costs over time, providing a long-term return on investment. The versatility of the equipment allows it to be used in a wide range of applications, from small-scale processing plants to large-scale industrial facilities. For instance, in the pharmaceutical industry, the conveyors are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product meets stringent quality standards. In the food processing industry, they are employed to handle powders like flour, sugar, and spices, maintaining the purity and freshness of the ingredients. In electronics manufacturing, the conveyors are used to transport fine powders used in circuit board production, where contamination can impact the performance of electronic components. The ability to handle a variety of powder types and sizes, combined with the ability to operate in different environments, makes the purified powder conveyors a versatile and essential tool for modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top