With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of advanced powder handling technologies, specializes in the design and implementation of capsule powder conveying systems. These systems are engineered to efficiently transport bulk powders, ensuring precision, reliability, and safety in industrial applications. This article explores the fundamental working principles and distinctive characteristics of capsule powder conveying, highlighting how these systems address the unique challenges of powder handling.
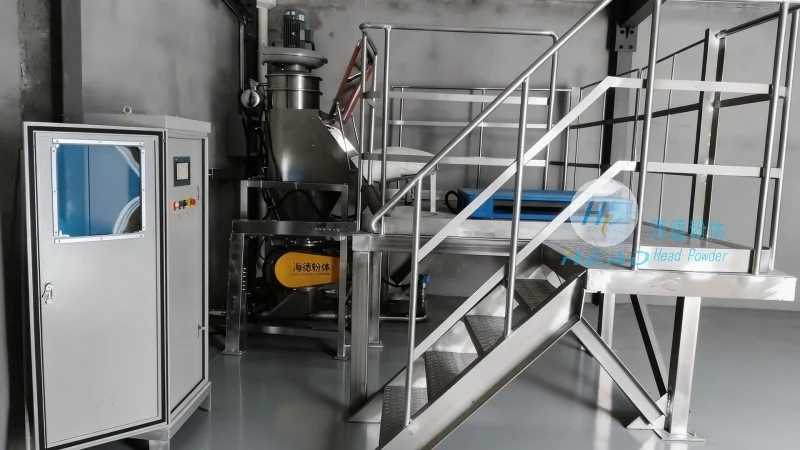
HeadPowder, operating from Shandong, China, is dedicated to delivering innovative powder handling solutions tailored to the needs of various industries. With a focus on quality and performance, the company has established itself as a trusted partner for businesses seeking reliable and efficient powder conveying systems. The expertise of HeadPowder lies in understanding the complexities of powder flow and developing systems that optimize material transport while minimizing downtime and operational costs.
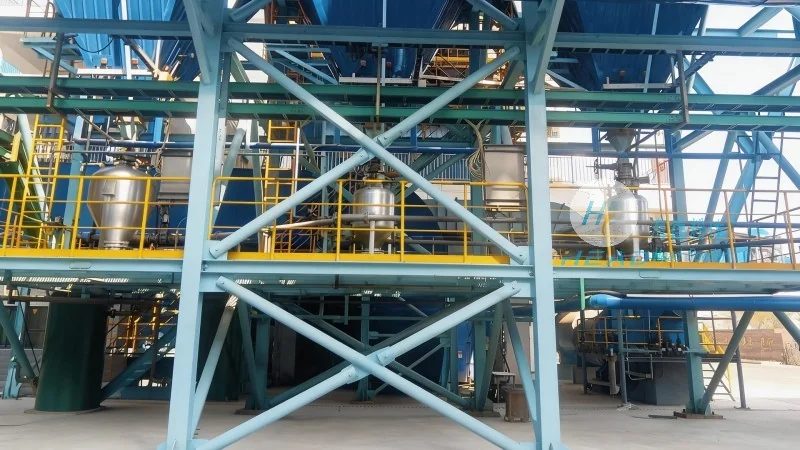
The core working principle of capsule powder conveying involves the use of flexible, collapsible tubes or hoses that can be expanded and contracted to move powders. These capsules, often made from durable materials like food-grade or industrial-grade plastics, are designed to accommodate the bulk density and flow characteristics of different powders. The system operates by creating a vacuum or pressure differential within the capsule, which draws the powder from the source and transports it to the destination. This process is typically automated, with control systems monitoring flow rates, pressure, and other critical parameters to ensure consistent and controlled delivery. The capsules are flexible, allowing them to navigate complex layouts and obstacles, making them ideal for applications where rigid pipelines are impractical. The principle of operation is based on the principles of fluid dynamics and pneumatic transport, where the powder is suspended in a carrier gas or air stream, enabling smooth and continuous movement. The system can handle a wide range of powder types, from fine powders to bulkier materials, with minimal degradation or segregation. By controlling the pressure and flow rate, operators can adjust the conveying speed and volume to meet specific production requirements. The automated control systems ensure that the process is consistent, reducing the risk of human error and improving overall efficiency.
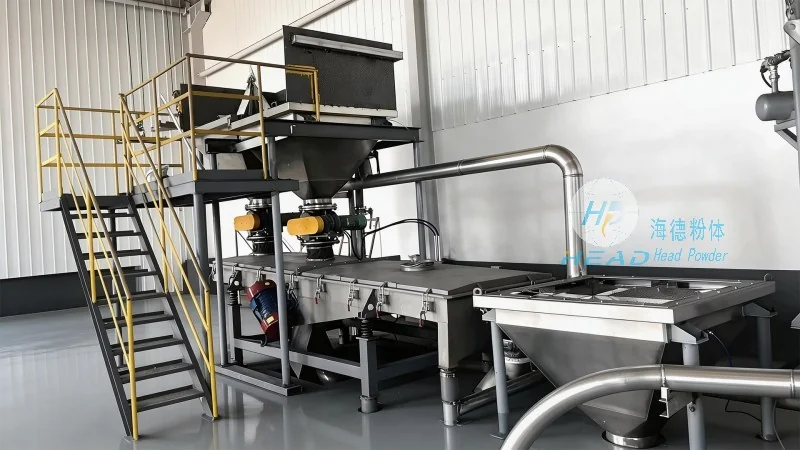
Capsule powder conveying systems exhibit several key characteristics that make them superior to traditional rigid pipelines in many applications. First, their flexibility allows for easy installation and adaptation to existing facilities, reducing the need for extensive civil works and reconfiguration. This flexibility also enables the system to handle irregular or changing layouts, such as in plants with limited space or complex production lines. Second, the systems are highly versatile, capable of conveying a wide variety of powders, including sensitive materials that may degrade in rigid pipelines. The flexible capsules protect the powder from friction and contamination, maintaining its quality and integrity throughout the conveying process. Third, the systems offer excellent control over flow rates and pressure, allowing for precise delivery of powders to different destinations. This precision is crucial in applications where exact dosing or batching is required, such as in pharmaceutical manufacturing or food processing. Fourth, the maintenance of capsule systems is relatively simple and cost-effective compared to rigid pipelines. The flexible components can be replaced or repaired without major disruptions, reducing downtime and maintenance costs. Additionally, the systems are less prone to blockages and clogs, as the flexible material allows for self-cleaning and the prevention of material buildup. Finally, the systems are designed with safety in mind, incorporating features such as pressure relief valves and leak detection to minimize risks associated with powder handling. The combination of these characteristics makes capsule powder conveying an attractive solution for industries seeking efficient, reliable, and adaptable powder transport solutions.
The advantages of capsule powder conveying are evident in various industrial applications. In the pharmaceutical industry, for example, capsule systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring consistent dosing and quality control. The flexibility of the system allows for easy integration into existing production lines, minimizing the need for modifications. In the food and beverage industry, capsule conveying is employed to transport powders like cocoa, milk powder, and vitamins, maintaining the product's freshness and quality. The systems are also used in chemical and mineral processing, where they handle bulk materials like cement, limestone, and coal. The benefits of these systems include improved product quality, reduced operational costs, and enhanced safety. By minimizing material degradation and segregation, capsule systems help maintain the integrity of the product, which is critical in industries where quality is paramount. Additionally, the systems reduce the risk of dust explosions and other safety hazards by containing the powder within the flexible tubes. The automated control systems further enhance safety by monitoring and controlling the process parameters in real-time. Overall, capsule powder conveying systems offer a reliable and efficient solution for bulk powder transport, addressing the unique challenges of each industry while providing consistent performance and durability.
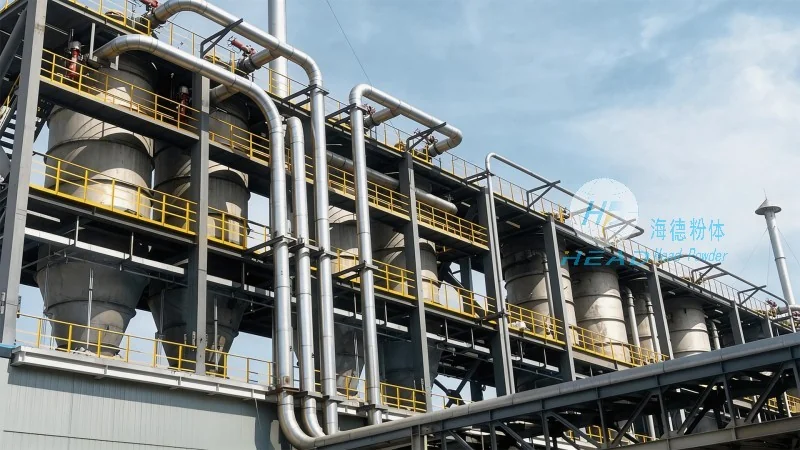
HeadPowder's expertise in capsule powder conveying systems positions the company as a leader in providing advanced powder handling solutions. By leveraging the working principles and characteristics of these systems, businesses can achieve efficient, reliable, and safe powder transport. The flexibility, versatility, and control offered by capsule systems make them an ideal choice for modern industrial applications. As industries continue to demand higher efficiency and quality in powder handling, HeadPowder remains committed to delivering innovative solutions that meet these needs. With a focus on customer satisfaction and technological advancement, HeadPowder is poised to play a significant role in the future of powder handling, helping businesses optimize their operations and achieve their production goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top