

Working Principle and Features of Negative Pressure Dilute Phase Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced negative pressure dilute phase pneumatic conveying equipment. This article aims to provide a comprehensive overview of the working principle and key features of such equipment, highlighting its applications and benefits in various industrial sectors.
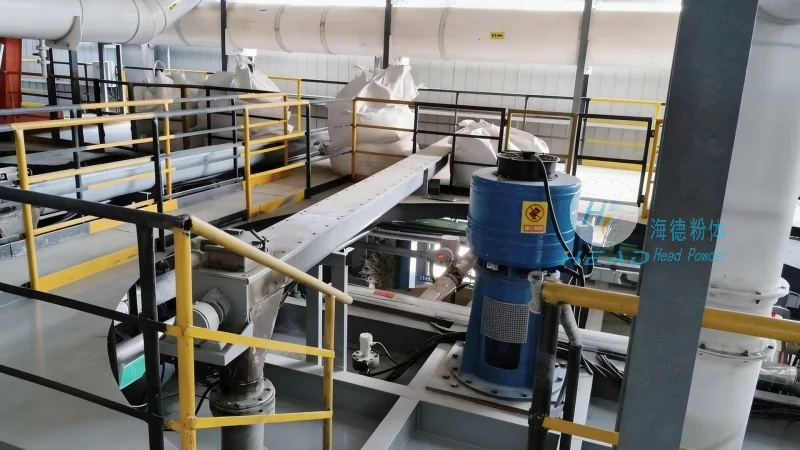
Introduction to Negative Pressure Dilute Phase Pneumatic Conveying
Negative pressure dilute phase pneumatic conveying systems are widely used in industries such as food, pharmaceuticals, chemicals, and minerals processing. These systems operate by creating a negative pressure (vacuum) in the conveying line to draw material from the source and transport it to the destination. The "dilute phase" refers to the low concentration of solid particles in the air stream, which allows for efficient and low-cost material transport over moderate distances.
Working Principle of Negative Pressure Dilute Phase Pneumatic Conveying Equipment
The core working principle of negative pressure dilute phase pneumatic conveying equipment involves several key components and processes. The system typically includes a vacuum pump, a conveying line, a material inlet, a material outlet, and a filter system. Here's a step-by-step breakdown of how the equipment operates:
1. **Material Loading**: The material to be conveyed is loaded into the material inlet, which is usually equipped with a hopper or a feeder. The feeder ensures a consistent flow of material into the conveying line.
2. **Vacuum Creation**: The vacuum pump is activated, creating a negative pressure within the conveying line. This pressure difference draws the material from the inlet and pulls it along with the air stream.
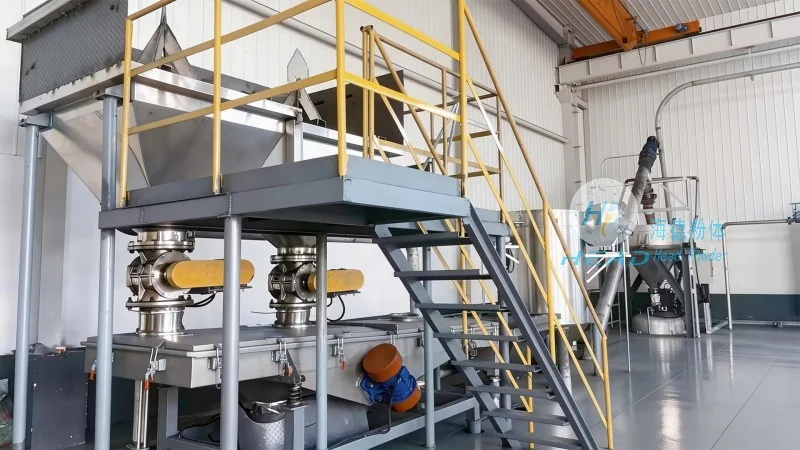
3. **Material Transport**: As the material is drawn into the line, it becomes suspended in the air stream due to the low pressure and high air velocity. The material is then transported to the destination, where it is discharged through the material outlet.
4. **Air Filtration and Recovery**: The air stream, now containing the conveyed material, passes through a filter system. The filter separates the solid particles from the air, allowing the air to be recycled back into the system or released into the environment. This step ensures that the system operates efficiently and maintains air quality.
Key Features of Negative Pressure Dilute Phase Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. offers negative pressure dilute phase pneumatic conveying equipment with several notable features that enhance performance and reliability. These features are designed to meet the specific needs of different industries and applications:
1. **Low Energy Consumption**: The dilute phase operation reduces the energy required for material transport compared to dense phase systems. The negative pressure approach minimizes the need for high-pressure air, resulting in lower operational costs.
2. **Versatile Material Handling**: The equipment can handle a wide range of materials, including powders, granules, and fine particles. It is suitable for materials with varying flow properties, such as cohesive or abrasive substances.
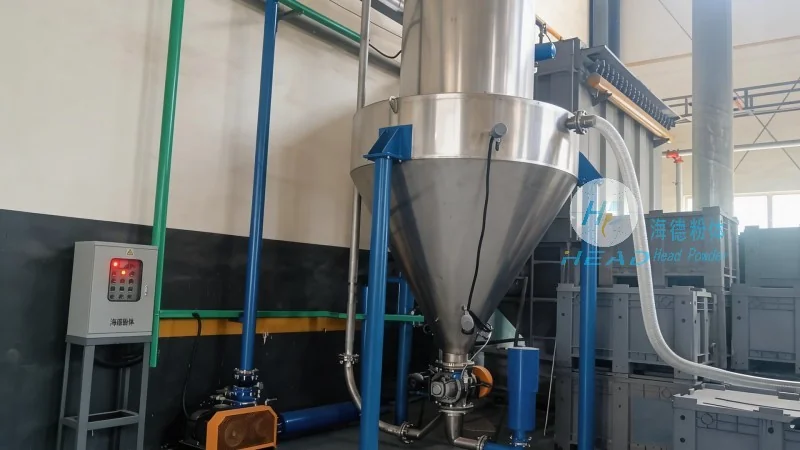
3. **Minimal Product Contamination**: The closed system design and filtration process ensure that the conveyed material remains clean and free from contamination. This is particularly important in industries like food and pharmaceuticals where product purity is critical.
4. **Quiet Operation**: Negative pressure systems operate at lower air velocities compared to positive pressure systems, resulting in quieter operation. This makes them suitable for applications where noise control is a concern.
5. **Easy Installation and Maintenance**: The equipment is designed for easy installation and maintenance. The modular components allow for quick replacement of parts, reducing downtime and maintenance costs.
Applications and Benefits
Negative pressure dilute phase pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is used in various applications across different industries. The equipment is particularly beneficial in applications where material transport needs to be efficient, cost-effective, and clean. Some common applications include:
1. **Food and Beverage Industry**: Conveying of powders, granules, and other food products in a hygienic and contamination-free manner.
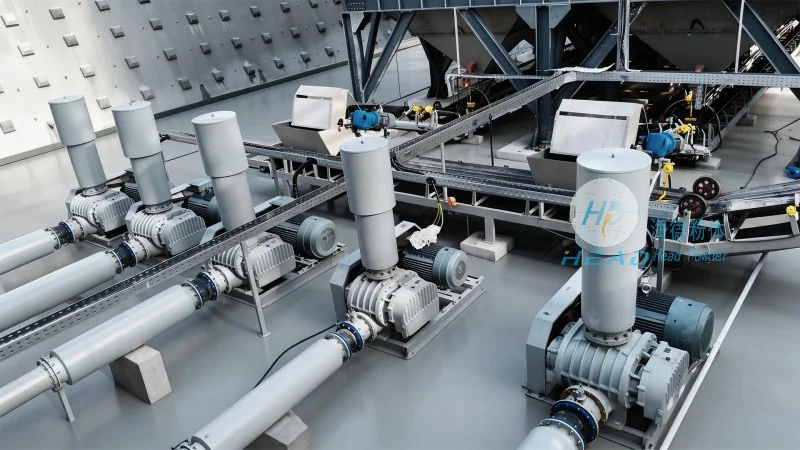
2. **Pharmaceutical Industry**: Transporting active pharmaceutical ingredients (APIs) and other sensitive materials with minimal risk of contamination.
3. **Chemical Industry**: Handling chemicals and powders in a controlled environment, ensuring safety and compliance with regulations.
4. **Minerals and Mining Industry**: Conveying minerals and ores from processing plants to storage or further processing facilities.
By leveraging the advanced technology and expertise of Shandong HeadPowder Engineering Co., Ltd., industries can achieve efficient and reliable material transport solutions that meet their specific requirements. The negative pressure dilute phase pneumatic conveying equipment offers a cost-effective and environmentally friendly approach to material handling, contributing to improved operational efficiency and product quality.