

The Working Principle and Characteristics of Cocoa Powder Pneumatic Conveying
HeadPowder, a leading provider in the field, specializes in advanced material handling solutions tailored for industries dealing with fine powders such as cocoa. This article delves into the fundamental aspects of cocoa powder pneumatic conveying, focusing on its operational mechanics and key attributes that make it a preferred choice for efficient material transport.
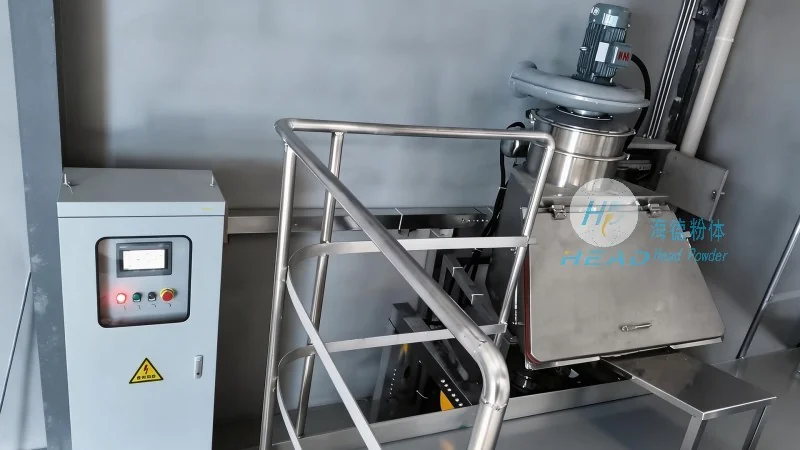
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, is dedicated to delivering innovative engineering solutions for bulk material handling. With a strong commitment to quality and efficiency, the company has established itself as a trusted partner in the industry, offering tailored pneumatic conveying systems that meet the specific needs of clients in various sectors.
Understanding Pneumatic Conveying for Cocoa Powder
Pneumatic conveying is a method that utilizes air to transport solid materials like cocoa powder through a pipeline system. This technology eliminates the need for mechanical components such as belts or buckets, offering a more hygienic and flexible approach to material handling. The process typically involves either positive pressure or negative pressure systems, each with distinct characteristics suited to different operational requirements.
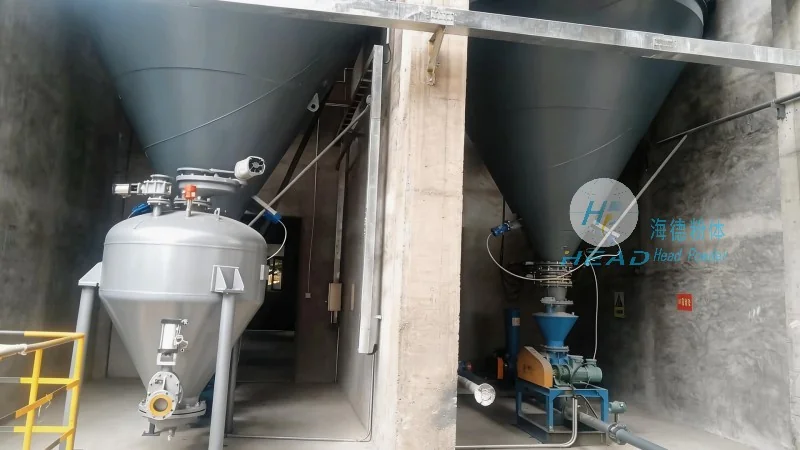
The Working Principle of Cocoa Powder Pneumatic Conveying
In the context of cocoa powder, the working principle revolves around creating a flow of air that propels the powder particles through the conveying line. Positive pressure systems generate air pressure within the pipeline, pushing the material forward, while negative pressure systems create a vacuum that draws the powder into the line. For cocoa powder, which is often sensitive to moisture and contamination, the choice of system can significantly impact the quality and integrity of the product during transport.
Key Characteristics of Cocoa Powder Pneumatic Conveying Systems
Several distinct characteristics define the effectiveness of pneumatic conveying systems for cocoa powder. Firstly, the hygienic design of these systems ensures that the product remains free from external contaminants, which is crucial for maintaining the quality of cocoa powder used in food and beverage applications. Secondly, the flexibility of the system allows for easy integration with existing production lines, enabling seamless material transfer without disrupting operational workflows. Additionally, the ability to handle fine powders with minimal degradation is a critical advantage, as cocoa powder is prone to clumping and particle breakage if not handled properly.
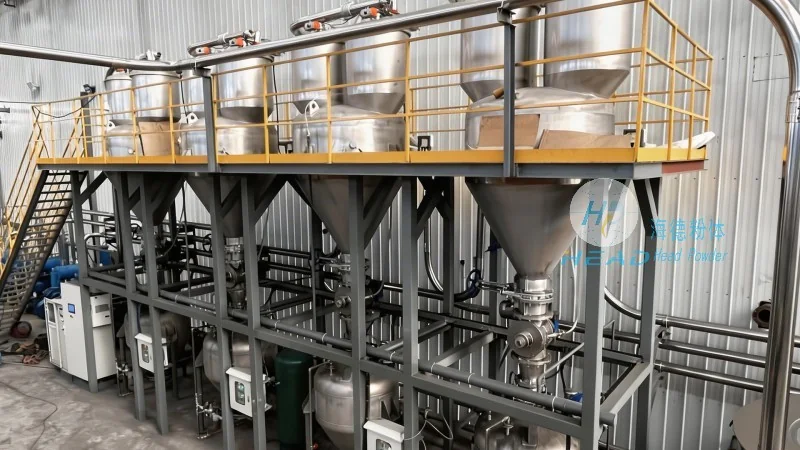
Efficiency and Performance in Material Handling
The efficiency of pneumatic conveying for cocoa powder is marked by its ability to achieve high throughput rates while maintaining consistent material flow. The system's design allows for precise control over air pressure and flow rates, ensuring that the powder is transported at optimal speeds without excessive energy consumption. This balance between performance and energy efficiency makes it an economical choice for long-term material handling operations. Furthermore, the reduced need for manual handling and the elimination of mechanical wear and tear contribute to lower maintenance costs and extended system lifespan.
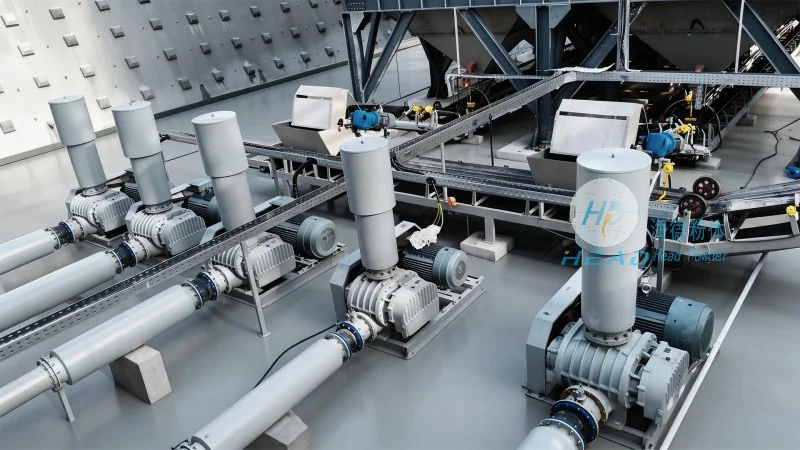
Application-Specific Advantages for Cocoa Processing
For cocoa processing facilities, the advantages of pneumatic conveying extend beyond basic material transport. The system's ability to handle fine, abrasive powders like cocoa without causing equipment damage is particularly beneficial. This reduces the risk of clogging and equipment failure, which are common issues with traditional mechanical conveyors. Additionally, the clean and enclosed nature of the system helps in maintaining compliance with food safety regulations, ensuring that the final product meets stringent quality standards. The adaptability of the system to different production scales, from small batch processing to large-scale industrial operations, further enhances its utility in diverse cocoa processing environments.
Conclusion and Industry Impact
As a result of its efficient design and operational benefits, cocoa powder pneumatic conveying has become a standard solution in the cocoa processing industry. The combination of hygienic handling, high efficiency, and flexibility makes it an indispensable component of modern material handling strategies. By leveraging advanced engineering principles, companies like Shandong HeadPowder Engineering Co., Ltd. continue to refine these systems, ensuring that they meet the evolving demands of the industry while maintaining the highest standards of product quality and operational reliability.