

What is a Barley Powder Pneumatic Conveying Machine? And What Are Its Design Principles?
Barley powder pneumatic conveying machines are specialized equipment designed to transport barley powder and other fine powders through a pipeline using air pressure. As a key component in the grain processing industry, these machines play a crucial role in ensuring efficient and safe material handling. This article, brought to you by Shandong HeadPowder Engineering Co., Ltd. (headpowder), will explore the fundamental concepts of such machines and delve into their design principles, providing a comprehensive understanding for professionals in the field.
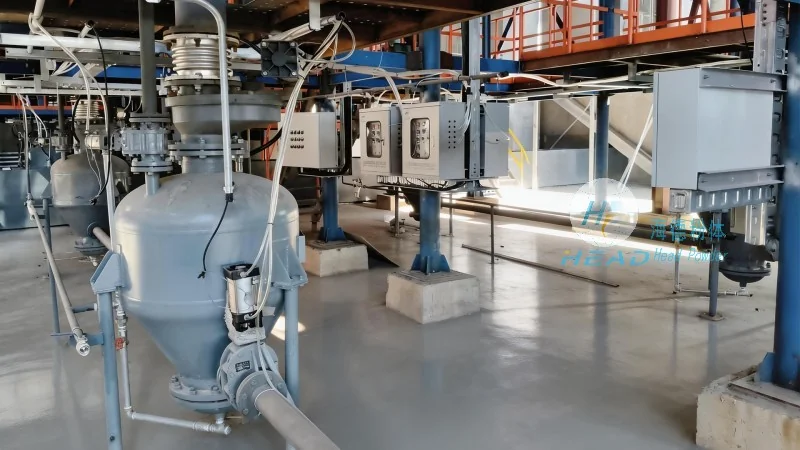
Introduction to Barley Powder Pneumatic Conveying Machines
Barley powder pneumatic conveying machines, also known as pneumatic conveyors, are systems that utilize air or gas to move powders like barley powder from one location to another. Unlike traditional mechanical conveyors, which rely on belts or buckets, pneumatic systems use the force of compressed air to propel particles through a pipeline. This method offers several advantages, including the ability to transport materials in a closed system, minimizing dust emissions and contamination. For barley processing facilities, where maintaining product purity and hygiene is paramount, these machines are an essential investment.
Key Components of a Barley Powder Pneumatic Conveying Machine
At the core of a pneumatic conveying system are several critical components that work in tandem to achieve efficient material transport. The primary components include the hopper, which holds the barley powder; the air compressor, which generates the necessary air pressure; the pipeline, through which the powder and air mixture travels; and the discharge device, which releases the material at the destination. Additionally, a filter system is often integrated to capture any fine particles that may escape the pipeline, ensuring clean air is released back into the environment. Each component must be carefully selected and maintained to ensure optimal performance and longevity of the system.
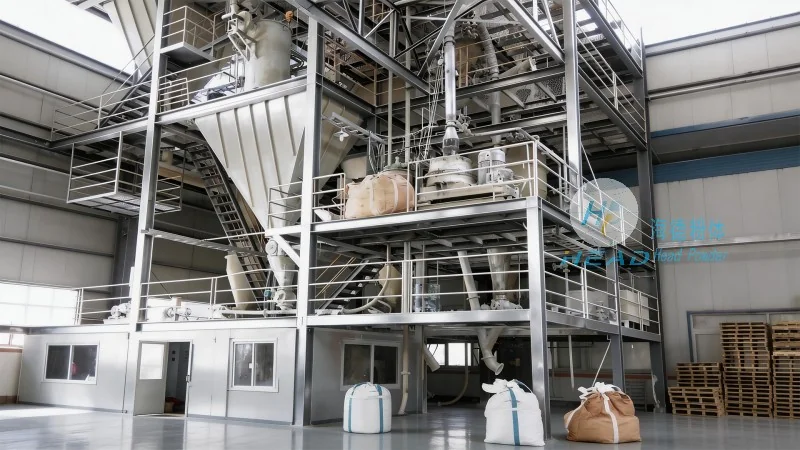
Design Principles Behind the Operation
The design principles of a barley powder pneumatic conveying machine are centered around the balance of air pressure and material flow. The system operates on the principle of creating a pressure differential between the inlet and outlet of the pipeline. By introducing compressed air into the hopper, the air and powder mixture is forced through the pipeline to the discharge point. The velocity of the air and the particle size of the barley powder are critical factors in determining the efficiency of the conveying process. Proper design ensures that the air velocity is sufficient to lift and transport the powder without causing excessive wear on the pipeline or components. Engineers must consider factors such as the specific gravity of the barley powder, the desired conveying distance, and the required flow rate when designing the system.
Advantages of Using Pneumatic Conveying for Barley Powder
Implementing a pneumatic conveying system for barley powder offers numerous benefits that enhance operational efficiency and product quality. One of the most significant advantages is the ability to maintain a closed system, which prevents dust from spreading and reduces the risk of contamination from external sources. This is particularly important in food processing environments where hygiene standards are strictly regulated. Additionally, pneumatic conveyors can handle materials with high moisture content or sticky properties, which would be difficult to transport using traditional methods. The flexibility of pneumatic systems allows for easy integration into existing processing lines, with the ability to change the direction or location of the discharge point without major modifications. This adaptability makes them a versatile choice for various barley processing applications.
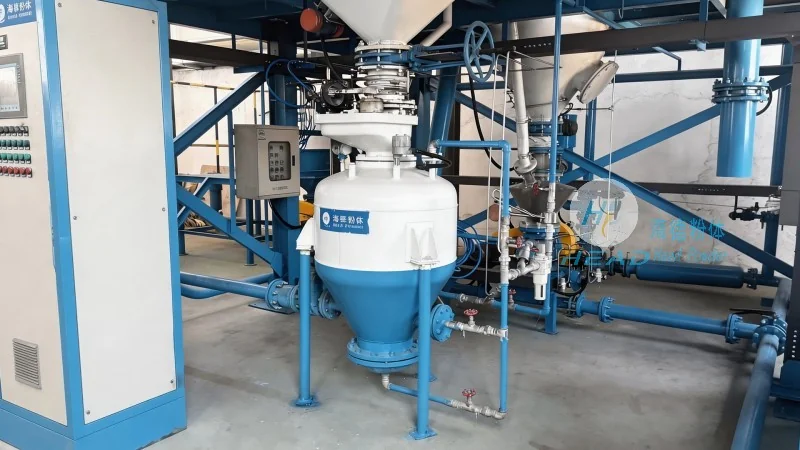
Applications in the Barley Processing Industry
Barley powder pneumatic conveying machines are widely used in various stages of barley processing, from raw material handling to final product packaging. In the milling process, these machines efficiently transport ground barley powder from storage silos to the mixing and blending areas. During the production of barley-based products like malt or flour, pneumatic conveyors ensure a consistent flow of material, reducing downtime and improving overall productivity. Furthermore, in the packaging stage, these systems can transport finished barley products to packaging lines, maintaining the integrity of the product throughout the process. The ability to handle fine powders with precision makes them indispensable in modern barley processing facilities.
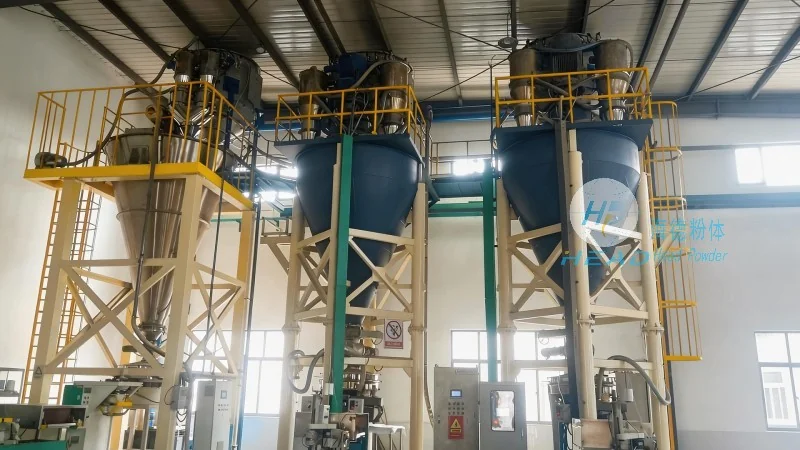
Maintenance and Operational Considerations
Proper maintenance is essential to ensure the long-term reliability and efficiency of a barley powder pneumatic conveying machine. Regular checks of the air compressor, filter system, and pipeline for blockages or wear are crucial. The hopper and discharge device should be inspected for any signs of material buildup or wear, as this can affect the system's performance. Additionally, monitoring the air pressure and flow rate during operation helps identify any issues before they lead to system failure. Training operators on the proper use and maintenance of the equipment is also vital to prevent accidents and ensure optimal performance. By adhering to a regular maintenance schedule, facilities can minimize downtime and extend the lifespan of their pneumatic conveying systems.
Conclusion
In conclusion, barley powder pneumatic conveying machines are sophisticated equipment that leverage air pressure to efficiently transport fine powders like barley powder. Their design principles, centered on maintaining a pressure differential and controlling air velocity, ensure reliable and safe material handling. The advantages of using these systems, including closed-loop operation and flexibility, make them a preferred choice in the barley processing industry. By understanding the key components and operational considerations, facilities can optimize their use of pneumatic conveying systems, enhancing productivity and maintaining product quality. As technology advances, these machines continue to evolve, offering even more efficient and sustainable solutions for barley powder transport.