With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications that require efficient and clean handling of bulk powders, the dust-free bulk bag unloading powder conveyor is a critical piece of equipment. This system is designed to safely and effectively transfer materials from bulk bags into processing or storage systems while minimizing dust generation and ensuring product integrity. Understanding the functionality and design principles of such a conveyor is essential for industries like pharmaceuticals, food processing, and chemical manufacturing where contamination control is paramount.
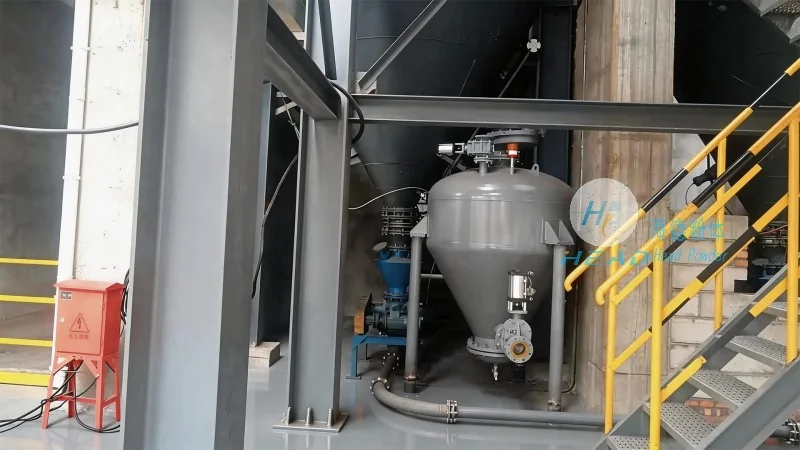
A dust-free bulk bag unloading powder conveyor, also known as a bulk bag discharger or FIBC (Flexible Intermediate Bulk Container) unloader, is a specialized system engineered to handle the unloading of powders from bulk bags. These systems are typically used in environments where dust control is a primary concern, as they incorporate features that prevent or contain dust during the material transfer process. The primary goal is to ensure that the material is transferred without exposing it to the air, thus maintaining its quality and preventing contamination from external sources.
The design of a dust-free bulk bag unloading powder conveyor involves several key components that work together to achieve efficient and clean operation. These components include the bulk bag support frame, the discharge valve or spout, the dust containment housing, and the material transfer mechanism. The support frame is designed to securely hold the bulk bag in place, ensuring stability during the unloading process. The discharge valve, often a bottom-discharge spout or a valve that can be opened and closed, allows controlled release of the material. The dust containment housing is a critical feature that encloses the entire unloading area, preventing dust from escaping into the environment. This housing may include filters or air extraction systems to further reduce dust emissions.
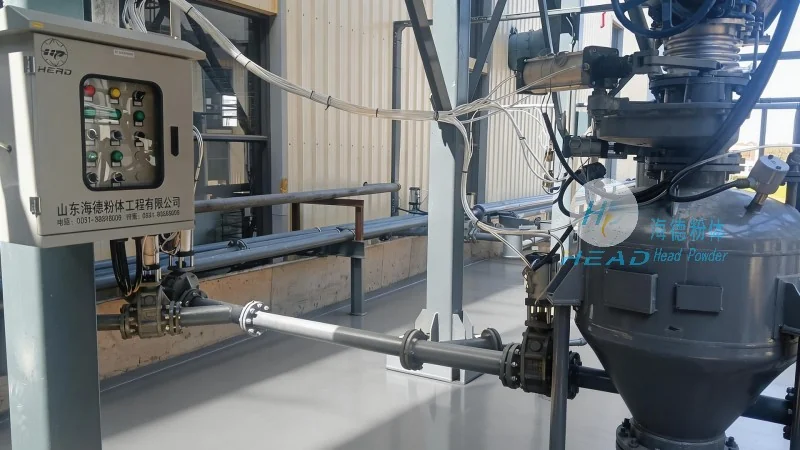
The design principles of a dust-free bulk bag unloading powder conveyor focus on creating a closed system that minimizes the interaction between the powder and the air. One of the main principles is the use of a sealed or enclosed discharge area. When the bulk bag is placed in the support frame, the discharge spout is connected to the bag, and the system is sealed. As the material is discharged, it falls into a hopper or conveyor that is integrated with the system, keeping the material contained within the equipment. This enclosed design prevents dust from being generated or released into the surrounding environment.
Another important design principle is the incorporation of air filtration or vacuum systems. Many dust-free conveyors are equipped with filters that capture any dust particles that may escape during the unloading process. These filters can be cleaned or replaced to maintain their efficiency. Some systems also use a vacuum to draw the material from the bag and into the discharge line, which further reduces the risk of dust generation. The combination of a sealed housing and filtration systems ensures that the operation is dust-free and meets the stringent requirements of industries where product purity is essential.
Dust-free bulk bag unloading powder conveyors are widely used in various industrial sectors due to their ability to handle a wide range of powders while maintaining a clean environment. In the pharmaceutical industry, for example, these systems are crucial for handling active pharmaceutical ingredients (APIs) and excipients, as any contamination can have serious health implications. In the food processing industry, they are used for handling ingredients like flour, sugar, and spices, where dust control is necessary to prevent spoilage and maintain product quality. The chemical industry also benefits from these systems when handling chemicals that are sensitive to moisture or contamination.
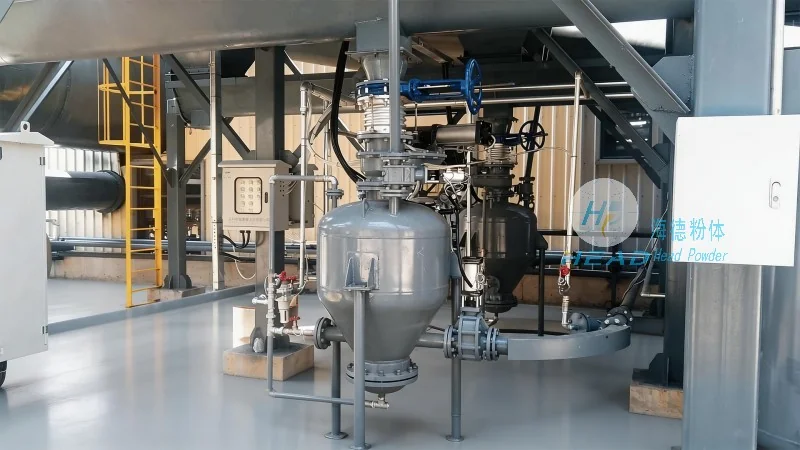
The benefits of using a dust-free bulk bag unloading powder conveyor extend beyond just dust control. These systems offer improved efficiency compared to manual unloading methods, as they can handle large quantities of material quickly and consistently. They also reduce labor costs and the risk of accidents associated with manual handling of bulk bags. Additionally, the enclosed design helps to maintain the temperature and humidity of the material, which is important for materials that are sensitive to environmental conditions.
Understanding the design principles and functionality of a dust-free bulk bag unloading powder conveyor is essential for industries that require clean and efficient handling of bulk powders. The combination of enclosed housing, filtration systems, and controlled discharge mechanisms ensures that these systems operate without generating dust, thus maintaining product integrity and meeting regulatory requirements. For companies in need of such equipment, Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, offers reliable and high-quality solutions tailored to specific industrial needs. Their expertise in engineering and manufacturing ensures that customers receive equipment that is efficient, durable, and compliant with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top