With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the Manganese Carbonate Material Handling Conveyor and Its Design Principles
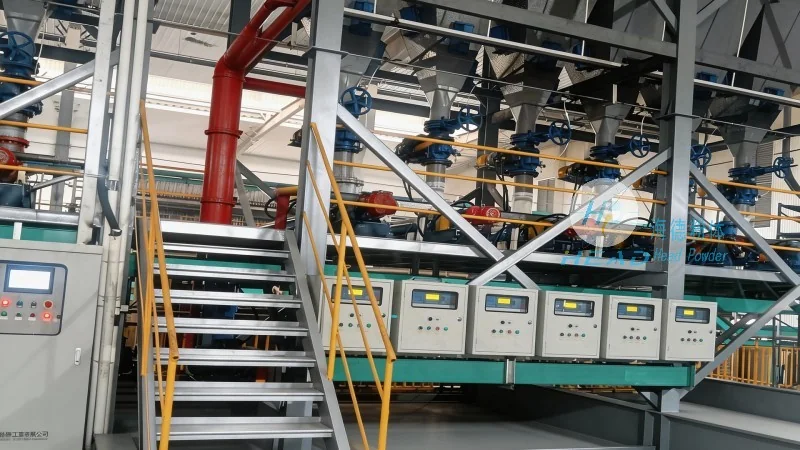
A manganese carbonate material handling conveyor is a specialized industrial system engineered to transport manganese carbonate, a critical raw material in various industries such as battery manufacturing, steel production, and chemical processing. This type of conveyor is designed to handle the unique physical and chemical properties of manganese carbonate, ensuring efficient and safe material movement from one processing stage to another. The system typically integrates components like feeders, conveyors, and control mechanisms to optimize material flow and minimize operational disruptions. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, this conveyor system exemplifies advanced engineering tailored to the demands of manganese carbonate handling.
The design of a manganese carbonate material handling conveyor involves several key components that work in tandem to achieve effective material transport. These components include: feed hoppers that receive the manganese carbonate from storage or processing units, conveyor belts or rollers that move the material along the designated path, and control systems that regulate the speed and direction of the conveyor. Additionally, the system may incorporate screening or sorting mechanisms to ensure the material meets quality standards before further processing. The choice of materials for these components, such as corrosion-resistant metals or specialized polymers, is crucial to withstand the chemical properties of manganese carbonate and maintain long-term operational efficiency.
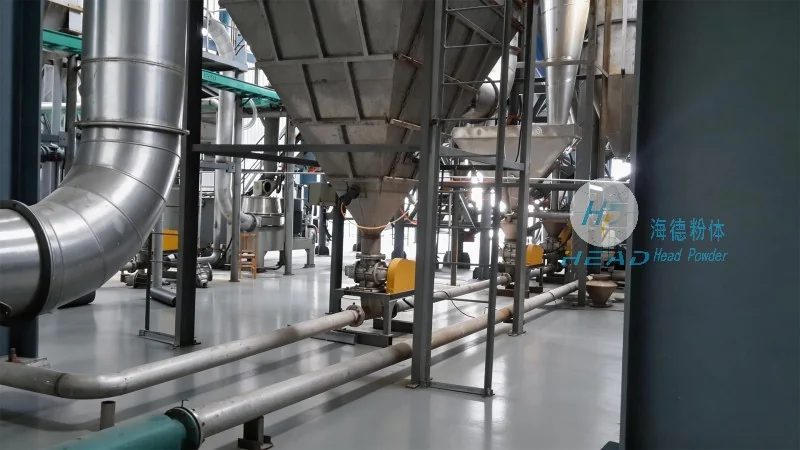
The design principles for a manganese carbonate material handling conveyor are centered on optimizing material flow, ensuring safety, and enhancing durability. One primary principle is the consideration of the material's bulk density and flow characteristics. Manganese carbonate has a relatively low bulk density compared to other minerals, which can affect how it moves through the conveyor system. Engineers must account for this by designing appropriate hopper angles and conveyor slopes to prevent material bridging or clogging. Another key principle is the prevention of material degradation during transport. Manganese carbonate is sensitive to moisture and can degrade if exposed to air or water, so the conveyor system is often enclosed or equipped with moisture-resistant materials to maintain the material's quality.
Operational efficiency is a critical aspect of manganese carbonate material handling conveyor design. The system is engineered to minimize downtime and maximize throughput. This includes features like adjustable speed controls that allow operators to match the conveyor speed to the processing capacity of downstream equipment. Additionally, the conveyor may be equipped with sensors to detect blockages or overloads, triggering automatic shutdowns to prevent equipment damage. Maintenance is another important consideration, as regular cleaning and inspection of the conveyor components are necessary to prevent the buildup of manganese carbonate residue, which can affect the system's performance over time. The design incorporates easy access points for maintenance personnel, reducing the time and effort required for routine checks and repairs.
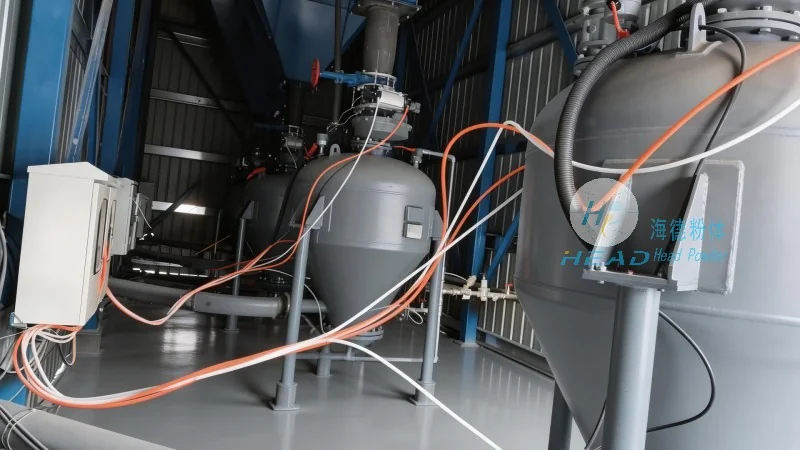
Manganese carbonate material handling conveyors play a vital role in various industrial processes where manganese carbonate is a key ingredient. In battery manufacturing, for example, the conveyor system transports manganese carbonate to mixing and compounding units, ensuring a consistent supply of raw material for battery production. In steel production, manganese carbonate is used as a deoxidizer and alloying agent, and the conveyor system efficiently delivers it to the steelmaking furnaces. The versatility of these conveyors allows them to adapt to different industrial settings, making them a valuable asset in any facility that processes manganese carbonate.
In summary, a manganese carbonate material handling conveyor is a sophisticated industrial system designed to efficiently transport manganese carbonate while adhering to specific design principles that prioritize material quality, operational safety, and long-term durability. The system's components and operational features are tailored to the unique properties of manganese carbonate, ensuring reliable performance in various industrial applications. As a result, these conveyors are essential equipment in industries that rely on manganese carbonate as a critical raw material.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top