With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Stone material handling systems are critical infrastructure in industries such as mining, construction, and manufacturing, engineered to efficiently transport and manage bulk materials like gravel, crushed stone, and other aggregates. These systems are essential for optimizing workflow, enhancing operational safety, and reducing costs associated with material movement. Understanding the core components and design principles of such systems is vital for businesses seeking to improve their material processing capabilities and overall productivity.
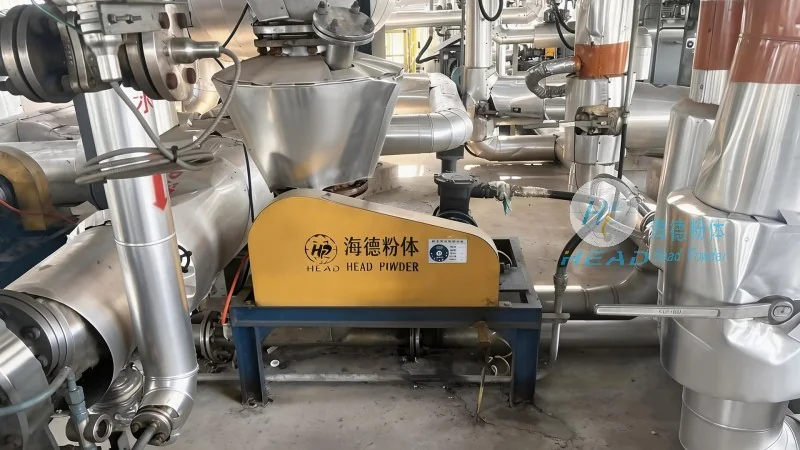
A stone material handling system typically comprises interconnected equipment including feeders, conveyors, elevators, and storage silos. The primary objective is to move raw materials from their source—such as quarries or stockpiles—to processing units, storage areas, or distribution points. Key components may include vibrating feeders for uniform material distribution, belt conveyors for horizontal transport, bucket elevators for vertical lifting, and hopper bins for temporary storage. Each component is carefully selected and integrated to ensure seamless material flow, minimizing downtime and maximizing throughput. The system's design is tailored to the specific characteristics of the material being handled, such as size, shape, moisture content, and abrasiveness, ensuring compatibility with the equipment and operational environment.
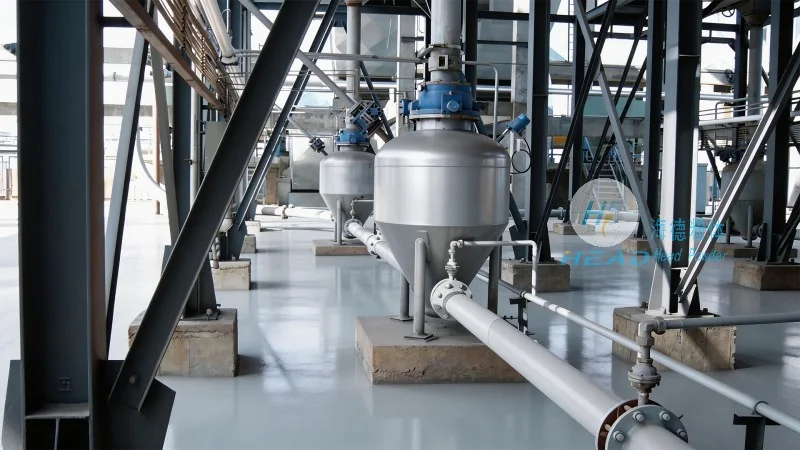
The design of a stone material handling system is guided by several fundamental principles aimed at achieving optimal performance and durability. First, the system must be adapted to the material's physical properties and processing requirements. Engineers evaluate factors like material density, flowability, and potential for degradation to select appropriate equipment that can withstand mechanical stresses and environmental conditions. Second, energy efficiency and cost-effectiveness are prioritized. Systems often incorporate variable speed drives, which adjust conveyor speed based on load, and energy-saving mechanisms to minimize power consumption. Third, safety is a non-negotiable consideration. Systems are equipped with safety guards, emergency stop mechanisms, and compliance with industry standards to protect operators and prevent accidents. Additionally, modular and scalable designs allow for easy expansion or modification as production needs evolve, ensuring long-term adaptability.
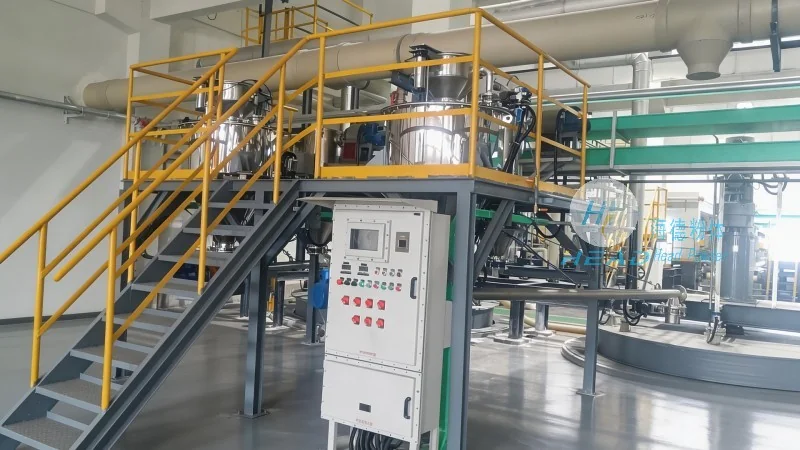
Each component within a stone material handling system serves a distinct functional role, contributing to the overall efficiency of material transport. Vibrating feeders are used to evenly distribute raw stone from a stockpile or hopper, ensuring a consistent feed rate to downstream equipment. Belt conveyors, commonly constructed from heavy-duty rubber or steel, are ideal for horizontal transport due to their ability to handle large volumes of material over long distances. Bucket elevators, with rotating buckets, are effective for vertical lifting, allowing materials to be raised to elevated levels for processing or storage. Storage silos, typically made from reinforced concrete or steel, provide bulk storage capacity, enabling smooth material flow even during periods of low demand. The integration of these components is critical; a well-designed system ensures that each part works in harmony, minimizing bottlenecks and maximizing productivity.
Stone material handling systems are widely utilized in mining operations, where they facilitate the transport of crushed ore and rock from extraction sites to processing plants, improving the efficiency of ore beneficiation. In the construction industry, they are essential for moving aggregates like gravel and sand from quarries to building sites, supporting the production of concrete and other building materials. The consistent and reliable operation of these systems directly impacts project timelines and costs, making them indispensable in modern construction and industrial processes. By optimizing material movement, these systems help reduce labor costs, minimize material waste, and enhance overall operational performance. For example, in a mining facility, an efficient stone handling system can increase ore throughput by up to 30%, while in a construction site, it can reduce material handling time by 40%.
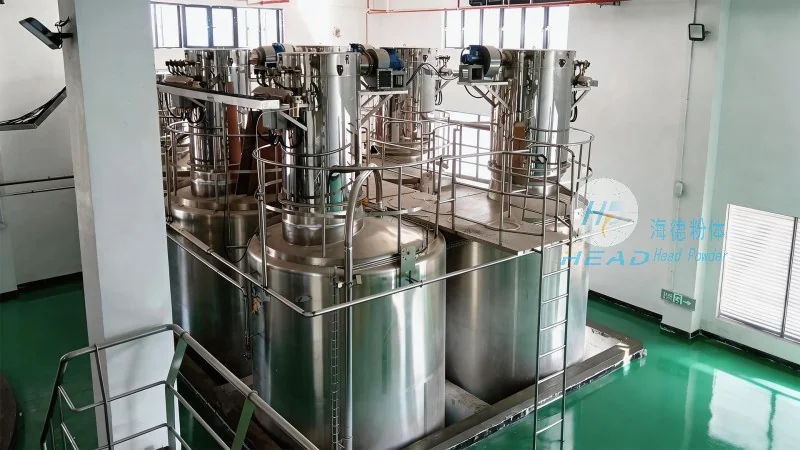
Stone material handling systems represent a sophisticated integration of engineering principles and industrial equipment, designed to meet the demanding requirements of material processing. The design principles discussed—such as material-specific considerations, energy efficiency, and safety—are fundamental to creating systems that deliver reliable performance. Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions based in Shandong, China, specializes in designing and manufacturing customized stone material handling systems tailored to the unique needs of various industries. With a focus on durability, efficiency, and safety, HeadPowder's systems help clients streamline operations and achieve their production goals. Whether for mining, construction, or other bulk material applications, these systems play a vital role in modern industrial operations. The company's expertise in system integration and material handling technology ensures that clients receive solutions that are both effective and cost-efficient, supporting long-term business success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top