With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The question of what a bentonite powder pneumatic conveying system is and the principles behind its design is crucial for those involved in material handling and processing industries. This article aims to provide a comprehensive overview of such systems, focusing on their functionality, design philosophy, and practical applications. By understanding the core elements and operational logic, users can better appreciate the efficiency and reliability these systems offer in transporting bentonite powder.
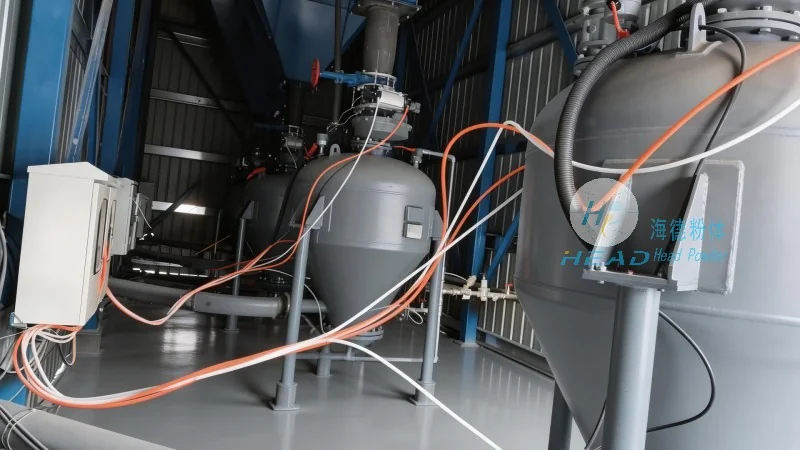
A bentonite powder pneumatic conveying system is a specialized piece of equipment designed to transport fine powders, such as bentonite, through a pipeline using air as the conveying medium. This method, known as pneumatic conveying, has become increasingly popular in industries where traditional mechanical conveying systems may be less effective or efficient. The system is engineered to handle the unique properties of bentonite, including its fine particle size, low bulk density, and potential for dust generation, ensuring safe and reliable material transport.
A typical bentonite powder pneumatic conveying system consists of several key components that work in unison to facilitate material transport. These components include a material hopper for storage, a feeder to control the flow rate, a blower or compressor to generate the necessary air pressure, a conveying pipeline, a dust collector or filtration system to manage airborne particles, and a control system for operation. Each component plays a vital role in maintaining the system's efficiency and safety, ensuring that the bentonite powder is transported without loss or degradation.
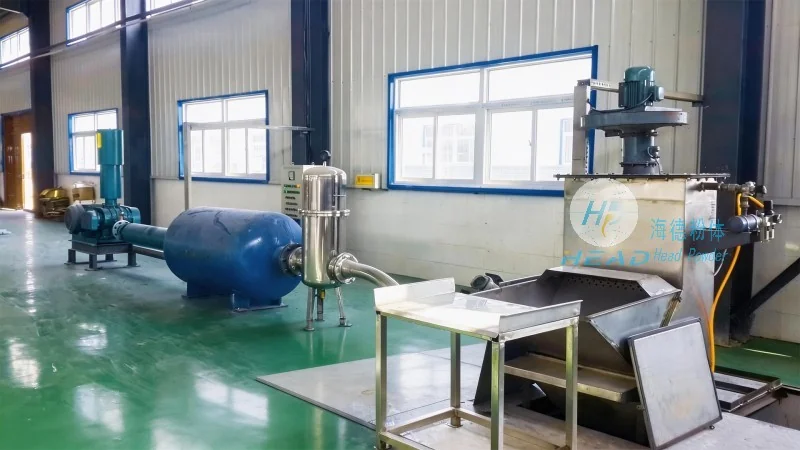
The design principle of a pneumatic conveying system for bentonite powder revolves around the use of air as the primary transport medium. This approach leverages the pressure differential created by the blower or compressor to move the powder through the pipeline. The system is designed to handle the challenges associated with fine powders, such as clogging and dust dispersion, by incorporating features like airlocks, cyclones, and adjustable flow controls. The design philosophy emphasizes energy efficiency, operational simplicity, and adaptability to varying material characteristics.
One of the primary advantages of a bentonite powder pneumatic conveying system is its ability to transport material over long distances without the need for mechanical components like belts or chains. This reduces maintenance costs and increases operational reliability. Additionally, the system can handle varying flow rates and material types, making it versatile for different industrial applications. The design also emphasizes safety, with features like explosion-proof components and dust suppression mechanisms to protect both personnel and equipment. Other benefits include reduced material waste, improved product quality due to consistent handling, and the ability to integrate with existing processing lines.
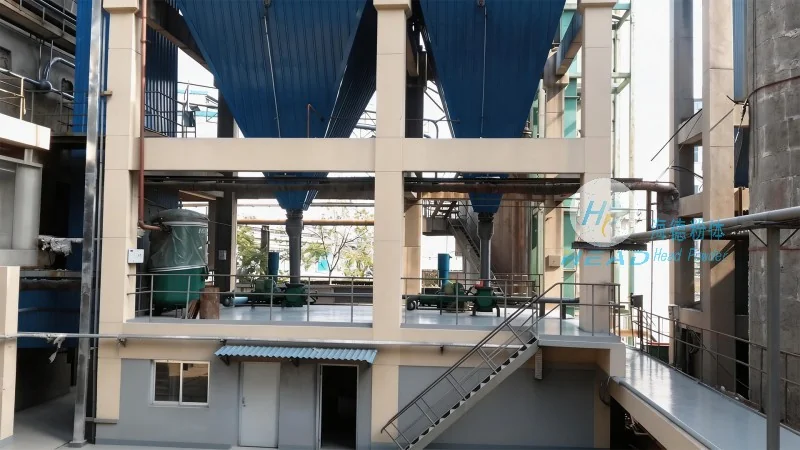
These systems are widely used in industries such as mining, chemical processing, and food production, where the efficient and safe transport of bentonite powder is essential. For example, in mining operations, bentonite is used as a drilling fluid and its transport requires precise control to avoid clogging or contamination. In chemical plants, the system ensures that the powder is delivered to processing units without loss or degradation. The operational advantages include reduced downtime, lower labor costs, and improved product quality due to consistent material handling. Furthermore, the system's ability to handle dusty environments without compromising safety makes it a preferred choice for many industries.
In conclusion, a bentonite powder pneumatic conveying system is a sophisticated and efficient solution for transporting fine powders like bentonite. The design principles, which focus on air-based transport and integrated components, provide a reliable and cost-effective method for material handling. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in the design and production of advanced pneumatic conveying systems tailored to the specific needs of various industries. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality equipment that meets the demands of modern material processing. By understanding the core components and operational logic of these systems, users can make informed decisions about implementing such technology in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top