With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk materials, maintaining a clean and efficient processing environment is crucial. A dust-free bulk material feeding pneumatic conveying system is a specialized solution designed to handle powders and granules without generating airborne dust, ensuring safety, hygiene, and operational efficiency. This article explores the concept of such systems and delves into their core design principles.
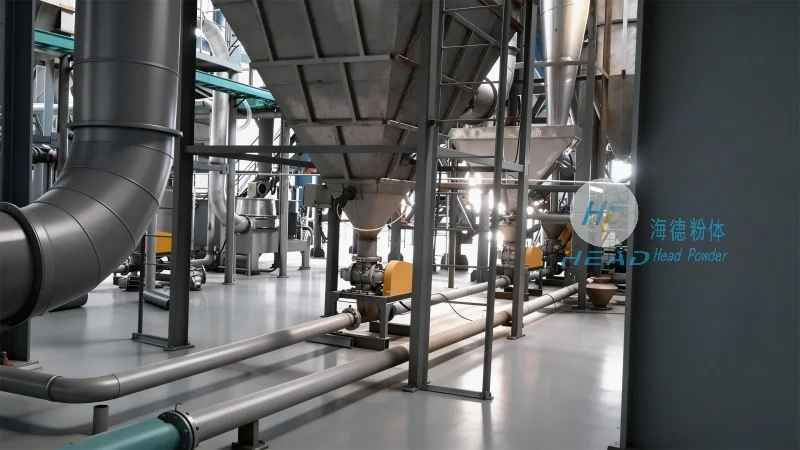
The dust-free bulk material feeding pneumatic conveying system is a technology that uses air or other gases to transport bulk materials from one location to another within a processing facility. Unlike traditional systems that may produce dust during material transfer, this system is engineered to minimize or eliminate dust emissions, making it ideal for applications where air quality and product purity are paramount. Common industries that benefit from this technology include pharmaceuticals, food processing, chemical manufacturing, and electronics.
The design of a dust-free bulk material feeding pneumatic conveying system revolves around several critical principles to ensure optimal performance and compliance with safety and environmental standards. These principles include:
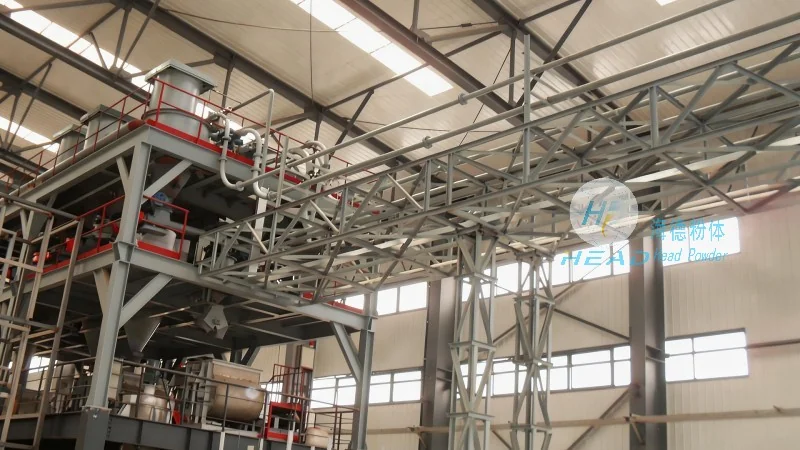
One of the fundamental design aspects is the use of sealed or enclosed pipelines and transfer points. This design prevents dust from escaping into the environment and maintains a controlled atmosphere within the system. The sealed pathways are typically made of materials resistant to corrosion and wear, such as stainless steel or specialized polymers, to ensure durability and long-term reliability.
Many dust-free systems operate under positive pressure, meaning the conveying air pressure is higher than the ambient air pressure. This approach ensures that any potential leaks will result in material being drawn back into the system rather than escaping into the workplace. Positive pressure operation also helps maintain a consistent flow of material and prevents contamination from external sources.
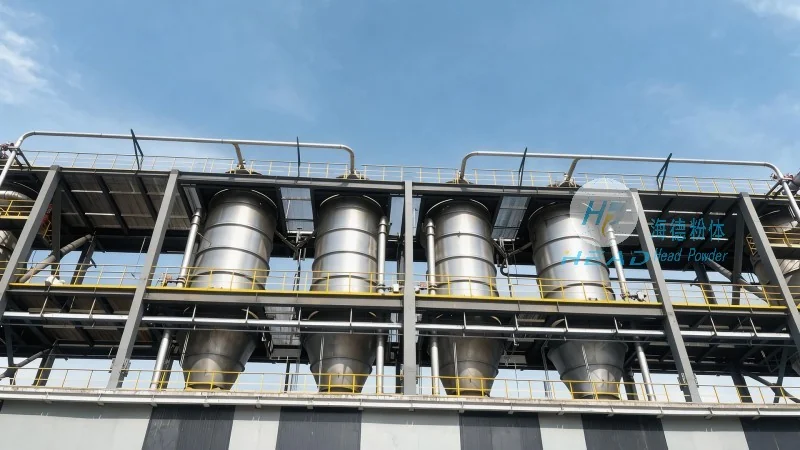
The system incorporates mechanisms for efficient material handling and separation. This includes components like feeders, cyclones, and filters that work together to ensure smooth material transfer and separation of any fine particles or contaminants. The design focuses on minimizing material degradation and ensuring that the conveyed material remains in its original state, which is essential for industries where product quality is non-negotiable.
Advanced control and monitoring systems are integrated into the design to manage the system's performance. These systems allow operators to adjust air pressure, flow rates, and other parameters in real-time, ensuring optimal operation and preventing issues such as blockages or overloading. The monitoring capabilities also help in maintaining the system's efficiency and longevity by detecting and addressing potential problems early.
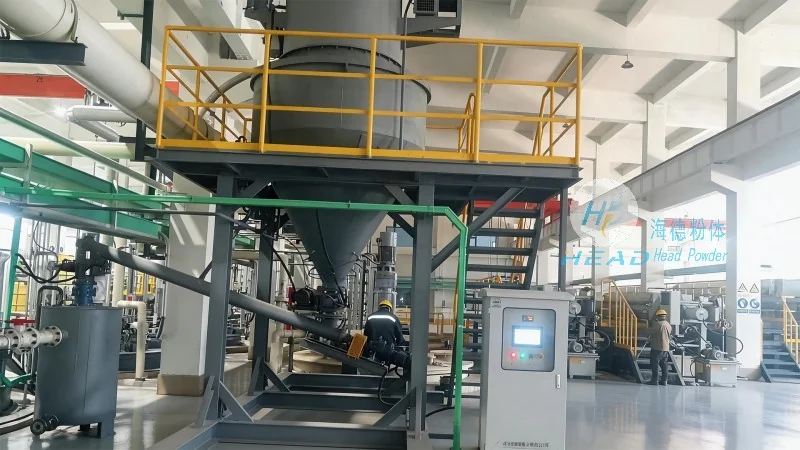
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing dust-free bulk material feeding pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's products are engineered to meet stringent safety and environmental standards, ensuring reliable performance and long-term value for clients.
HeadPowder is committed to delivering solutions that enhance operational efficiency while maintaining the highest standards of safety and hygiene. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to develop cutting-edge material handling systems. By prioritizing customer needs and adhering to industry best practices, HeadPowder has established itself as a trusted partner in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top