

What is a Soil Pneumatic Conveying Equipment? Introduction to the Structure and Principle of Powder
Soil pneumatic conveying equipment, also known as powder conveying systems, is a critical technology for the efficient transportation of bulk materials such as soil, powders, and granules. This equipment leverages compressed air or gas to move materials through a pipeline system, offering a dust-free, flexible, and automated solution for material handling in diverse industrial applications. The core function of these systems is to transport dry bulk materials from a source to a destination without relying on mechanical components like belts or buckets, making them ideal for environments where hygiene, cleanliness, and minimal maintenance are paramount.
Key Structural Components and Working Principle
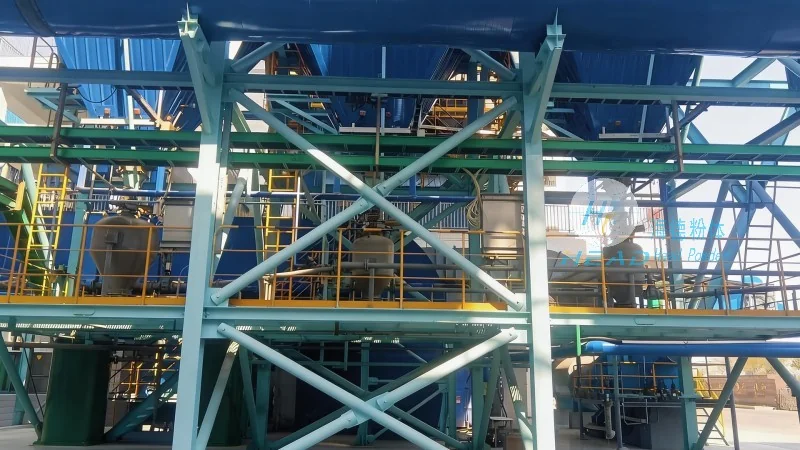
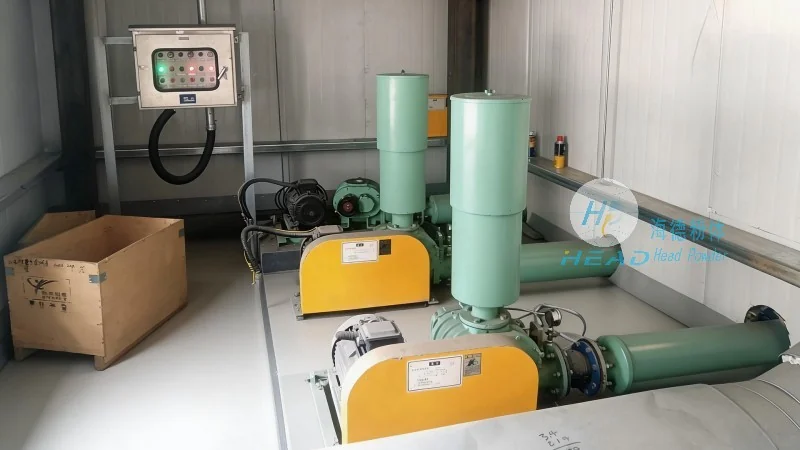
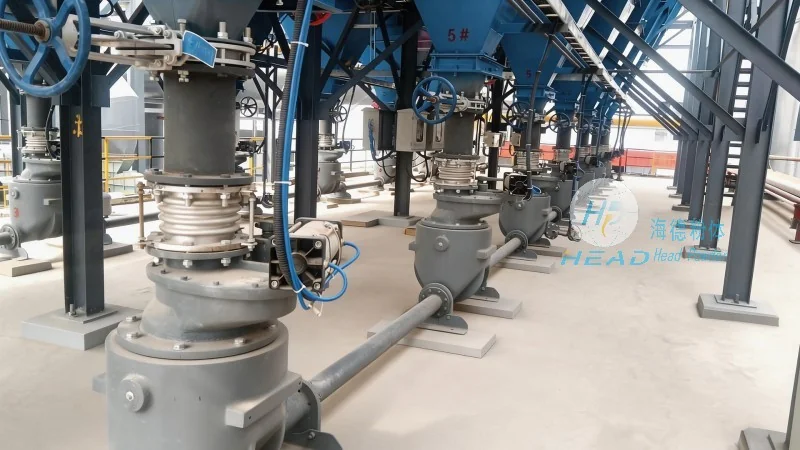
The structure of a typical soil pneumatic conveying system comprises several essential components that collaborate to ensure smooth material transport. The primary components include the material hopper, feeder, air compressor, conveying line, and discharge hopper. The material hopper is designed to store the bulk material, often equipped with a hopper liner and discharge valve to regulate flow. The feeder, typically a rotary valve or star feeder, ensures a consistent and controlled feed of material into the system. The air compressor generates the necessary pressure to create a flow of air through the conveying line, which carries the material particles along with it. The conveying line, made of metal or plastic, is selected based on the material being transported and operating conditions. The discharge hopper collects the material at the end of the pipeline, often incorporating a filter or cyclone separator to remove air and fine particles before release.
Application in Soil Transportation and Handling
For soil transportation, the pneumatic conveying equipment excels due to its ability to handle fine particles and prevent material degradation. The system efficiently transports soil from excavation sites to processing facilities or storage areas without manual handling, reducing labor costs and enhancing safety. The dust-free operation minimizes respiratory risks and contamination, a significant advantage in soil handling. Additionally, the system's flexibility allows for easy reconfiguration of the pipeline to adapt to changes in material flow or operational needs, ensuring adaptability in dynamic environments.
About Shandong HeadPowder Engineering Co., Ltd.
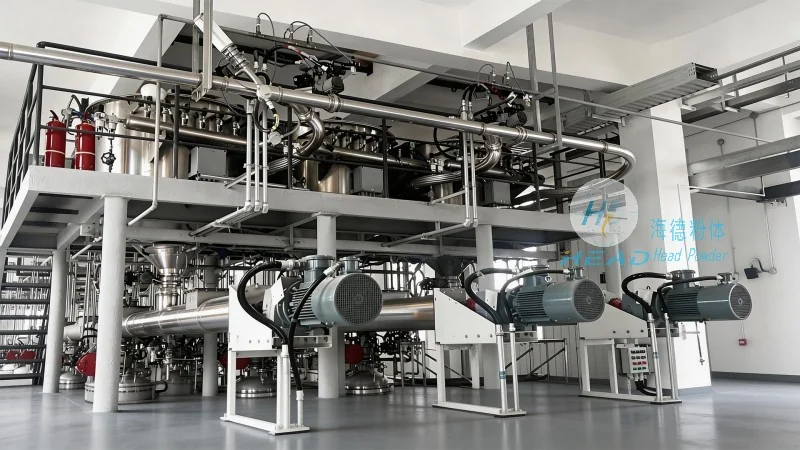
HeadPowder, a leading manufacturer of powder handling equipment, specializes in the design, production, and installation of advanced pneumatic conveying systems. With a commitment to innovation and quality, the company provides customized solutions tailored to the specific requirements of clients across industries such as construction, mining, and environmental management. HeadPowder's products are engineered to meet the highest standards of performance, durability, and efficiency, ensuring reliable operation in demanding conditions. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver superior products and services to global markets.