With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for alumina hydroxide applications. With a focus on efficient material handling solutions, the company provides comprehensive services from system design to on-site installation and commissioning. HeadPowder's expertise lies in optimizing material flow, ensuring minimal product degradation, and enhancing overall operational efficiency in industrial processes.
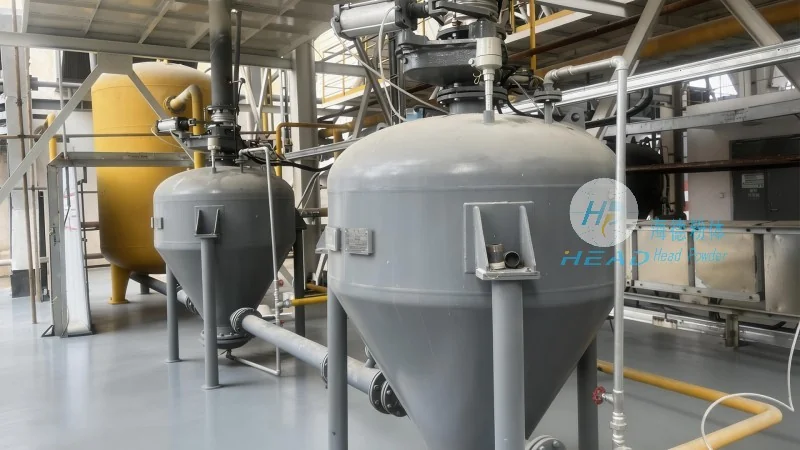
Alumina hydroxide, a key raw material in various industrial applications such as ceramics, pharmaceuticals, and chemical manufacturing, requires reliable and efficient transportation methods to maintain product quality and process continuity. Pneumatic conveying systems offer a non-contact, low-damage solution for handling fine powders like alumina hydroxide, addressing challenges such as dust control, material segregation, and environmental compliance. This article explores the classification of alumina hydroxide pneumatic conveying systems and their practical applications in industrial settings.
Alumina hydroxide pneumatic conveying systems can be broadly categorized into two main types based on the conveying principle: pressure and vacuum systems. Each type has distinct characteristics and is suitable for different operational requirements.
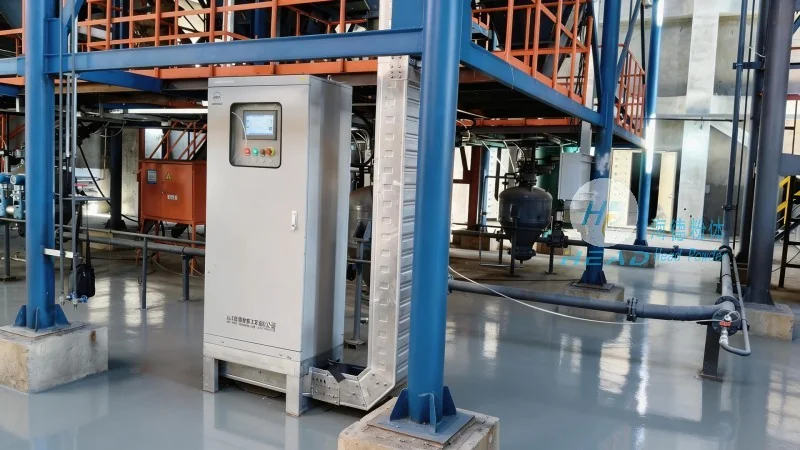
Pressure systems utilize compressed air or gas to push the material through a pipeline. They are commonly used for long-distance or high-volume material transport. Key components include a positive displacement blower, a hopper for material storage, and a pipeline network. The pressure system ensures consistent material flow and is ideal for applications requiring high throughput. HeadPowder's pressure systems are engineered to handle alumina hydroxide with particle sizes ranging from sub-micron to several microns, maintaining low pressure differentials to prevent product degradation.
Vacuum systems employ a vacuum pump to draw material from a source into a pipeline. These systems are suitable for short-distance transport or when the material needs to be collected from multiple points. They are often used in applications where the material is generated at a point and needs to be transferred to a central processing unit. Vacuum systems are particularly effective for handling fine powders as they minimize material spillage and dust emissions. HeadPowder's vacuum systems are designed with high-efficiency vacuum pumps and flexible hose connections, ensuring reliable material collection and transport for alumina hydroxide.
The application of alumina hydroxide pneumatic conveying systems varies across industries, with each sector requiring tailored solutions to meet specific operational demands.
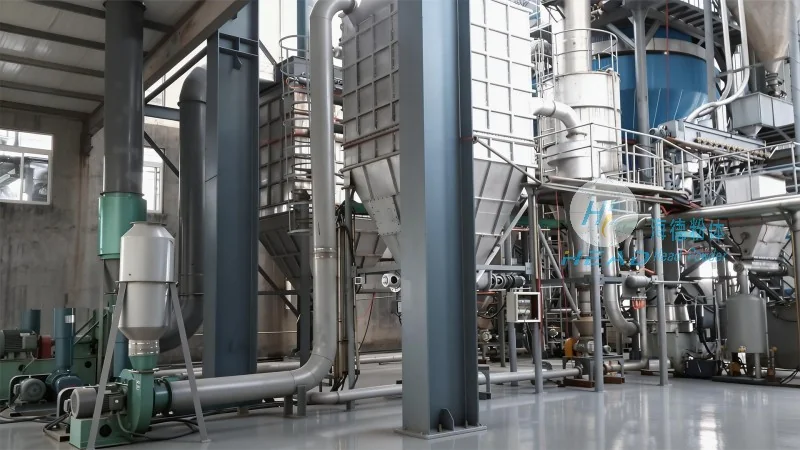
In the ceramic industry, alumina hydroxide is used as a raw material for producing high-purity alumina products. The pneumatic conveying system must ensure that the material is transported without contamination and with minimal moisture content. HeadPowder's systems are equipped with drying and filtration components to maintain the quality of alumina hydroxide during transport. The pressure system is often preferred for transporting large quantities of material from storage silos to production lines, ensuring a steady supply for ceramic manufacturing processes.
For pharmaceutical and chemical applications, the handling of alumina hydroxide requires strict adherence to hygiene and safety standards. Pneumatic conveying systems provide a closed-loop transport solution, preventing cross-contamination and protecting the material from environmental exposure. HeadPowder's systems are designed with stainless steel components and advanced filtration to meet the stringent requirements of the pharmaceutical industry. The vacuum system is commonly used for transferring alumina hydroxide from processing equipment to storage tanks, ensuring a clean and efficient material flow.
In environmental applications, alumina hydroxide is used as a coagulant in water treatment processes. The pneumatic conveying system must be capable of handling wet or moist material and ensuring proper mixing with other chemicals. HeadPowder's systems are equipped with specialized hoppers and pumps to handle wet alumina hydroxide, maintaining the material's integrity during transport. The pressure system is ideal for transporting the material from storage to treatment facilities, where it is mixed with water to form a slurry for wastewater treatment.
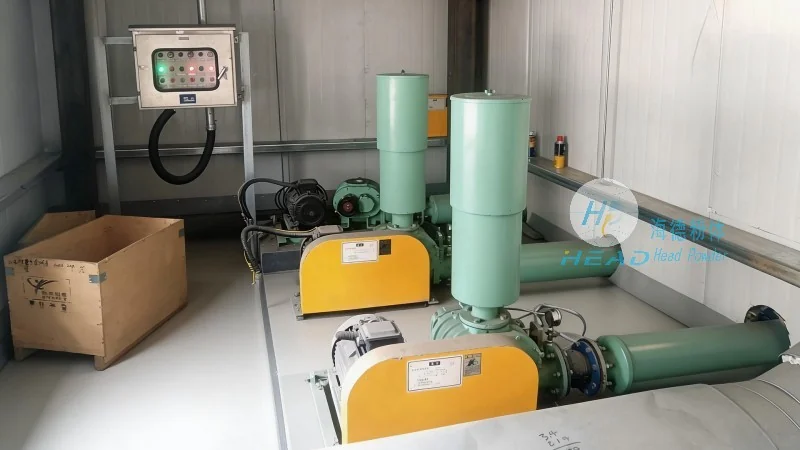
Implementing pneumatic conveying systems for alumina hydroxide offers several advantages over traditional methods such as belt conveyors or bucket elevators.
Firstly, the non-contact nature of pneumatic conveying minimizes product degradation, preserving the quality of alumina hydroxide. This is crucial for applications where the material's purity and particle size distribution are critical. Secondly, the closed-loop system reduces dust emissions and improves workplace safety, aligning with environmental regulations. Thirdly, the flexibility of pneumatic conveying allows for easy integration with existing industrial processes, enabling seamless material flow from storage to processing units. HeadPowder's systems are designed to optimize these advantages, providing reliable and efficient material handling solutions for alumina hydroxide applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top