With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient material handling is a critical factor in the flour and grain processing industry, where the seamless transfer of wheat flour and other powders from one location to another is essential for maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a preferred solution for this purpose, offering advantages such as reduced contamination, improved safety, and the ability to handle delicate materials like wheat flour without the need for mechanical components that could cause degradation. This article delves into the technical aspects of wheat flour pneumatic conveying, focusing on the two primary system types: negative pressure (suction) and positive pressure (blow) systems, and explores their applications in real-world scenarios.
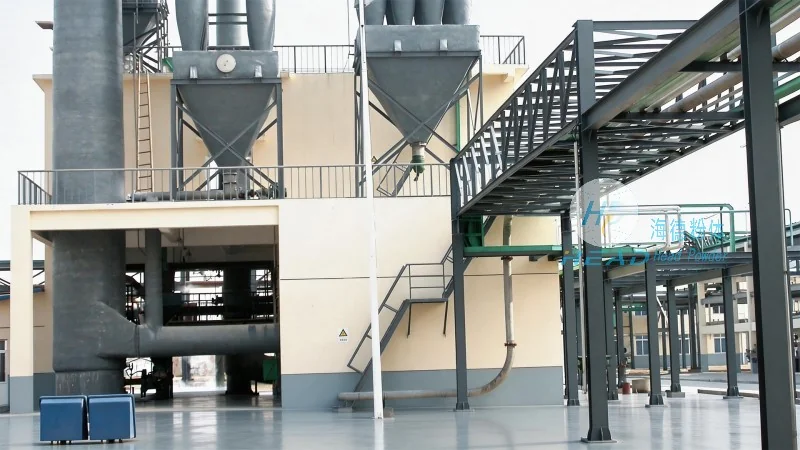
HeadPowder, as the name suggests, is a leading engineering company specializing in the design, manufacturing, and installation of pneumatic conveying systems for the food processing industry. With a strong presence in China, particularly in Shandong province, HeadPowder has built a reputation for delivering high-quality, customized solutions that meet the unique needs of flour mills, bakeries, and other grain processing facilities. The company's expertise lies in understanding the specific challenges of handling wheat flour and other fine powders, ensuring that their systems are optimized for performance, reliability, and durability.
Negative pressure systems operate by creating a low-pressure environment at the material intake point, drawing the wheat flour into the conveying line using a vacuum pump. This method is particularly effective for applications where the material is to be transferred from a higher elevation to a lower one, or when the source is located in a confined space. The key components of a negative pressure system include a vacuum pump, a filter to remove dust and particles from the air, and a discharge valve at the receiving end. The system works by pulling air and material through the line, with the filter ensuring that the air released at the discharge point is clean and safe for the environment. One of the main advantages of negative pressure systems is their ability to handle fine powders without causing excessive pressure buildup, which can lead to product degradation. However, they may require more maintenance due to the continuous operation of the vacuum pump and the need for regular filter cleaning.
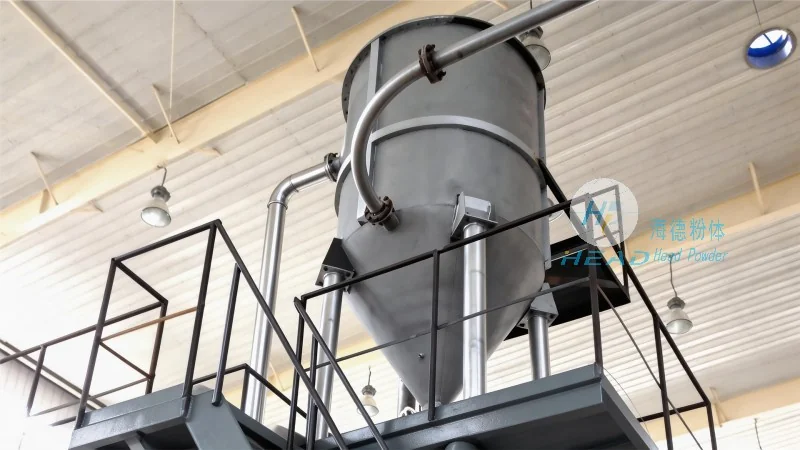
Positive pressure systems, on the other hand, use a blower or compressor to generate high-pressure air that pushes the wheat flour through the conveying line. This method is ideal for applications where the material needs to be transferred from a lower elevation to a higher one, or when the source is located in an open area. The system typically includes a blower, a material feeder, and a discharge valve at the receiving end. The high-pressure air creates a positive pressure inside the line, forcing the material to move forward. Unlike negative pressure systems, positive pressure systems do not require a filter at the intake point, as the material is not drawn in but rather pushed. This can reduce maintenance costs and increase system efficiency. However, positive pressure systems may generate more noise and require more energy to operate, especially when handling large volumes of material.
The choice between negative and positive pressure pneumatic conveying systems for wheat flour depends on several factors, including the layout of the facility, the distance and elevation changes between the source and destination, the volume of material to be conveyed, and the specific requirements of the processing line. For example, a mill that needs to transfer flour from a silo to a packaging machine located at a higher level may benefit from a positive pressure system, as it can efficiently move the material upward. Conversely, a facility that needs to collect flour from multiple points and transport it to a central storage area may find a negative pressure system more suitable, as it can draw material from various sources without the need for additional feeders at each point. HeadPowder engineers carefully evaluate these factors to recommend the most appropriate system for each client, ensuring optimal performance and cost-effectiveness.
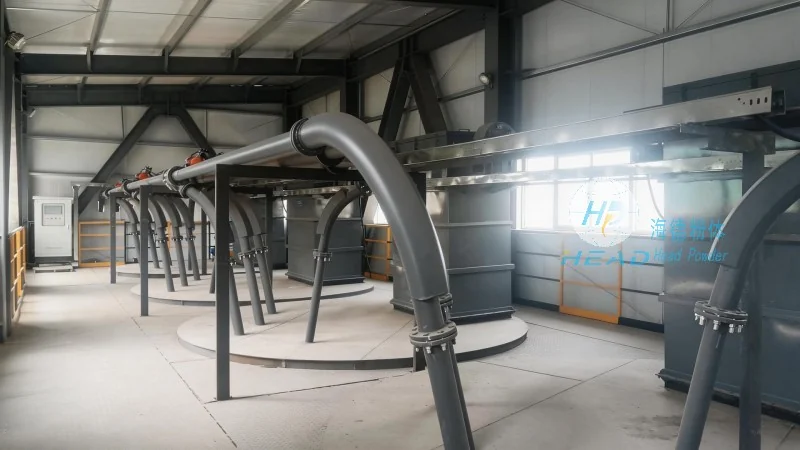
Both negative and positive pressure pneumatic conveying systems require regular maintenance to ensure long-term reliability and efficiency. For negative pressure systems, the vacuum pump and filter are critical components that need to be checked and serviced regularly. The filter must be cleaned or replaced as needed to prevent clogging, which can reduce the system's suction capacity and increase energy consumption. The discharge valve and material handling components, such as the intake hopper, also require periodic inspection to ensure they are free from blockages or wear. Positive pressure systems, while generally requiring less maintenance than negative pressure systems, still need to have the blower and material feeder checked for proper operation. The discharge valve and line connections should also be inspected for leaks, as even small leaks can reduce the system's pressure and affect performance. HeadPowder provides comprehensive maintenance services to its clients, including regular inspections, component replacement, and troubleshooting, to ensure that their pneumatic conveying systems operate at peak performance and minimize downtime.
Pneumatic conveying systems, whether negative or positive pressure, are essential tools for the efficient handling of wheat flour and other fine powders in the food processing industry. The choice between the two system types depends on the specific requirements of the application, with negative pressure systems excelling in material intake from multiple sources and positive pressure systems being ideal for material transfer over longer distances or to higher elevations. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing these systems, leveraging their expertise to deliver customized solutions that meet the unique needs of each client. By understanding the technical nuances of both system types and considering factors such as facility layout and material characteristics, HeadPowder ensures that their clients achieve optimal performance, reliability, and cost-effectiveness in their wheat flour handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top