With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a prominent enterprise in the field of pneumatic conveying technology, specializes in the research, development, and manufacturing of advanced dust-free automatic pneumatic conveying equipment. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring efficient, clean, and reliable material handling solutions. Based in Shandong, China, HeadPowder leverages its extensive experience and state-of-the-art technology to deliver customized solutions tailored to diverse industrial needs.
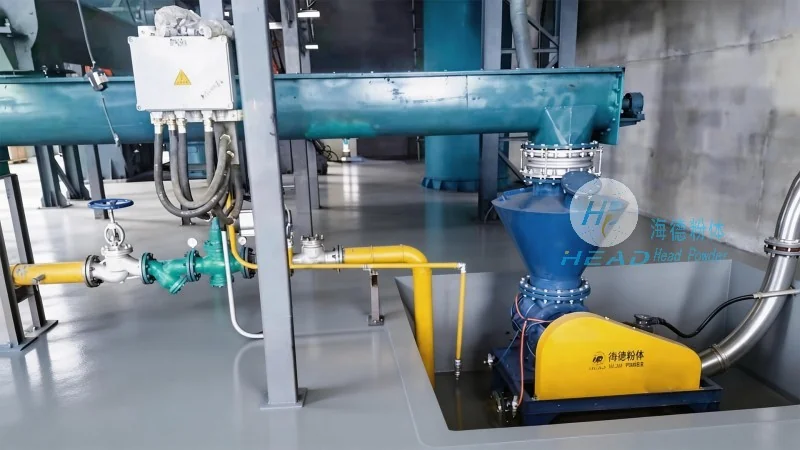
The dust-free automatic pneumatic conveying equipment from HeadPowder is designed to address the challenges of material transport in environments where contamination and dust control are critical. This equipment represents a significant advancement in pneumatic conveying systems, combining efficiency, safety, and environmental friendliness to meet modern industrial standards. The system is engineered to handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal risk of product degradation or cross-contamination.
The dust-free automatic pneumatic conveying equipment from HeadPowder is characterized by several key features that set it apart in the market. Firstly, its design incorporates advanced filtration and sealing mechanisms to ensure that the conveying process remains completely dust-free, protecting both the material and the surrounding environment. This is achieved through high-efficiency filters and airtight connections, which prevent any leakage of particles or air. Secondly, the equipment is equipped with intelligent control systems that allow for precise regulation of flow rates, pressure, and other operational parameters, ensuring optimal performance and energy efficiency. Additionally, the system is built with durable materials and robust construction, making it suitable for continuous operation in demanding industrial settings.
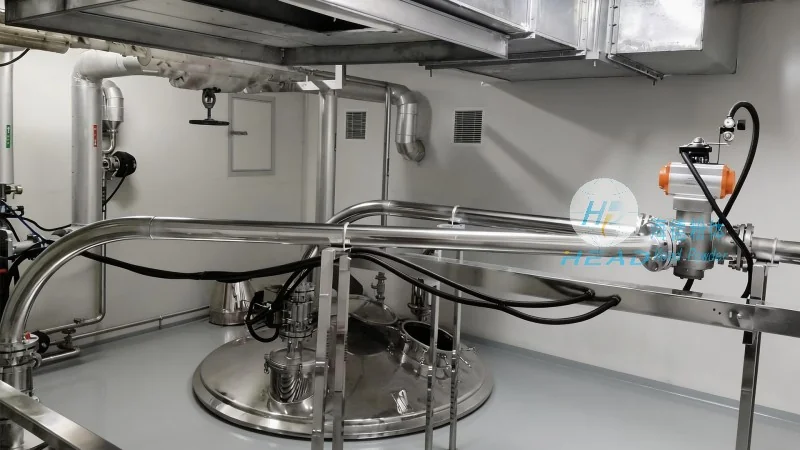
Applications of this equipment span various industries, including pharmaceuticals, food processing, chemical manufacturing, and cement production. In the pharmaceutical industry, for example, the dust-free design is crucial for maintaining sterile conditions and preventing contamination of sensitive products. Similarly, in food processing, the equipment ensures that powders and granules are handled hygienically, meeting stringent food safety regulations. The versatility of the system also makes it suitable for handling materials in the chemical and cement sectors, where efficiency and reliability are paramount.
The structural design of the dust-free automatic pneumatic conveying equipment is a result of meticulous engineering to ensure both functionality and durability. The system typically consists of several key components, including a hopper for material storage, a rotary valve or feeder for controlled material discharge, a conveying pipe network, a fan or blower for air supply, and a filter system for air purification. Each component is carefully integrated to create a seamless and efficient operation.
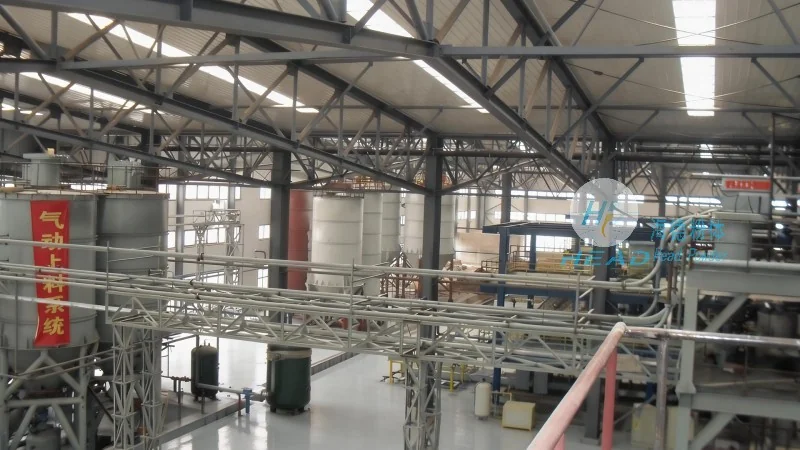
The working principle of the equipment is based on the pneumatic conveying method, where material is transported through a pipeline using compressed air. The process begins with the material being fed into the hopper, where it is then transferred to the feeder. The feeder controls the flow of material into the conveying pipe, while the fan generates the necessary air pressure to move the material through the system. As the material travels through the pipe, it is mixed with the air, forming a slurry-like mixture that is propelled forward by the air flow. The filter system at the end of the pipe removes any residual particles from the air, ensuring that the exhaust air is clean and safe for the environment.
A key aspect of the equipment's design is the use of positive pressure or negative pressure systems, depending on the specific application and material characteristics. Positive pressure systems are commonly used for conveying materials over longer distances or to multiple destinations, as they provide consistent air pressure throughout the pipeline. Negative pressure systems, on the other hand, are suitable for applications where the material needs to be transported from a higher to a lower elevation, as they create a vacuum that pulls the material through the pipe. The choice of system depends on factors such as the material's density, particle size, and the distance and elevation changes involved in the conveying process.
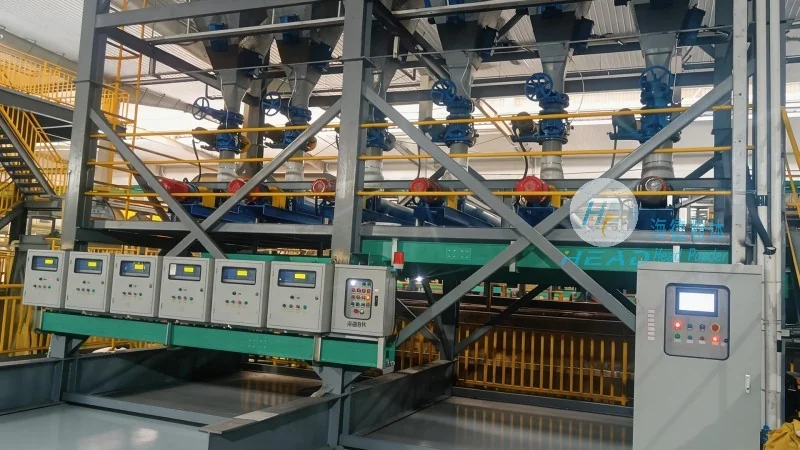
The dust-free automatic pneumatic conveying equipment from HeadPowder offers several advantages over traditional material handling methods. Firstly, it significantly reduces labor costs by automating the entire conveying process, eliminating the need for manual handling and reducing the risk of human error. Secondly, the equipment minimizes material loss and degradation, as the material is handled gently and in a controlled environment. This is particularly important for sensitive materials, such as pharmaceuticals or food products, where even small amounts of contamination can have significant impacts on product quality and safety.
Furthermore, the equipment enhances workplace safety by eliminating the need for manual handling of powders and granules, which can be hazardous if not handled properly. The dust-free design also reduces the risk of respiratory issues and other health problems associated with exposure to airborne particles. In terms of technical specifications, the equipment is available in various sizes and capacities to suit different industrial requirements. The system can handle material flow rates ranging from a few kilograms per hour to several tons per hour, depending on the specific model and configuration. The fan or blower used in the system can generate pressures up to several bars, ensuring efficient material transport even over long distances.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top