With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Feather pneumatic conveying equipment is a specialized system designed for the efficient and safe transport of lightweight materials such as feathers, powders, and granules. This equipment is widely used in industries like poultry processing, food processing, and material handling, where the gentle handling of delicate materials is crucial. The system operates by using compressed air to move material through a pipeline network, ensuring minimal product degradation and loss.
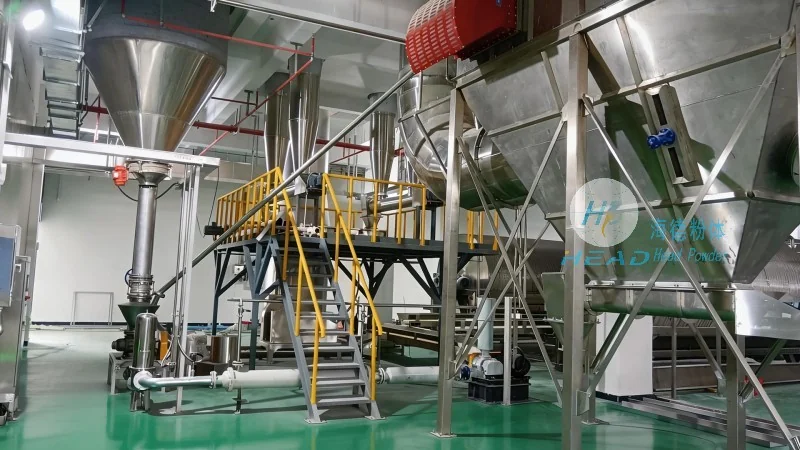
The core components of a feather pneumatic conveying system typically include a material hopper, a rotary valve or feeder, a conveying pipeline, a dust separator or cyclone, and a collection bin. The process begins with the material being fed into the hopper from a storage silo or container. The rotary valve then regulates the flow of material into the pipeline, ensuring a consistent feed rate. Compressed air is introduced at one end of the pipeline, creating a low-pressure zone that draws the material particles into the air stream. As the mixture travels through the pipeline, it passes through the dust separator, where larger particles and dust are separated from the air. The cleaned air is then released, while the separated material is collected in the bin. The system's design ensures that the material is conveyed gently, preventing breakage or contamination, which is essential for delicate products like feathers.
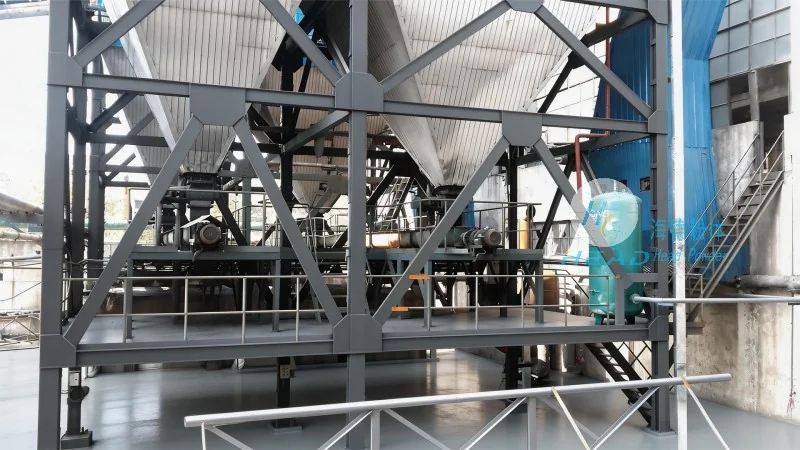
One of the primary advantages of this equipment is its ability to handle lightweight, low-density materials that are difficult to transport using traditional methods like belt conveyors or screw conveyors. The pneumatic system provides a gentle and continuous flow, reducing product damage and improving overall efficiency. Additionally, the enclosed pipeline design minimizes dust emissions and contamination, making it suitable for food-grade applications. The system also offers flexibility in terms of layout, as the pipeline can be configured to follow the existing facility layout, optimizing space utilization. Furthermore, the equipment is relatively easy to maintain, with components like the rotary valve and dust separator being accessible for routine checks and cleaning.
Feather pneumatic conveying equipment is particularly valuable in the poultry processing industry, where feathers are a byproduct that needs to be collected and processed. The system efficiently transports feathers from the processing line to storage or further processing facilities. The gentle handling of feathers prevents them from being broken or contaminated, which is critical for maintaining product quality. In food processing, the equipment can also handle other powders and granules, such as flour, sugar, or spices, ensuring that these delicate materials are transported without degradation. The system's ability to maintain a clean and hygienic environment is essential for meeting food safety regulations.
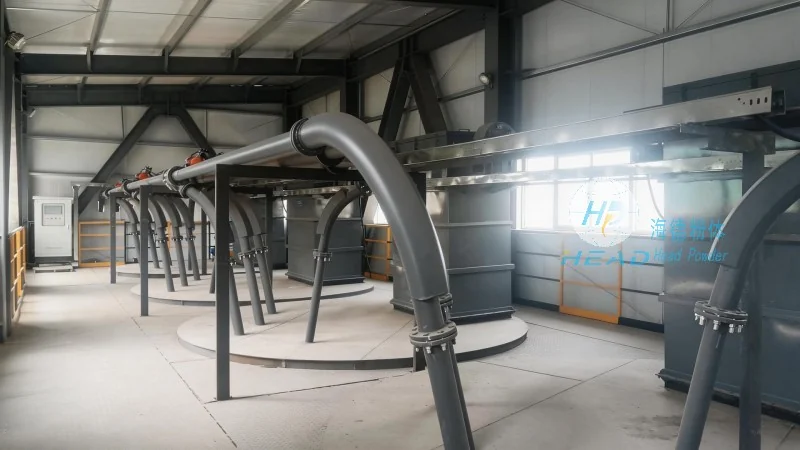
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pneumatic conveying systems and related equipment. The company is headquartered in Shandong, China, and has a strong reputation for producing high-quality, reliable equipment tailored to the needs of various industries. With years of experience in the field, headpowder has developed advanced solutions for material handling, focusing on efficiency, durability, and safety. The company's products are designed to meet the specific requirements of each application, ensuring optimal performance and minimal downtime. HeadPowder Engineering Co., Ltd. is committed to providing innovative and sustainable solutions for material handling challenges, serving clients both domestically and internationally.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top