

Operation Process and Working Principle of Clinker and Fly Ash Material Pneumatic Conveying Equipmen
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for bulk materials. This article provides a detailed exploration of the operation process and working principle of a clinker and fly ash material pneumatic conveying equipment, highlighting its efficiency and reliability in industrial applications.
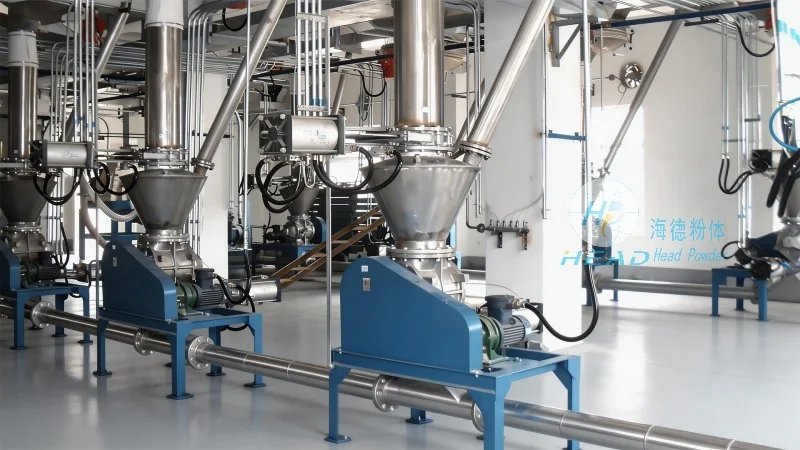
Working Principle of Pneumatic Conveying Equipment
The core of the pneumatic conveying system lies in the use of air as the conveying medium. In this equipment, compressed air is introduced into a pipeline, creating a flow that propels the clinker and fly ash particles through the system. The system typically operates under positive pressure, where the air pressure is higher than the ambient air pressure, ensuring continuous and unidirectional material transport. The design incorporates specialized components such as feeders, pipelines, and separation units that work in tandem to achieve effective material handling. The air flow velocity is carefully controlled to prevent material degradation and ensure smooth transport, while the system's sealing mechanisms minimize dust emissions and maintain operational safety.
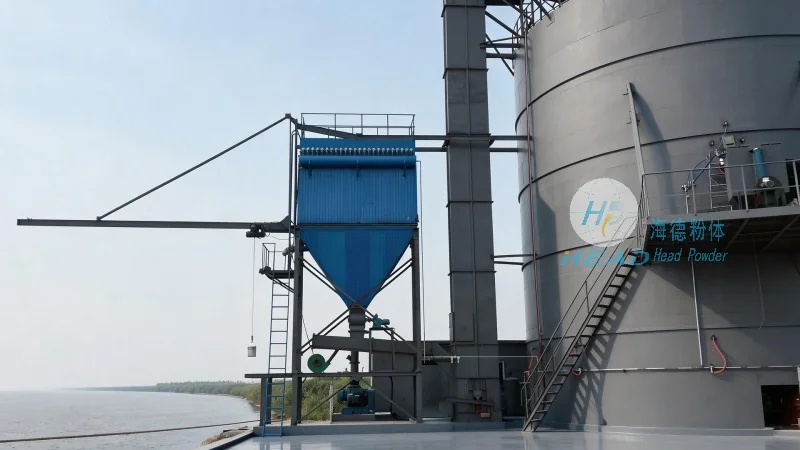
Operation Process of the Equipment
The operation process of the clinker and fly ash material pneumatic conveying equipment involves several key steps. Initially, the raw clinker and fly ash are stored in bulk storage silos or hoppers. A feeder, often a rotary valve or a screw feeder, then meters the material into the conveying pipeline at a controlled rate. Simultaneously, compressed air is supplied to the system, creating a pressure differential that drives the material forward. As the material travels through the pipeline, it is carried by the air stream, which can be either dense-phase or dilute-phase depending on the system design. The conveying line may include bends, expansions, or contraction sections, each designed to maintain the material's flow characteristics. At the discharge end, a separator or a cyclone unit is used to separate the material from the air stream, allowing the clinker and fly ash to be deposited into the target storage or processing equipment. The system also includes control valves and sensors to monitor pressure, flow rate, and material level, ensuring stable and efficient operation. Regular maintenance procedures, such as cleaning the pipelines and checking the air compressor performance, are essential to sustain the equipment's optimal performance over time.
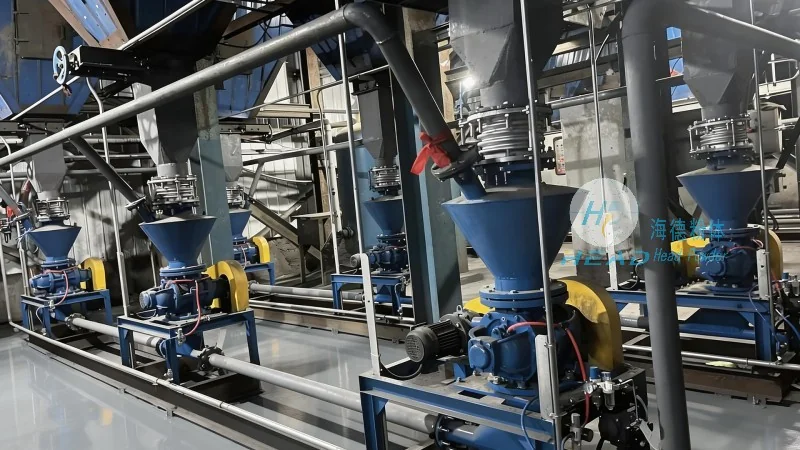
Technical Features and Advantages
HeadPowder's clinker and fly ash pneumatic conveying equipment is engineered with several technical features that enhance its performance and reliability. The system utilizes high-efficiency air compressors that provide consistent pressure and flow, ensuring smooth material transport even with varying material characteristics. The pipeline design incorporates corrosion-resistant materials, such as stainless steel or special coatings, to withstand the abrasive nature of clinker and fly ash. The equipment also includes advanced control systems that allow for real-time monitoring and adjustment of operational parameters, improving process efficiency and reducing downtime. Additionally, the system's compact design minimizes space requirements, making it suitable for both new installations and retrofit applications in existing cement plants. The equipment's ability to handle large volumes of material with minimal labor input, combined with its low maintenance requirements, makes it a cost-effective solution for bulk material handling in the cement industry.
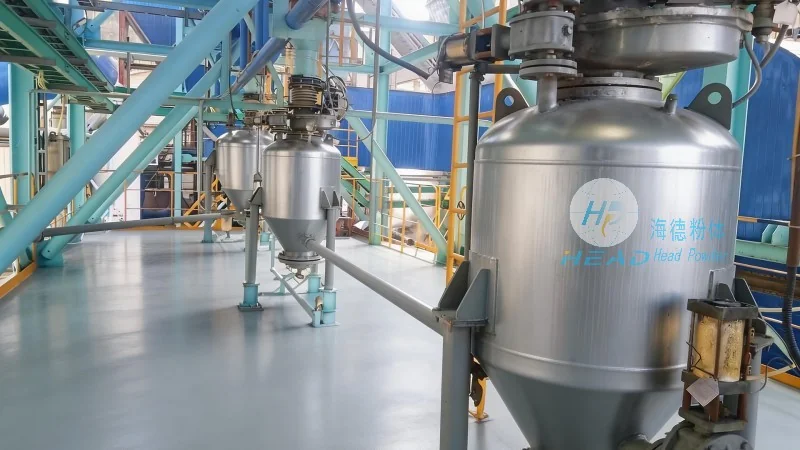
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of pneumatic conveying systems, with a focus on serving the cement, power, and construction industries. The company is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, customized solutions that meet the specific needs of its clients. With years of experience in the field, HeadPowder has developed a comprehensive range of equipment, including positive and negative pressure conveying systems, screw conveyors, and bulk material handling solutions. The company's commitment to innovation and quality ensures that its products are reliable, efficient, and environmentally friendly, contributing to the sustainable development of the industrial sector. HeadPowder's team of engineers and technicians provides comprehensive support, from initial consultation and system design to installation and after-sales service, ensuring that clients receive the best possible solution for their material handling challenges.