With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The capsule powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized device designed for the efficient and reliable transportation of capsule powders in industrial settings. This system is engineered to handle the unique challenges associated with capsule powder handling, such as maintaining product integrity, ensuring consistent flow rates, and minimizing material loss during transit. By integrating advanced mechanical and pneumatic components, the system provides a robust solution for pharmaceutical and food processing industries where precision and reliability are paramount.
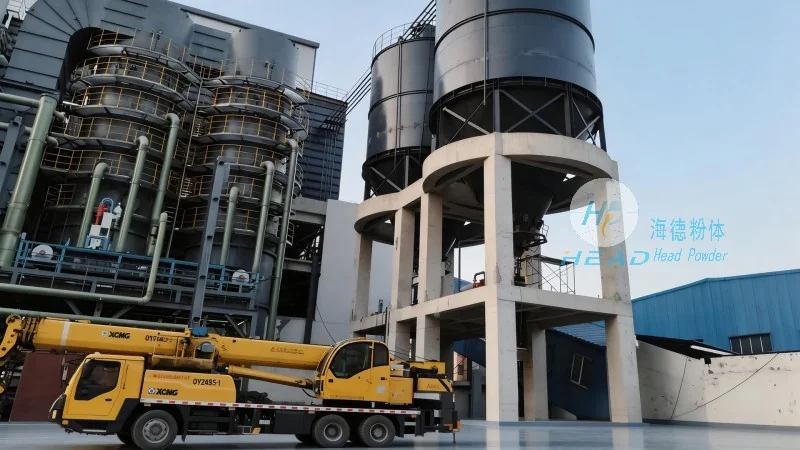
The capsule powder conveying system consists of several critical components that work in harmony to achieve optimal performance. The main components include a hopper for material storage, a conveying tube or duct system, a control unit for regulating air pressure and flow, and a discharge mechanism for delivering the powder to the next processing stage. The hopper is typically designed with a smooth interior surface to prevent powder sticking and ensure uniform material flow. The conveying tube is often made of stainless steel or other corrosion-resistant materials to maintain hygiene standards and prevent contamination. The control unit, equipped with sensors and valves, allows operators to adjust the air pressure and flow rate according to the specific characteristics of the capsule powder, such as particle size, density, and moisture content. The discharge mechanism, which may include a rotary valve or a slide gate, ensures a controlled and continuous release of the powder, preventing clogging and maintaining system efficiency.
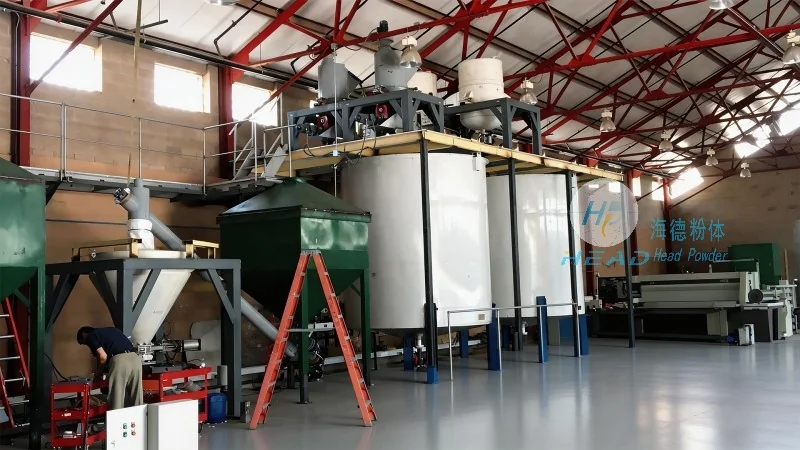
The operation of the capsule powder conveying system follows a systematic process that ensures smooth and uninterrupted material transport. The process begins with the loading of capsule powder into the hopper. The powder is then drawn into the conveying system by creating a pressure differential using compressed air. The air flow carries the powder particles through the conveying tube, while the control unit continuously monitors and adjusts the air pressure to maintain a consistent flow rate. As the powder travels through the system, it passes through any necessary filtration or separation stages to remove impurities or oversized particles. The discharge mechanism then releases the processed powder into the receiving container or the next processing equipment. Throughout the operation, the system's sensors provide real-time feedback on flow rates, pressure, and other critical parameters, allowing for immediate adjustments to maintain optimal performance. The entire process is designed to be automated, reducing the need for manual intervention and minimizing the risk of human error.
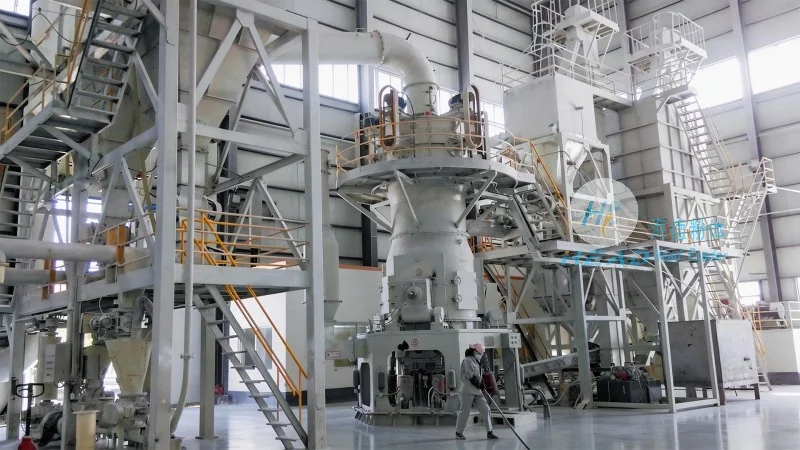
The working principle of the capsule powder conveying system is based on pneumatic conveying technology, which utilizes compressed air to transport dry powders. The system operates by creating a pressure difference between the hopper and the discharge point. When the control unit activates the air compressor, compressed air is introduced into the conveying tube, creating a low-pressure zone at the discharge end. This pressure differential causes the capsule powder to be drawn into the air stream and carried through the tube. The air flow velocity is carefully controlled to ensure that the powder particles are fully suspended in the air, preventing them from settling or clogging the system. The control unit continuously adjusts the air pressure and flow rate to maintain the optimal velocity for the specific powder characteristics. The system's design also incorporates features such as pulse or rotary air flow to enhance the conveying efficiency, especially for powders with high moisture content or cohesive properties. By leveraging the principles of fluid dynamics and particle mechanics, the capsule powder conveying system effectively transports the material while preserving its quality and integrity.
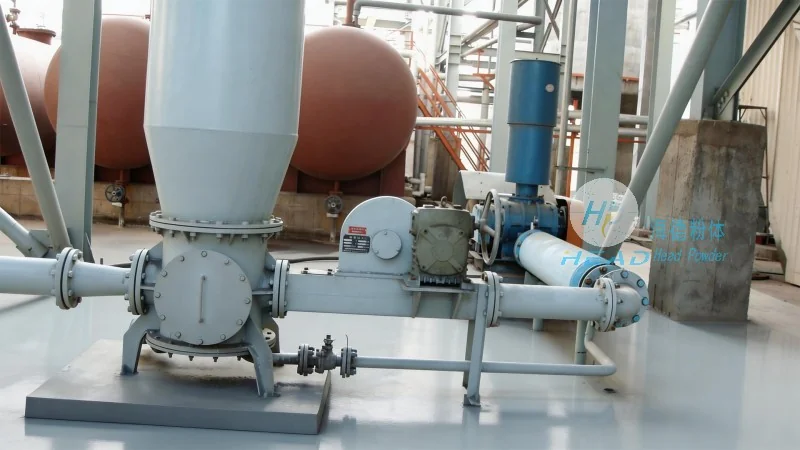
The capsule powder conveying system offers several advantages that make it an ideal choice for industries requiring precise and reliable powder handling. One of the key benefits is its ability to maintain product purity and integrity, as the system is designed to minimize contact with external contaminants and prevent cross-contamination. The stainless steel construction and smooth surfaces ensure that the powder remains free from dust or debris, which is crucial in pharmaceutical and food applications. Another advantage is the system's flexibility in handling different types of capsule powders, including those with varying particle sizes, densities, and moisture levels. The adjustable control unit allows operators to customize the system's performance to suit specific material characteristics, ensuring consistent and efficient transport. The system also provides energy efficiency, as it uses compressed air in a controlled manner, reducing energy consumption compared to traditional mechanical conveying methods. In terms of applications, the capsule powder conveying system is widely used in the pharmaceutical industry for transporting active pharmaceutical ingredients (APIs) and excipients, in the food industry for handling spices, powders, and supplements, and in other industries such as chemical and cosmetic manufacturing where precise powder handling is essential.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top