With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Intelligent material feeding pneumatic conveying systems represent a sophisticated solution for the efficient and precise handling of bulk materials in industrial settings. Developed by Shandong HeadPowder Engineering Co., Ltd., these systems integrate advanced technology to optimize material transport, feeding, and processing operations. This article explores the fundamental principles behind their operation and highlights key working scene characteristics that make them indispensable in modern manufacturing and processing industries.
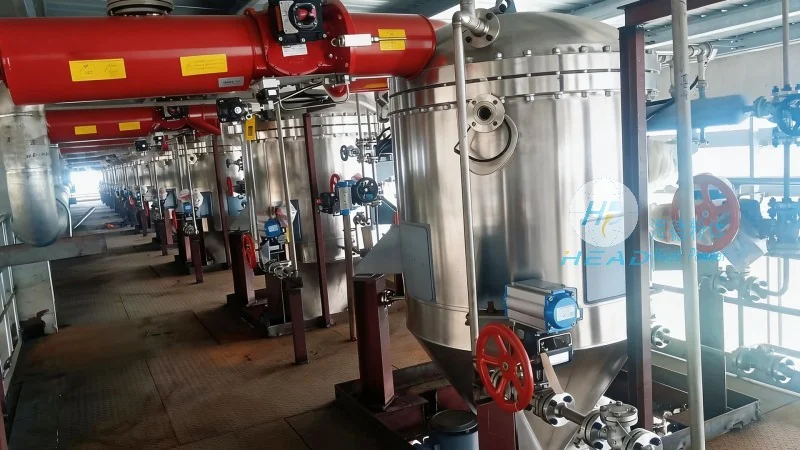
The operation of intelligent material feeding pneumatic conveying systems is grounded in the principles of pneumatic transport, which utilizes air flow to move bulk materials through a closed pipeline system. At the heart of this technology is the ability to create a controlled air flow that propels material particles from a source to a destination. The system typically consists of several key components, including a material hopper, a feeding device, a conveying line, and a receiver. The feeding device, often a rotary valve or a screw feeder, regulates the flow of material into the conveying line, ensuring consistent and controlled discharge. The conveying line itself is designed to withstand the pressure and flow conditions, with appropriate fittings and valves to manage the air and material mixture. The receiver collects the material at the end of the conveying process, completing the cycle. The intelligent aspect of these systems often involves advanced control systems that monitor and adjust parameters such as air pressure, material flow rate, and system pressure to maintain optimal performance and prevent issues like blockages or material degradation.
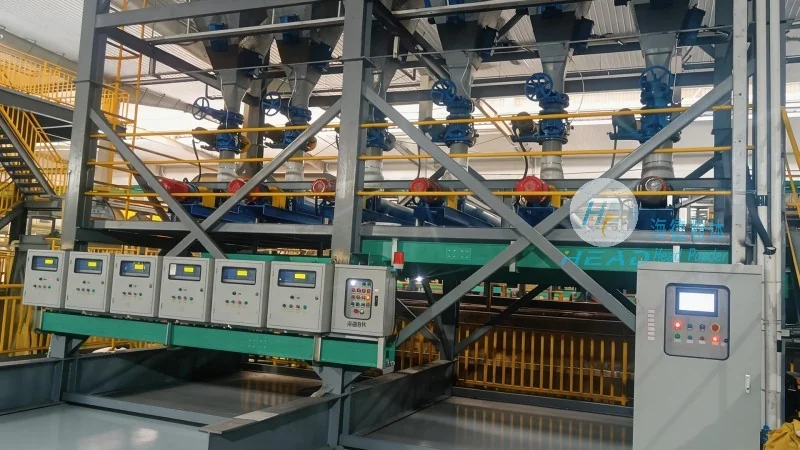
Intelligent material feeding pneumatic conveying systems are widely applied across various industrial sectors, each with distinct characteristics that define their operational environment. In the pharmaceutical industry, for example, these systems are used to handle sensitive powders with strict contamination control requirements. The intelligent control features ensure precise dosing and minimal particle degradation, meeting regulatory standards for product quality and safety. In the food processing sector, the systems are employed to transport ingredients like flour, sugar, and spices, where hygiene and material purity are paramount. The closed pipeline design and advanced cleaning capabilities of the equipment help maintain sanitary conditions, reducing the risk of cross-contamination. In the chemical and petrochemical industries, these systems handle a range of powders and granules, often with varying particle sizes and moisture content. The ability to adjust air flow and pressure allows for the efficient transport of these materials without causing degradation or agglomeration. Additionally, in the cement and mineral processing industries, the systems are used to convey raw materials and finished products, contributing to the overall efficiency of production lines. The working scene characteristics include high throughput requirements, the need for dust control, and the integration with other processing equipment, all of which are addressed by the intelligent design of the conveying systems.
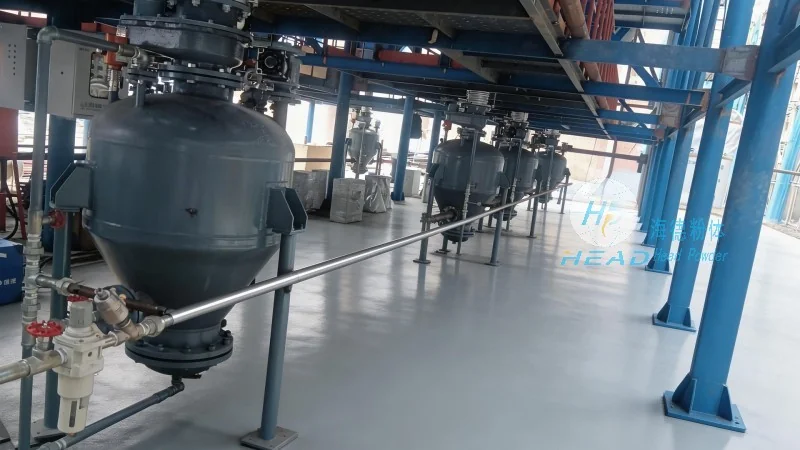
Shandong HeadPowder Engineering Co., Ltd. has integrated several advantages into their intelligent material feeding pneumatic conveying systems. One of the primary benefits is the ability to handle a wide variety of materials, from fine powders to coarse granules, with minimal maintenance. The systems are designed for durability and reliability, with components that can withstand the rigors of continuous operation. The intelligent control systems provide real-time monitoring and feedback, allowing operators to adjust settings quickly in response to changes in material properties or system conditions. This adaptability ensures consistent performance and reduces downtime. Another key feature is the energy efficiency of the systems, which is achieved through optimized air flow management and the use of high-efficiency motors. The closed pipeline design also contributes to better dust control and environmental compliance, as it prevents the release of airborne particles into the workplace. Furthermore, the systems are modular in design, allowing for easy expansion or integration with existing production lines. This flexibility makes them suitable for both new installations and retrofitting in existing facilities.
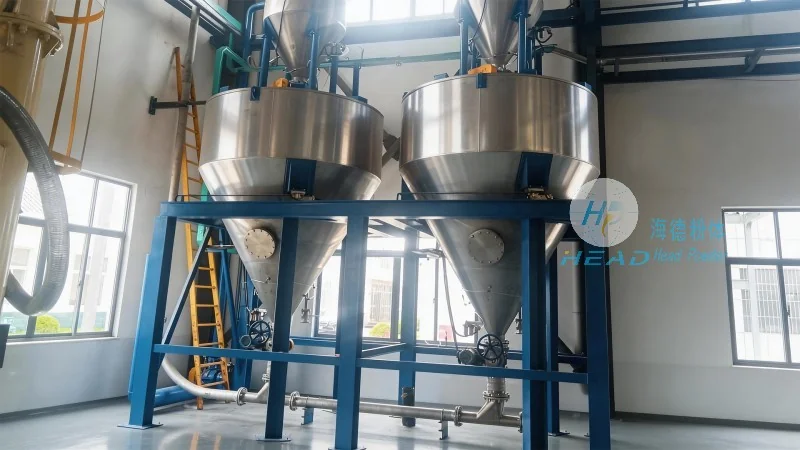
Intelligent material feeding pneumatic conveying systems, as developed by Shandong HeadPowder Engineering Co., Ltd., represent a significant advancement in bulk material handling technology. By combining advanced pneumatic transport principles with intelligent control systems, these systems offer superior performance, reliability, and adaptability across a range of industrial applications. The working scene characteristics, from pharmaceutical and food processing to chemical and mineral industries, highlight the versatility and importance of these systems in modern manufacturing. As industries continue to demand higher efficiency and precision in material handling, the intelligent features of these conveying systems will remain a critical component in achieving operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top