Principle and Working Scene Characteristics of Soda Ash Material Pneumatic Conveying Systems
Release time:2026-09-19 22:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for soda ash material handling. This article explores the fundamental principles behind such systems and highlights the key characteristics of their operational environments.
Understanding the Core Principles of Soda Ash Pneumatic Conveying Systems
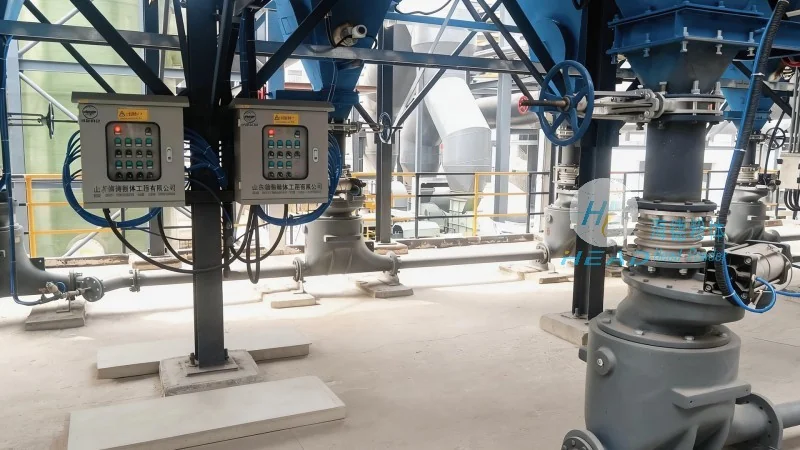
Pneumatic conveying systems utilize air or gas as the medium to transport bulk materials like soda ash from one location to another. The technology operates on the principle of creating a pressure differential between the conveying line and the ambient environment. By generating a vacuum or pressure within the system, the material is entrained and carried through the pipeline. For soda ash, which is often a fine, dry powder, this method offers several advantages over traditional mechanical conveyors, including reduced dust generation, lower maintenance requirements, and the ability to handle materials in enclosed systems, minimizing environmental impact.
Key Working Scene Characteristics of Pneumatic Conveying Systems for Soda Ash
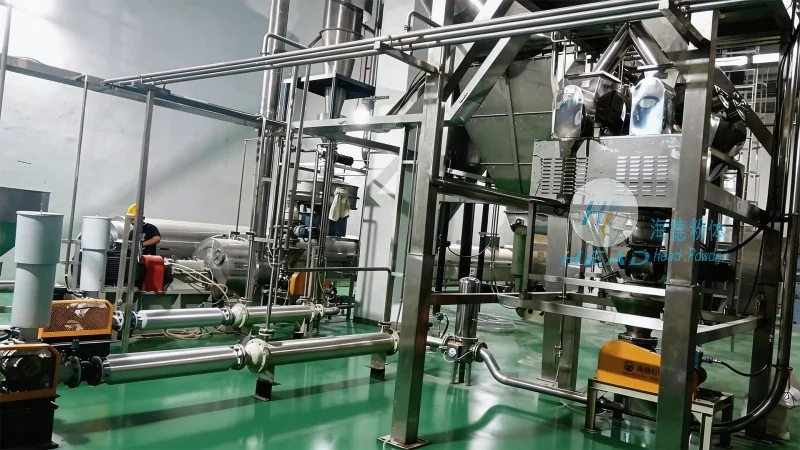
The operational characteristics of pneumatic conveying systems for soda ash are defined by several critical factors that influence system performance and efficiency. These include:
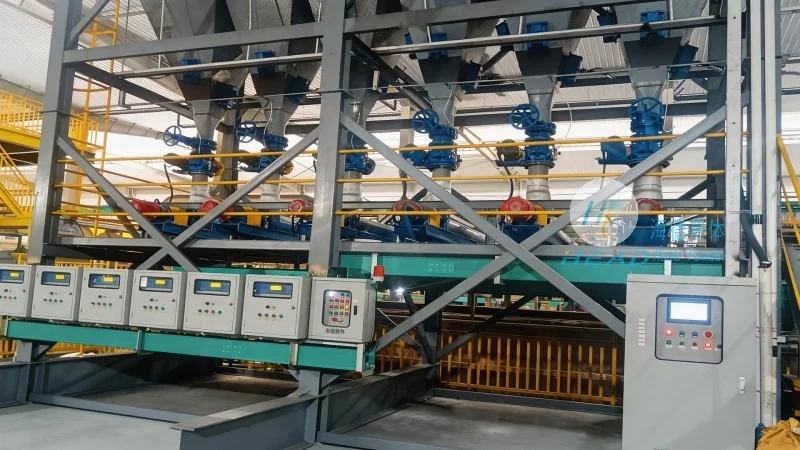
- Material Properties: Soda ash, typically in a fine powder form, has specific flow characteristics that affect how it behaves in the conveying process. Its density, particle size distribution, and moisture content are crucial in determining the optimal conveying velocity and pressure levels required to prevent blockages and ensure smooth transport.
- System Configuration: The layout of the conveying system, including the number of transfer points, vertical and horizontal runs, and the use of components like cyclones, filters, and silos, directly impacts the system's efficiency. A well-designed system minimizes pressure losses and ensures consistent material flow, which is essential for maintaining production line stability.
- Environmental Considerations: In industrial settings, especially where soda ash is processed, dust control is paramount. Pneumatic conveying systems are designed with enclosed pipelines and efficient filtration systems to contain dust, adhering to environmental regulations and ensuring a safe working environment for personnel.
- Energy Efficiency: Modern pneumatic conveying systems are engineered to optimize energy usage. By selecting the appropriate air velocity and system pressure, operators can achieve efficient material transport while minimizing energy consumption, contributing to cost savings and sustainability goals.
Application Scenarios in Industrial Settings
HeadPowder's pneumatic conveying systems for soda ash are widely applied in various industrial scenarios, including:
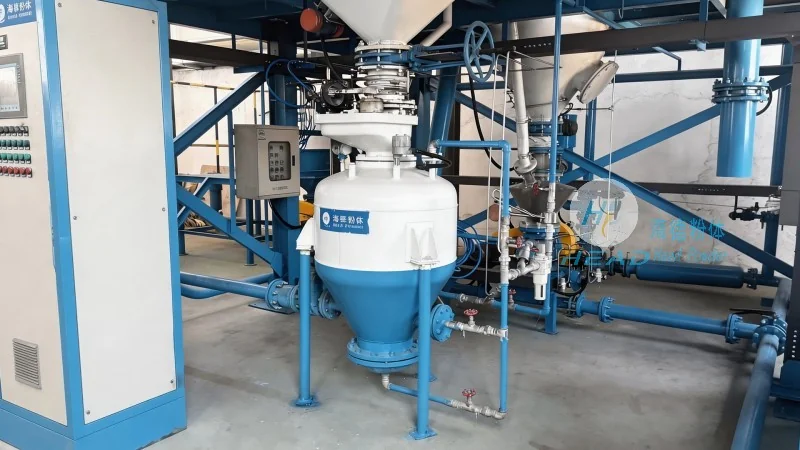
- Manufacturing Plants: In soda ash production facilities, these systems are used to transport raw materials to processing units and to move finished products to storage or packaging areas. The systems ensure a continuous and reliable supply chain, reducing downtime and improving overall plant productivity.
- Storage and Handling Facilities: For companies managing large inventories of soda ash, pneumatic conveying systems facilitate the transfer of material between silos, hoppers, and loading/unloading areas. This reduces the need for manual handling and enhances safety by keeping operations enclosed and dust-free.
- Transportation and Logistics: In logistics operations, pneumatic conveying systems can be integrated into supply chains to move soda ash from production sites to distribution centers or ports. This method offers a flexible and efficient alternative to traditional truck or rail transport, especially for high-volume, fine-particle materials.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of specialized pneumatic conveying solutions for soda ash and other bulk materials. With a focus on engineering excellence and customer-centric design, the company delivers systems that meet the unique demands of industrial applications. By adhering to rigorous standards and leveraging advanced technology, HeadPowder ensures that its pneumatic conveying systems provide reliable, efficient, and sustainable material handling solutions for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China
