With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems. With a focus on precision and efficiency, the company has established itself as a trusted partner for industries requiring reliable powder handling solutions.
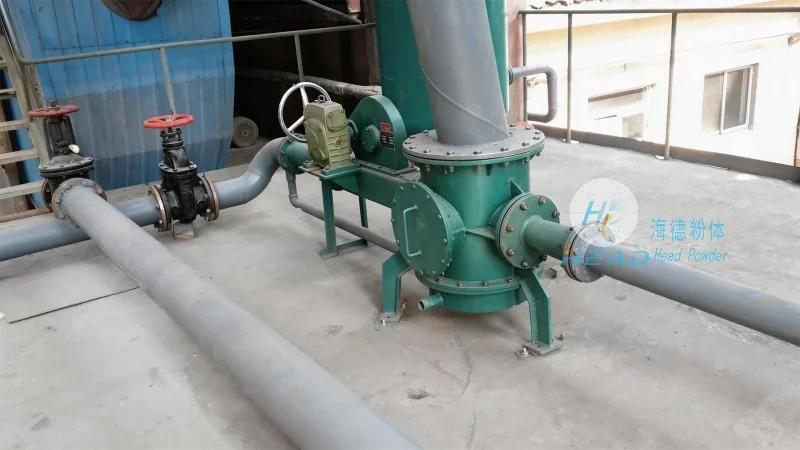
At the core of HeadPowder's product line is the chocolate powder pneumatic conveying machine, a sophisticated system engineered to transport chocolate powders with exceptional accuracy and minimal product degradation. This equipment is specifically designed to handle the delicate nature of chocolate powders, ensuring that the quality and flavor profile of the product are preserved throughout the conveying process. The system integrates advanced air management technology, allowing for gentle and controlled movement of the powder, which is crucial for maintaining the integrity of chocolate powders that are sensitive to pressure and temperature changes.
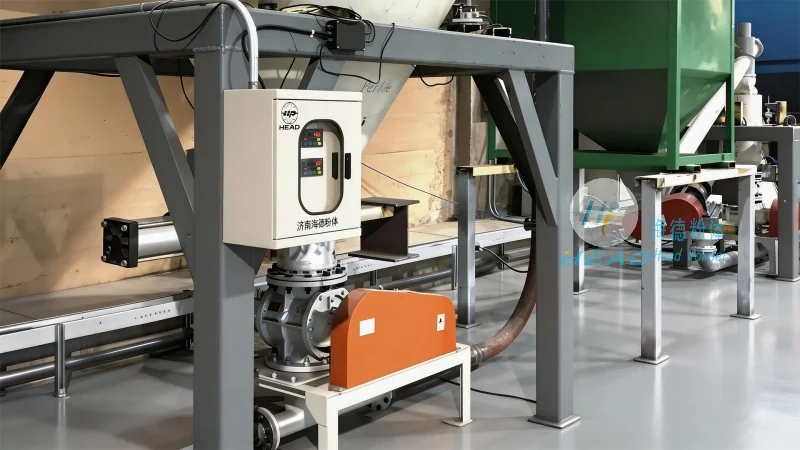
The chocolate powder pneumatic conveying machine operates on the principle of air-driven transport, where a stream of air is used to move the powder from a source to a destination. The system typically consists of a hopper, a venturi or a rotary valve, and a receiver. The hopper holds the chocolate powder, and as air is introduced, it creates a low-pressure zone that draws the powder into the conveying line. The venturi or rotary valve regulates the flow of both air and powder, ensuring a consistent and controlled rate of transport. This method of transport is particularly effective for chocolate powders because it minimizes direct contact with equipment surfaces, reducing the risk of contamination and product degradation. The air pressure and flow rate can be precisely adjusted to match the specific characteristics of the chocolate powder, such as its density and moisture content, ensuring optimal performance.
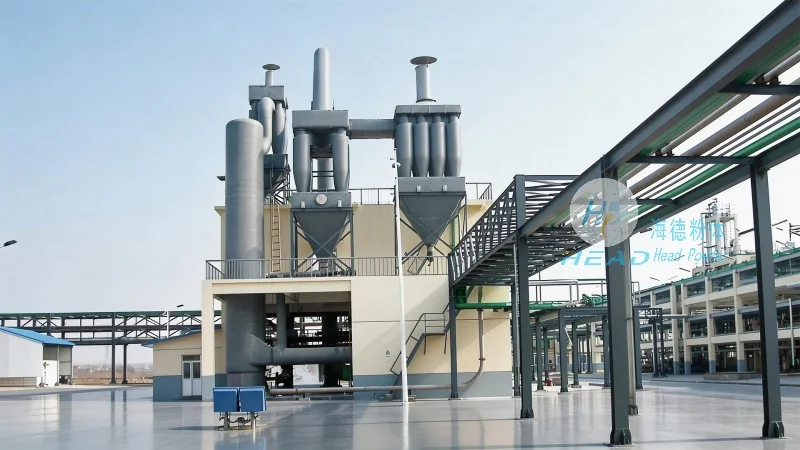
The chocolate powder pneumatic conveying equipment is designed for a variety of working scenarios, each tailored to meet the unique demands of chocolate production and processing. One of the primary applications is in chocolate manufacturing facilities, where the equipment is used to transport cocoa powder, sugar, and other ingredients from storage silos to mixing and processing units. The system's ability to handle large volumes of powder efficiently and with minimal downtime makes it ideal for high-throughput production lines. Another common application is in confectionery factories, where the equipment is used to convey finished chocolate powders to packaging lines or storage areas. The gentle handling of the powder ensures that the final product maintains its smooth texture and flavor, which is critical for consumer acceptance. Additionally, the equipment is suitable for use in environments where hygiene and cleanliness are paramount, such as in food processing plants, as the system is easy to clean and maintain, reducing the risk of cross-contamination.
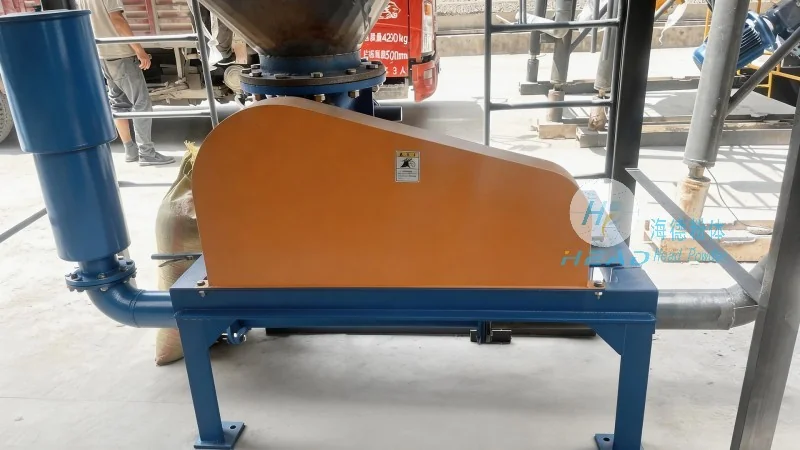
HeadPowder's chocolate powder pneumatic conveying machines offer several advantages that make them a preferred choice for chocolate manufacturers. The system's ability to handle delicate powders without causing agglomeration or breakage is a significant benefit, as it preserves the quality of the product. The adjustable air pressure and flow rate allow for customization to meet the specific requirements of different chocolate powders, ensuring optimal performance. The equipment is also designed for low maintenance, with easy access to components for cleaning and repair, reducing operational costs. Technical specifications include a conveying capacity ranging from 0.5 to 10 tons per hour, depending on the system configuration, and a pressure range of 0.5 to 2 bar. The system's compact design makes it suitable for installation in existing production facilities without requiring major structural modifications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top