With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring the efficient and reliable transport of calcium nitrite, specialized material handling systems are essential. This article explores the fundamental principles behind calcium nitrite material handling systems, as well as the key characteristics of their operational environments. The focus is on the technology and design elements that enable safe, efficient, and effective material transport, tailored to the unique demands of calcium nitrite handling in various industrial settings.
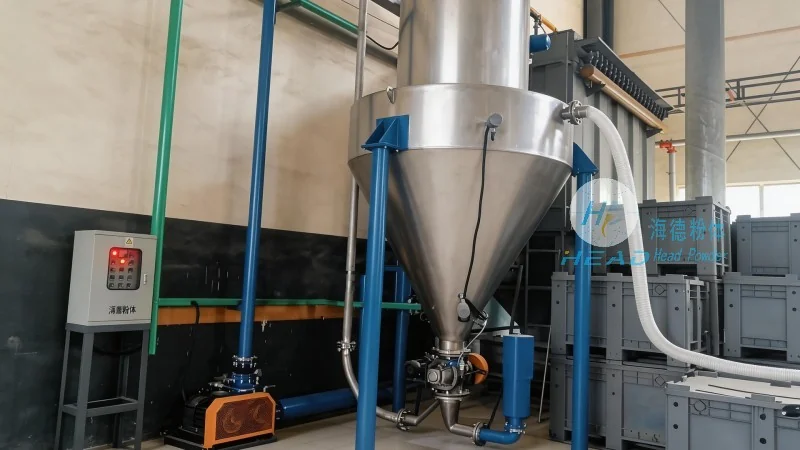
Headpowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of industrial material handling equipment. With headquarters located in Shandong, China, the company specializes in designing, manufacturing, and implementing customized solutions for diverse material transport needs. Headpowder's expertise lies in understanding the specific requirements of different industries, ensuring that their equipment not only meets but exceeds operational expectations. By leveraging advanced engineering and manufacturing capabilities, Headpowder delivers high-quality, durable, and efficient material handling systems that enhance productivity and safety in industrial operations.
Calcium nitrite is a chemical compound commonly used in industrial processes such as water treatment, concrete curing, and as a food preservative. Due to its properties and the nature of its applications, the handling of calcium nitrite requires specialized equipment to ensure safety, efficiency, and compliance with industry standards. Calcium nitrite material handling systems are engineered to address the challenges associated with this material, including its potential reactivity, handling requirements, and the need for precise control during transport. These systems integrate various components, such as conveyors, storage solutions, and control mechanisms, to create a cohesive and reliable material transport solution.
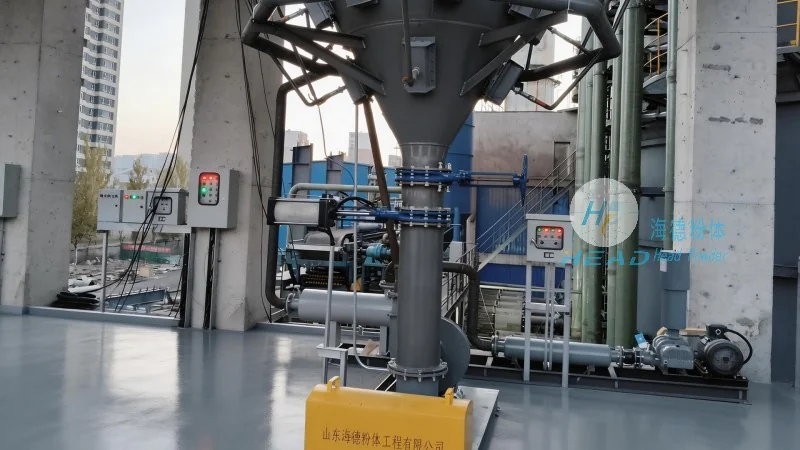
The operation of calcium nitrite material handling systems is based on several fundamental principles that ensure optimal performance and safety. One of the primary principles is the use of appropriate materials for construction to prevent chemical reactions or contamination. Calcium nitrite can be corrosive or reactive under certain conditions, so equipment components are typically made from materials like stainless steel, polyethylene, or other corrosion-resistant substances. This design choice minimizes the risk of material degradation and ensures the integrity of the transported substance. Another key principle is the implementation of proper ventilation and dust control measures. Calcium nitrite dust can be hazardous if inhaled, and thus, systems are equipped with dust collection and filtration systems to maintain a safe working environment. Additionally, the systems incorporate safety features such as emergency stop mechanisms, overload protection, and monitoring sensors to prevent accidents and ensure operational safety.
The operational environments where calcium nitrite material handling systems are deployed exhibit distinct characteristics that influence their design and functionality. These environments vary based on the industry and application, but common features include high-volume material handling, often in continuous or batch processing operations. The systems are typically integrated into larger production lines, requiring seamless coordination with other equipment and processes. The working scenes may also involve exposure to moisture, temperature fluctuations, or other environmental factors, necessitating robust construction and weather-resistant components. Furthermore, the systems are designed to accommodate the specific handling requirements of calcium nitrite, such as its bulk density, flow characteristics, and potential for dust generation. The operational settings may include indoor facilities like warehouses or processing plants, as well as outdoor applications in bulk storage or loading areas. Each of these scenarios demands tailored solutions that optimize material transport while maintaining safety and efficiency.

Implementing calcium nitrite material handling systems offers numerous advantages for industrial operations. Firstly, these systems enhance productivity by streamlining the material transport process, reducing downtime and labor costs associated with manual handling. The automated nature of the systems allows for consistent and reliable material movement, even in high-demand production environments. Secondly, the systems improve safety by minimizing human exposure to calcium nitrite, reducing the risk of respiratory issues or other health hazards. The integrated safety features and enclosed handling processes create a secure working environment. Thirdly, calcium nitrite material handling systems contribute to cost savings through reduced material waste and lower maintenance requirements. The durable construction and efficient operation result in lower long-term costs compared to traditional manual handling methods. Finally, these systems support compliance with industry regulations and standards, ensuring that operations adhere to safety and environmental guidelines. By addressing the unique challenges of calcium nitrite handling, these systems provide a comprehensive solution that meets both operational and regulatory requirements.
In conclusion, calcium nitrite material handling systems are critical components in industrial applications that require the efficient and safe transport of this chemical compound. The principles and characteristics of these systems are designed to address the specific needs of calcium nitrite, ensuring optimal performance, safety, and compliance. By leveraging advanced engineering and manufacturing, companies like Headpowder provide tailored solutions that enhance productivity and operational efficiency. The integration of proper materials, safety features, and environmental controls makes calcium nitrite material handling systems indispensable in modern industrial settings. As industries continue to rely on calcium nitrite for various applications, the importance of specialized material handling equipment becomes increasingly evident. The investment in such systems not only improves operational outcomes but also contributes to a safer and more sustainable industrial environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top