With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For sugar processing plants, efficient and reliable material handling is crucial to ensure smooth production processes. The sucrose material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to meet the specific needs of the sugar industry. This equipment is engineered to handle sucrose and related raw materials with precision, contributing to enhanced productivity and operational efficiency.
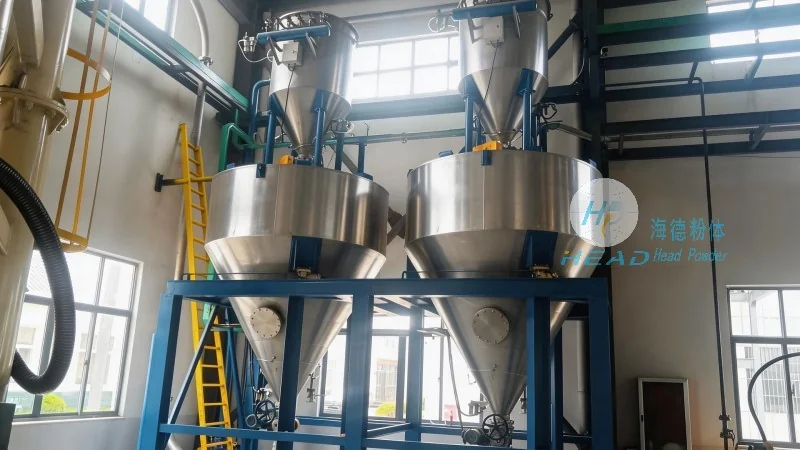
The core principle of the sucrose material handling system is to provide a seamless and continuous flow of materials from storage to processing units. The system integrates various components such as conveyors, elevators, and storage silos, working in tandem to minimize downtime and maximize throughput. By leveraging advanced engineering and material handling technologies, the equipment ensures that sucrose is transported safely and efficiently, reducing the risk of contamination and material loss.
Key components of the system include belt conveyors, screw conveyors, and pneumatic transport systems, each tailored to handle different types of sucrose materials. The belt conveyors are ideal for transporting bulk sucrose over long distances, while screw conveyors are used for vertical or inclined material movement. Pneumatic systems are employed for fine powders or granules, ensuring precise control over material flow. The integration of these components allows for a flexible and adaptable material handling solution that can be customized to meet the specific requirements of each sugar processing facility.
The sucrose material handling system is widely used in various working scenes within sugar processing plants. In the raw material reception area, the equipment efficiently receives and stores incoming sucrose, preparing it for subsequent processing. During the refining process, the system ensures that sucrose is transported to the refining units without any interruptions, maintaining consistent quality and purity. In the packaging and storage stages, the equipment handles finished products, ensuring they are stored in a controlled environment to prevent spoilage.
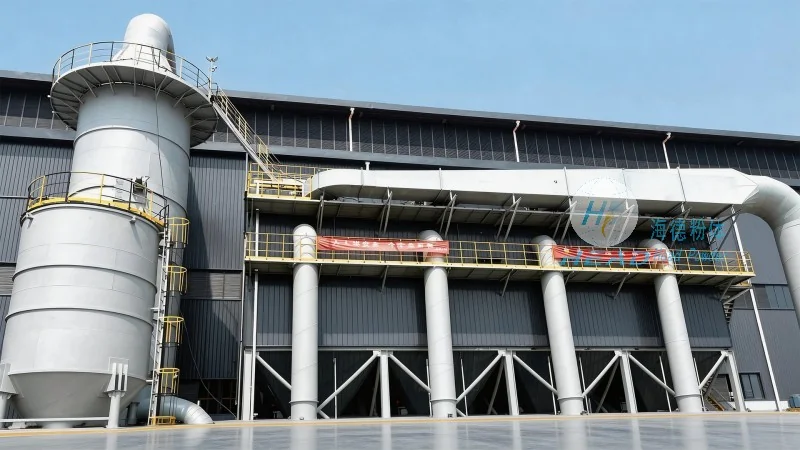
One of the notable characteristics of this system is its adaptability to different production scales. Whether it's a small-scale sugar mill or a large industrial facility, the system can be scaled to meet the operational needs. The modular design allows for easy expansion or modification as production demands change. Additionally, the system is designed with safety features to protect operators and equipment, ensuring compliance with industry standards and regulations.
The working scene also includes the integration of automation and control systems. Modern control panels and sensors are incorporated into the equipment, enabling real-time monitoring and adjustment of material flow. This automation not only improves operational efficiency but also reduces the need for manual intervention, minimizing human error and enhancing overall safety. The system's ability to integrate with existing plant infrastructure makes it a cost-effective solution for sugar processing facilities looking to upgrade their material handling capabilities.
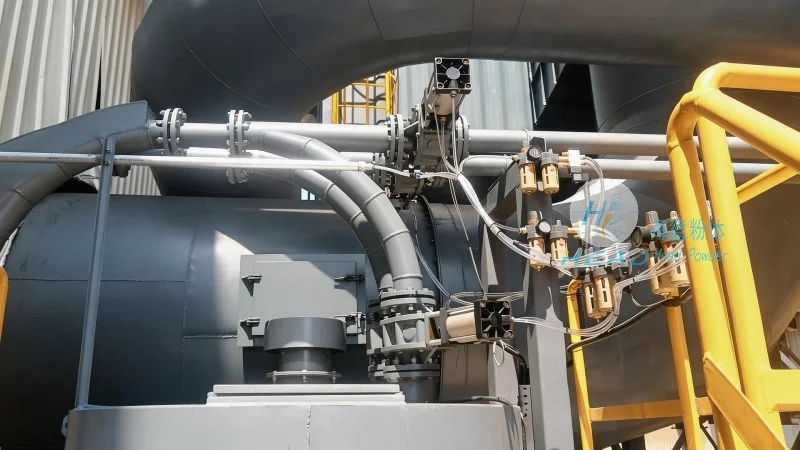
Implementing the sucrose material handling system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits to sugar processing plants. The primary advantage is the significant improvement in production efficiency, as the system minimizes material handling time and reduces downtime. This leads to increased output and reduced operational costs. Additionally, the system enhances product quality by ensuring consistent material flow and reducing the risk of contamination.
The system is particularly beneficial in large-scale sugar processing plants where high throughput is required. It can handle large volumes of sucrose, ensuring that the production line operates continuously without bottlenecks. The adaptability of the system also allows it to be used in various stages of sugar production, from raw material handling to final product packaging. This versatility makes it a valuable asset for sugar manufacturers looking to optimize their operations.
Another key benefit is the reduction in labor costs. The automated nature of the system reduces the need for manual labor in material handling tasks, leading to lower operational expenses. Furthermore, the system's durability and low maintenance requirements contribute to long-term cost savings. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive support, including installation, maintenance, and technical assistance, ensuring that the equipment operates at peak performance throughout its lifespan.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top