With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Automatic material handling systems are integral to modern industrial operations, streamlining the movement of goods from one location to another with precision and efficiency. These systems are designed to automate the processes of transporting, storing, and managing materials, reducing manual labor and minimizing operational errors. The core components of such systems typically include conveyors, robotic arms, automated storage and retrieval systems (AS/RS), and control software that coordinates the entire workflow.
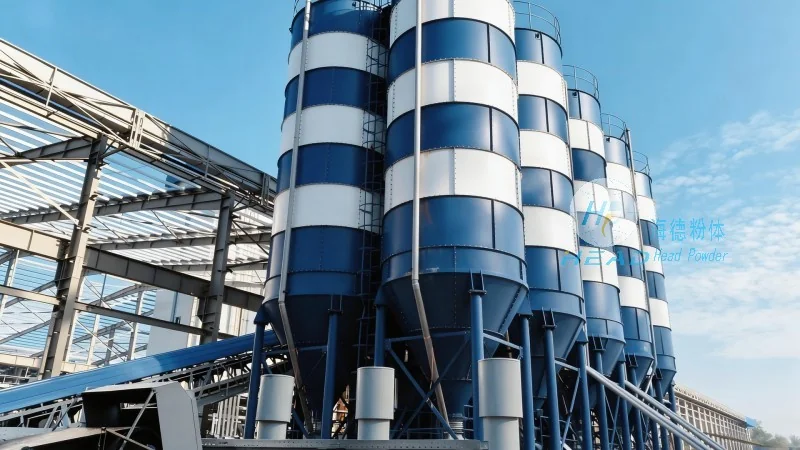
The fundamental principles of automatic material handling equipment revolve around mechanical motion, sensor technology, and intelligent control. Conveyors, for instance, use rollers or belts to move items horizontally or vertically, while robotic systems employ actuators and programming to perform complex tasks like picking, placing, and sorting. Sensor arrays, including cameras, laser scanners, and proximity detectors, enable the system to detect objects, track their position, and adjust the handling process in real-time. The control software acts as the brain, integrating data from various sensors and executing pre-programmed sequences to ensure smooth and reliable operation.
Several critical components contribute to the functionality of automatic material handling systems. Conveyor systems, which can be belt, roller, or chain-driven, are used for transporting items over short to medium distances. Robotic manipulators, equipped with grippers or suction cups, handle delicate or heavy objects with precision. Automated storage and retrieval systems (AS/RS) provide high-density storage solutions, using vertical lift modules or automated carousels to store and retrieve items based on demand. Additionally, control panels and user interfaces allow operators to monitor and adjust the system's parameters, ensuring optimal performance and adaptability to changing operational needs.
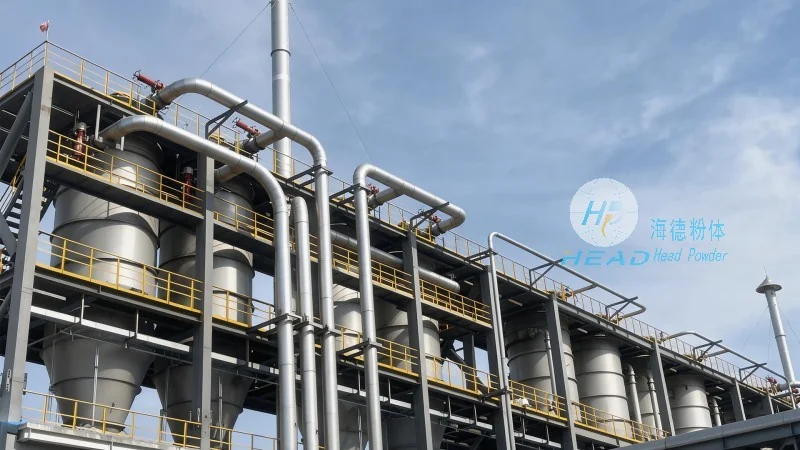
Automatic material handling equipment is widely applied across various industries, each with unique requirements that the systems address effectively. In manufacturing plants, these systems facilitate the smooth flow of raw materials to production lines and finished products to packaging areas, reducing bottlenecks and improving production throughput. In logistics and warehousing, automated conveyor networks and AS/RS systems enhance order picking accuracy and storage capacity, enabling faster order fulfillment and reduced labor costs. The food and beverage industry utilizes sanitary conveyor systems and robotic packaging solutions to maintain hygiene standards while increasing production speed. Similarly, in the pharmaceutical sector, automated systems ensure compliance with regulatory standards by providing traceability and contamination control. These applications highlight the versatility and adaptability of automatic material handling equipment to meet the diverse needs of modern industries.
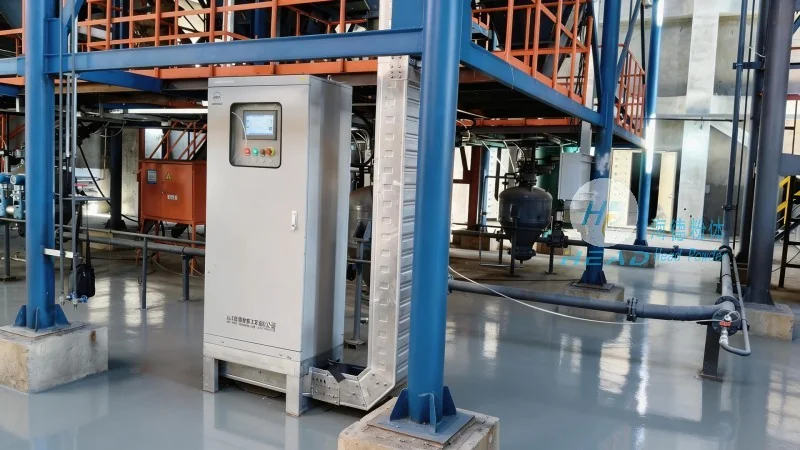
Adopting automatic material handling systems offers numerous benefits that enhance operational efficiency and cost-effectiveness. Firstly, automation significantly reduces labor costs by minimizing the need for manual handling, thereby lowering the risk of workplace injuries and associated insurance costs. Secondly, these systems improve accuracy and consistency, as they operate based on predefined parameters rather than human error. This leads to higher product quality and reduced waste. Thirdly, the integration of sensors and control software enables real-time monitoring and predictive maintenance, allowing for proactive issue resolution and extending the lifespan of equipment. Additionally, automated systems can operate 24/7, maximizing productivity and meeting the demands of high-volume operations. Finally, the scalability of these systems allows businesses to expand their operations without significant infrastructure changes, providing long-term flexibility and growth potential.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced automatic material handling solutions. With a focus on innovation and customer-centric design, the company specializes in developing customized systems tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians leverages cutting-edge technology to design and manufacture equipment that meets the highest standards of performance, reliability, and safety. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing and testing capabilities, ensuring that every product undergoes rigorous quality control before delivery. By combining technical expertise with practical application knowledge, HeadPowder delivers solutions that enhance operational efficiency and support sustainable business growth across various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top