With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Stone aggregate material handling equipment plays a crucial role in various industrial and construction applications. These specialized machines are designed to efficiently transport and manage stone aggregates, which are essential raw materials in the production of concrete, asphalt, and other building materials. The proper functioning of such equipment ensures smooth workflow, enhances productivity, and reduces operational costs in material handling processes.
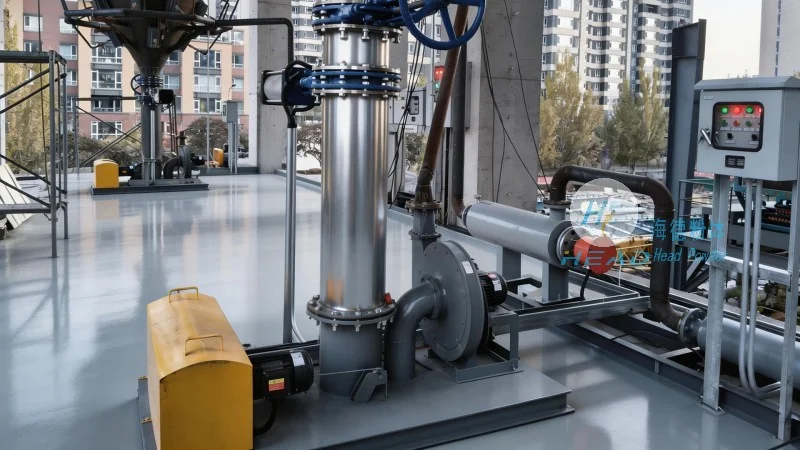
The core of stone aggregate material handling equipment lies in its mechanical and hydraulic systems. Typically, these devices utilize a combination of motor-driven mechanisms, such as belts, chains, or screw conveyors, to move bulk materials. The system often includes a hopper or feed inlet for material intake, a conveying section for transport, and an outlet for discharge. The motor provides the necessary power to drive the conveying components, while the control panel allows operators to adjust speed, direction, and other operational parameters. Advanced models may incorporate sensors and automation features to optimize performance and ensure safety during operation. The structural design is engineered to withstand the abrasive nature of stone aggregates, with robust frames and wear-resistant components to minimize maintenance and extend equipment lifespan.
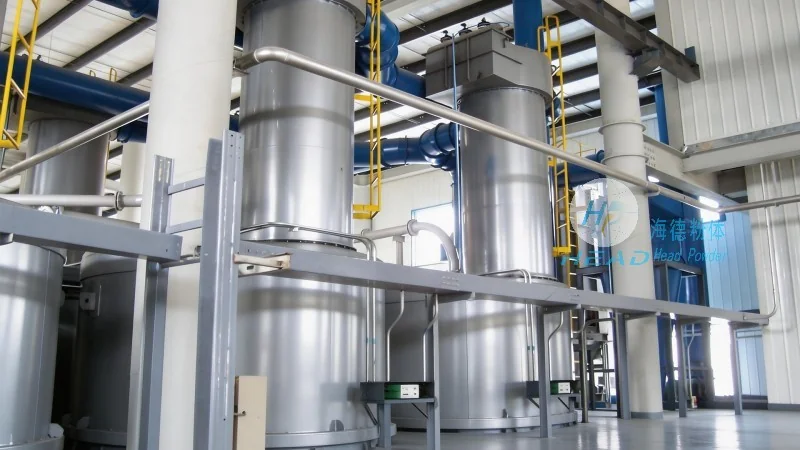
Stone aggregate material handling equipment is versatile and can be deployed in diverse working environments. In mining operations, these machines are used to transport crushed stone from extraction sites to processing facilities, ensuring a continuous supply of raw materials. On construction sites, they facilitate the movement of aggregates between storage areas, mixing plants, and job sites, supporting the efficient execution of concrete and pavement projects. In industrial settings, such as cement and asphalt production plants, the equipment aids in the internal logistics of raw materials, contributing to streamlined manufacturing processes. The adaptability of these devices allows them to handle different types of stone aggregates, including gravel, crushed rock, and sand, making them suitable for various applications. Additionally, the equipment's design considerations, like compact size for confined spaces or high-capacity models for large-scale operations, cater to the specific requirements of different working scenes. This flexibility ensures that operators can select the most appropriate equipment for their unique operational needs, enhancing overall efficiency and productivity.
HeadPowder, as a leading manufacturer in the field of material handling equipment, specializes in the design, development, and production of high-quality stone aggregate conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses in the construction and industrial sectors. HeadPowder's products are engineered to meet international standards and are known for their durability, efficiency, and reliability. The company's facilities, located in Shandong, China, leverage advanced manufacturing technologies and rigorous quality control processes to ensure that each piece of equipment meets the highest performance benchmarks. By focusing on the specific needs of clients, HeadPowder provides tailored solutions that enhance operational capabilities and reduce long-term costs. The company's expertise in material handling technology, combined with its dedication to customer service, makes it a preferred choice for organizations seeking reliable and efficient stone aggregate material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top