With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bioenzyme transportation is a critical process in various industrial applications, particularly in the biotechnology and pharmaceutical sectors. The efficient delivery of bioenzymes from production sites to processing or storage locations is essential for maintaining product quality and operational efficiency. This article explores the common methods used for bioenzyme transportation and highlights the advantages of HeadPowder's enzyme pneumatic conveying system.
Historically, bioenzyme transportation has relied on conventional methods such as manual handling, mechanical conveyors, and liquid or solid bulk transport. Manual handling, while cost-effective for small-scale operations, poses significant risks of contamination and human error. Mechanical conveyors, including belt conveyors and screw conveyors, are widely used but may not be suitable for delicate bioenzyme products due to potential mechanical stress and contamination risks. Liquid or solid bulk transport methods, like tank trucks or bulk containers, are often used for larger volumes but can lead to degradation of the enzyme's activity if not handled under optimal conditions.
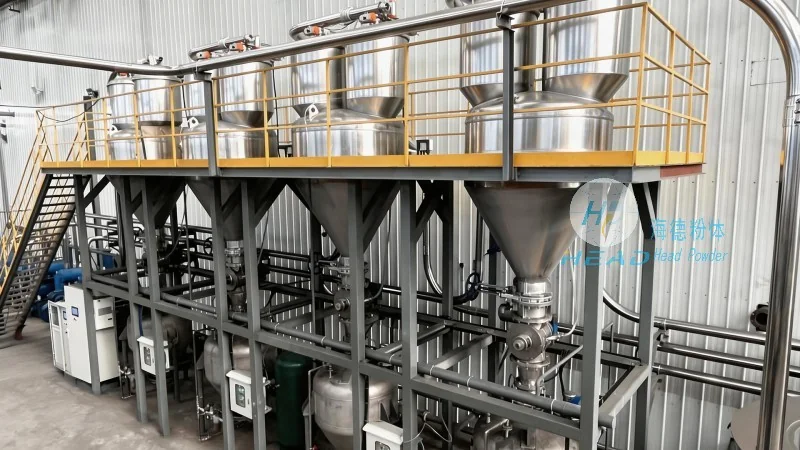
HeadPowder, a leading manufacturer based in Shandong, China, has developed a specialized enzyme pneumatic conveying system designed to address the challenges associated with traditional bioenzyme transportation. The system utilizes a combination of air pressure and vacuum to transport bioenzymes in a closed, sterile environment, ensuring minimal exposure to contaminants and maintaining the enzyme's activity throughout the process.
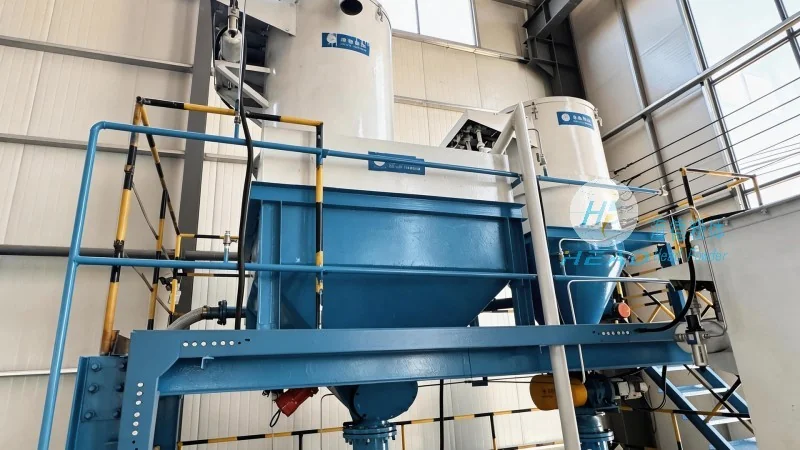
Key advantages of HeadPowder's enzyme pneumatic conveying include:
The enzyme pneumatic conveying system from HeadPowder has been successfully implemented in various bioenzyme production facilities. For instance, in a pharmaceutical plant producing therapeutic enzymes, the system was used to transport high-value enzymes from the production reactors to the purification and packaging stages. The result was a significant reduction in product loss due to contamination and a consistent improvement in enzyme activity, leading to higher product yields and better quality control.
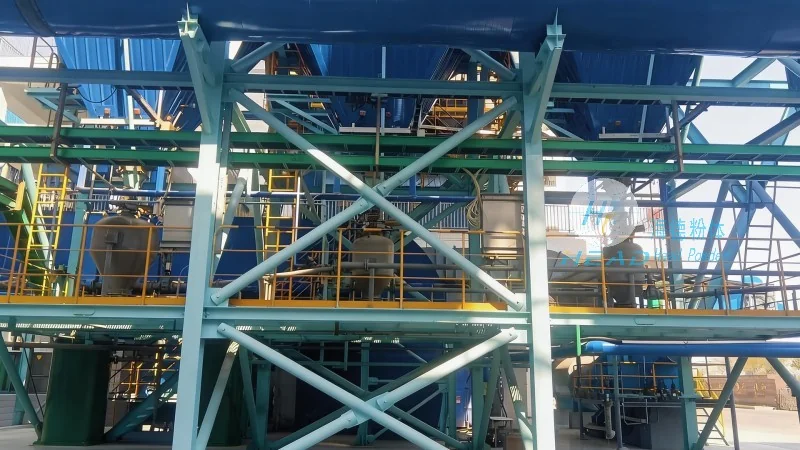
In another application, a food processing company utilized the system to transport food-grade enzymes used in baking and dairy production. The hygienic design of the system ensured compliance with food safety regulations, while the efficient transport process reduced labor costs and improved overall production throughput.
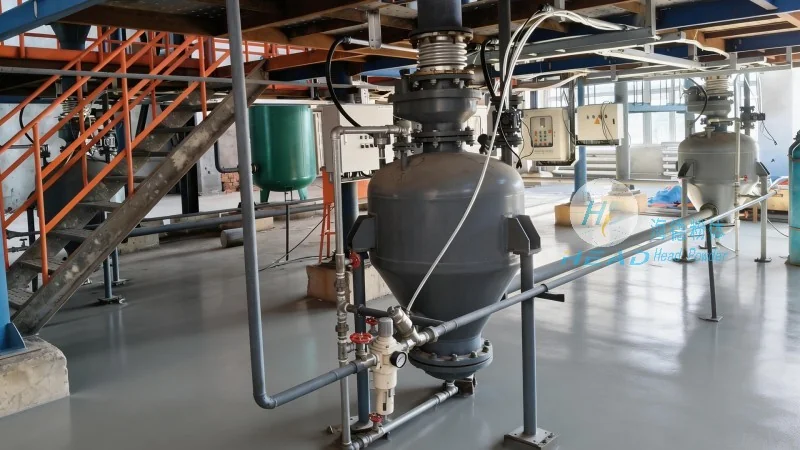
As the demand for bioenzymes continues to grow in industries such as biopharmaceuticals, food processing, and industrial biotechnology, the need for reliable and efficient transportation methods becomes increasingly important. HeadPowder's enzyme pneumatic conveying system offers a superior solution by combining advanced technology with a focus on maintaining the integrity of bioenzymes. With its hygienic operation, preservation of enzyme activity, and efficient design, the system provides significant benefits to manufacturers seeking to optimize their bioenzyme production processes.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to providing innovative solutions for bioenzyme transportation and processing. The company's expertise in pneumatic conveying technology, combined with a focus on customer needs, ensures that clients receive tailored solutions that meet their specific requirements. By choosing HeadPowder's enzyme pneumatic conveying system, manufacturers can enhance their operational efficiency, improve product quality, and stay competitive in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top