With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pumps, also known as pressure-type pneumatic conveyors, are specialized devices designed for the efficient and reliable transportation of bulk powders and granular materials. As a core product of Shandong HeadPowder Engineering Co., Ltd., these systems represent a significant advancement in material handling technology, offering solutions tailored to diverse industrial needs. The following sections will delve into the fundamental principles of bin pump operation and explore the key characteristics of their working environments.
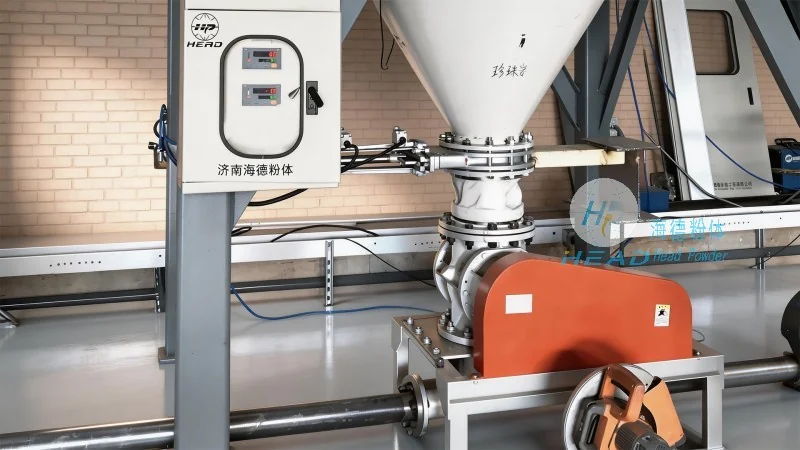
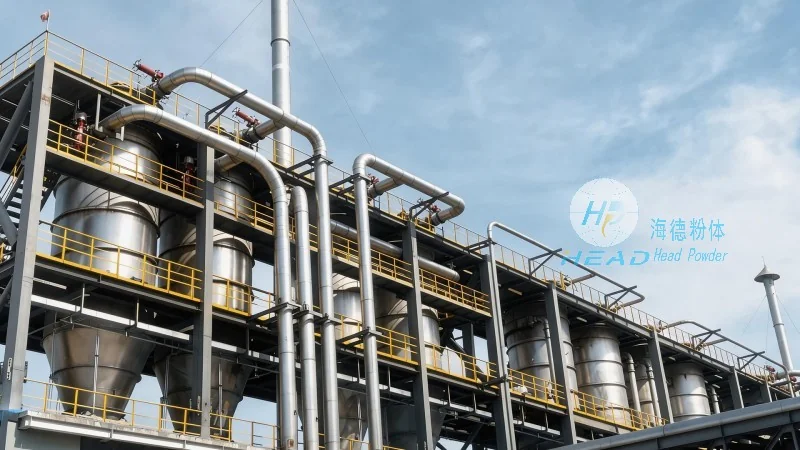
At the heart of bin pump technology lies a closed-loop system that utilizes compressed air to create a pressure differential, enabling the movement of powders from a storage bin to a destination point. The process typically begins with the material being fed from a hopper or silo into the pump chamber. As the chamber fills, a valve mechanism seals the inlet, and the pump then activates, drawing in compressed air from an external source. This air, combined with the powder, is then forced through a pipeline to the discharge point, where the air is released and the powder is deposited. The cycle repeats, with the pump continuously operating to maintain the flow of material. This principle ensures a consistent and controlled delivery of powders, minimizing material degradation and ensuring high efficiency.
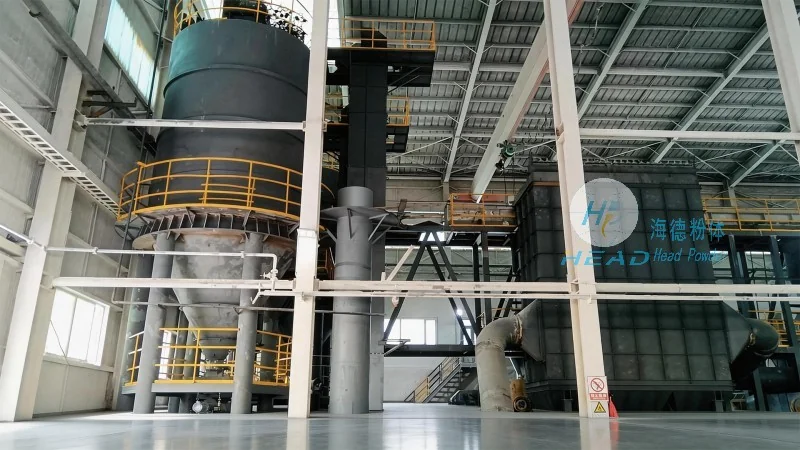
The application of bin pump systems is characterized by several distinct features that make them suitable for specific industrial scenarios. Firstly, their ability to handle a wide range of powder types, from fine powders to coarse granules, without clogging or degradation. This versatility is crucial in industries such as chemical processing, food production, and pharmaceutical manufacturing, where material quality is paramount. Secondly, the system's pressure-based operation allows for long-distance and high-rise transportation, making it ideal for facilities with complex layouts or multiple processing stages. Thirdly, the closed-loop design enhances safety by preventing dust emissions and ensuring that the material is contained throughout the transport process. Additionally, the compact and modular design of bin pumps facilitates easy integration into existing production lines, reducing installation time and costs. These characteristics collectively contribute to the widespread adoption of bin pump technology in modern industrial settings.
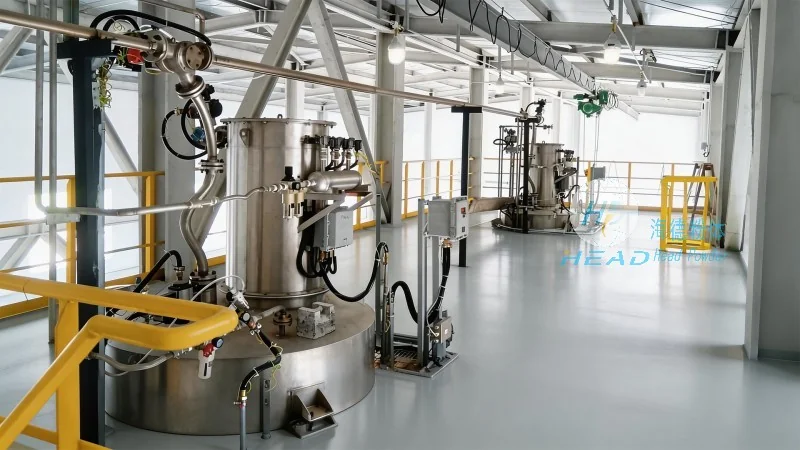
Bin pump powder handling equipment, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represents a robust and efficient solution for bulk material transportation. By leveraging the principles of pressure-driven pneumatic conveying, these systems provide reliable performance, adaptability, and safety, making them indispensable in various industrial applications. With a focus on innovation and quality, Shandong HeadPowder Engineering Co., Ltd. continues to advance the technology of bin pump systems, catering to the evolving needs of industries worldwide. The company's commitment to excellence ensures that its products meet the highest standards of performance and durability, supporting the operational efficiency of its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top