With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for handling calcined ash powders. With a focus on efficiency, reliability, and customization, our systems are engineered to meet the specific demands of industrial applications, ensuring optimal performance and minimal operational disruptions.
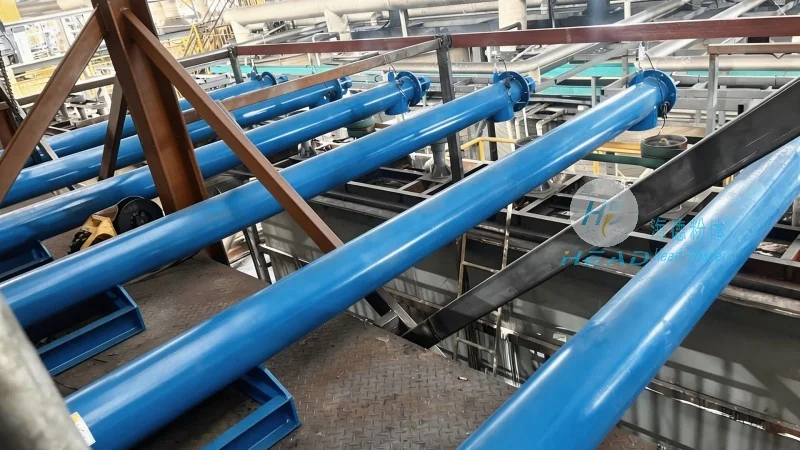
Calcined ash, a byproduct of coal combustion in power plants, is a fine powder that requires specialized handling due to its properties such as high temperature sensitivity, dustiness, and potential reactivity. Traditional methods like bucket elevators or belt conveyors may not be suitable for calcined ash due to the risk of material degradation, blockages, or contamination. Pneumatic conveying systems offer a solution by using air to transport the powder, providing a clean, enclosed, and efficient method of material transfer.
The core working principle of a calcined ash powder pneumatic conveying system involves the use of a compressor to generate high-pressure air, which is then directed through a pipeline network. The system typically consists of several key components: a material feeder, a conveying line, a control valve, and a dust collector or filter system. The material feeder, often a rotary valve or a screw feeder, introduces the calcined ash powder into the pipeline at a controlled rate. The high-pressure air then entrains the powder particles, creating a slurry-like mixture that is propelled through the pipeline to the destination point, such as a storage silo or processing unit.
During the conveying process, the air velocity within the pipeline is maintained above the minimum fluidization velocity of the calcined ash particles to prevent settling or blockages. The system may incorporate features like pulse-jet or rotary airlock valves to regulate the flow and ensure consistent material transport. At the receiving end, the air and powder mixture is separated using a cyclone or bag filter, where the air is discharged and the calcined ash is collected in a hopper or silo. This separation process is crucial for maintaining the purity of the material and ensuring the air is clean before release.
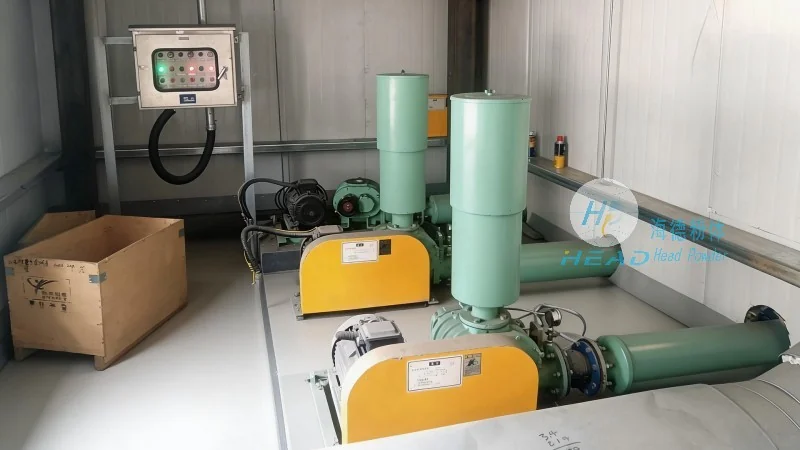
Calcined ash powder pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are designed with several distinctive features that enhance their performance and usability. One of the primary advantages is the enclosed and dust-free operation, which minimizes environmental contamination and ensures compliance with industrial safety and environmental regulations. The systems are also highly flexible, allowing for horizontal, vertical, or mixed-direction conveying, and can be configured to handle varying flow rates and material characteristics.
Another notable feature is the ability to handle abrasive and high-temperature materials without causing wear or damage to the system components. The use of high-quality materials, such as stainless steel or special alloys, ensures durability and long service life. Additionally, the systems are equipped with advanced control systems that allow for real-time monitoring of flow rates, pressure, and temperature, enabling operators to adjust the process parameters as needed to optimize performance and prevent equipment failure.
The systems also offer energy efficiency through optimized air flow management and the use of energy-saving compressors. By minimizing air leakage and ensuring efficient material transport, the systems reduce operational costs and environmental impact. Furthermore, the compact design of the conveying lines allows for easy integration into existing industrial facilities, reducing installation time and costs.
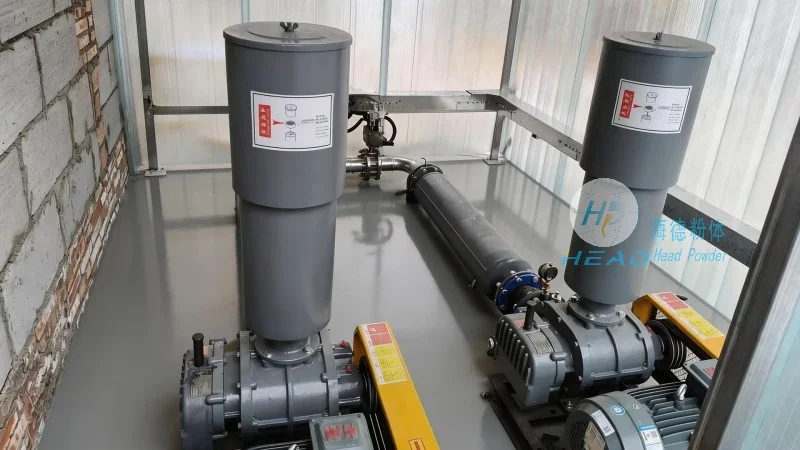
Shandong HeadPowder Engineering Co., Ltd. recognizes that each industrial application has unique requirements, and our pneumatic conveying systems are designed to be highly customizable. We offer a range of options, including different types of feeders, pipeline configurations, and control systems, to accommodate specific material properties, flow rates, and operational conditions. For example, systems can be configured to handle calcined ash with varying particle sizes, moisture content, or temperature levels, ensuring optimal performance in diverse applications.
Our team of engineers works closely with clients to understand their specific needs and develop tailored solutions. Whether for power plant ash handling, industrial waste processing, or other calcined ash applications, our systems are designed to meet the highest standards of efficiency, reliability, and safety. The integration of advanced technology and rigorous testing ensures that each system is optimized for the specific application, providing long-term performance and minimal maintenance requirements.
Pneumatic conveying systems for calcined ash powders represent a sophisticated and effective solution for material handling in industrial settings. With their enclosed operation, high efficiency, and flexibility, these systems offer significant advantages over traditional methods. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions that combine advanced technology, quality components, and expert engineering to deliver reliable and efficient calcined ash powder pneumatic conveying systems. By choosing our systems, industrial clients can enhance their operational efficiency, reduce costs, and ensure compliance with environmental and safety regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top