With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced material handling solutions. Our gravity dust removal material conveying systems are designed to efficiently transport and process bulk materials while effectively controlling dust emissions. This article explores the working principle and key features of our gravity dust removal material conveying system, highlighting its benefits and applications in various industrial sectors.
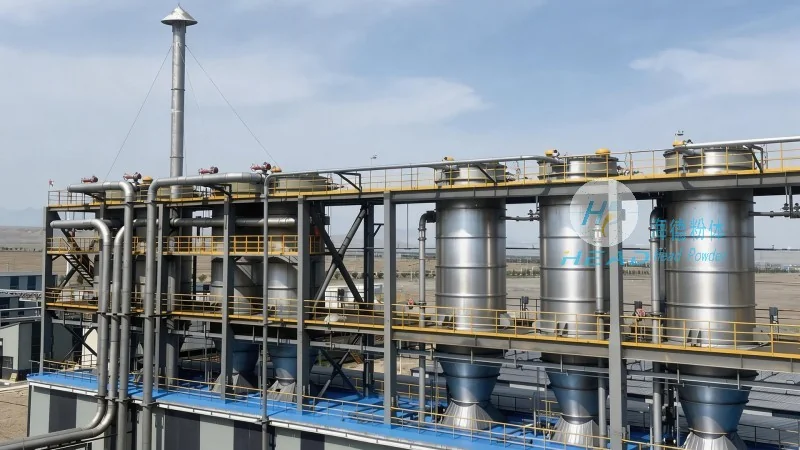
The gravity dust removal material conveying system operates on the principle of utilizing gravity and air flow to transport bulk materials while simultaneously removing dust particles. The system typically consists of a series of components, including a hopper, a conveyor belt or chute, a dust collection device, and a control system. When materials are fed into the hopper, they flow down the inclined conveyor due to gravity. As the material moves, air is drawn through the system, and the dust particles are separated from the bulk material by a filtration or cyclone mechanism. The clean material is then discharged at the end of the conveyor, while the collected dust is directed to a storage or disposal area. This process ensures that the material is conveyed efficiently with minimal dust generation, making it suitable for applications where air quality and material purity are critical.

Our gravity dust removal material conveying system is equipped with several advanced features that enhance its performance and reliability. Firstly, the system utilizes a gravity-driven design, which reduces the need for external power sources and minimizes energy consumption. This makes it an environmentally friendly and cost-effective solution for material handling. Secondly, the integrated dust removal mechanism effectively captures and filters dust particles, ensuring compliance with environmental regulations and maintaining a clean working environment. The system also features a robust construction with durable materials, such as stainless steel or high-quality plastics, to withstand harsh operating conditions and long-term use. Additionally, the modular design allows for easy installation and maintenance, reducing downtime and operational costs. The system is highly customizable to meet the specific requirements of different industries, including mining, cement, and chemical processing. It can handle a wide range of materials, from fine powders to bulk solids, with consistent performance and minimal maintenance.
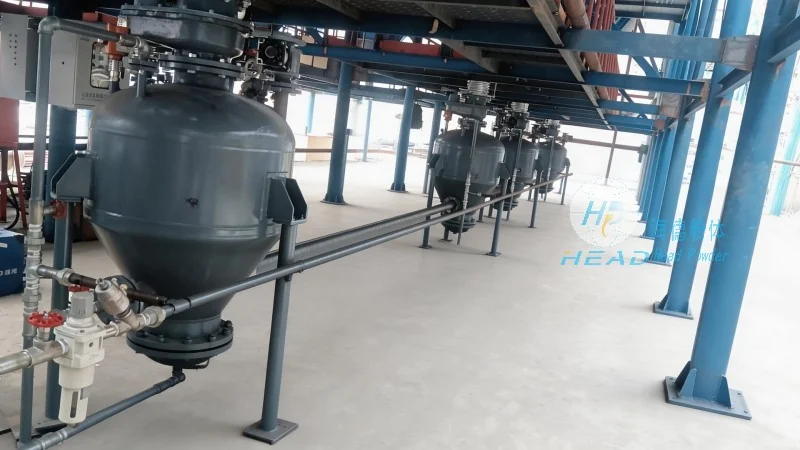
Adopting a gravity dust removal material conveying system offers numerous benefits for industrial operations. The primary advantage is the significant reduction in dust emissions, which improves air quality and protects the health and safety of workers. By controlling dust at the source, the system helps businesses comply with environmental regulations and avoid penalties. Additionally, the efficient material handling capabilities of the system increase productivity and reduce labor costs. The gravity-driven design minimizes energy consumption, leading to lower operational expenses and a smaller carbon footprint. The system's durability and low maintenance requirements also contribute to long-term cost savings. Furthermore, the clean material output ensures that downstream processes, such as packaging or processing, are not compromised by dust contamination, maintaining product quality and consistency. Overall, the gravity dust removal material conveying system is a reliable and efficient solution for industries seeking to optimize material handling while maintaining environmental standards.
Gravity dust removal material conveying systems are widely used in various industrial applications where bulk material handling and dust control are essential. In the mining industry, these systems are used to transport ore and other minerals from processing plants to storage or transport facilities, ensuring safe and efficient material movement. The cement industry utilizes gravity dust removal systems to convey raw materials and finished products, such as clinker and cement, while minimizing dust exposure. Chemical processing facilities also benefit from these systems when handling powders and granules, as they help maintain a clean and safe working environment. Additionally, the system is applicable in food processing, pharmaceuticals, and other industries where material purity and dust control are critical. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial plants.
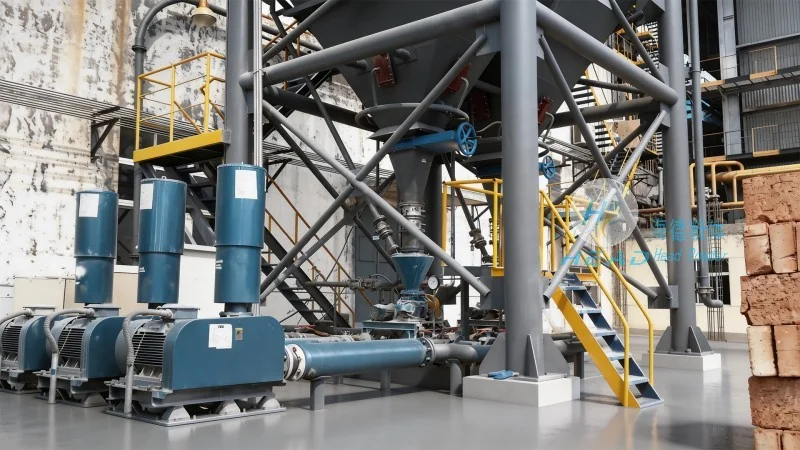
Shandong HeadPowder Engineering Co., Ltd. provides high-quality gravity dust removal material conveying systems that combine efficient material handling with effective dust control. The system's working principle, based on gravity and air flow, ensures reliable performance and minimal dust generation. Its key features, including energy efficiency, durability, and customization options, make it an ideal solution for various industrial applications. By implementing this system, businesses can enhance productivity, reduce operational costs, and comply with environmental regulations. With our expertise and commitment to quality, we offer reliable solutions that meet the diverse needs of our clients. Contact us today to learn more about how our gravity dust removal material conveying system can benefit your industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top