

Working Principle and Features of Industrial Salt Pneumatic Conveying Systems
Industrial salt pneumatic conveying systems are critical equipment in industries such as chemical processing and food manufacturing, designed to efficiently and safely transport bulk industrial salt. These systems utilize air as the primary medium to move salt particles through a network of pipes and components, offering a flexible and cost-effective solution for material handling. The core technology involves creating a controlled airflow that entrains the salt, allowing it to be transported from the source to the destination without direct physical contact. This method eliminates the need for mechanical components that can cause contamination or wear, making it ideal for applications where product purity and operational efficiency are paramount.
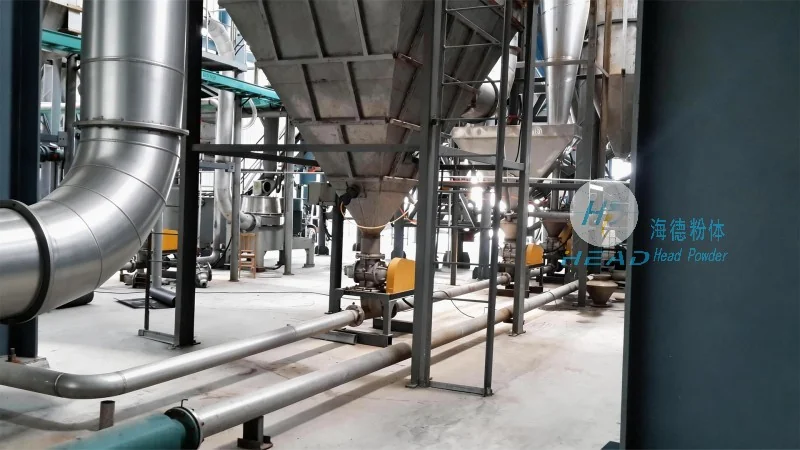
Working Principle of Industrial Salt Pneumatic Conveying Lines
The operation of an industrial salt pneumatic conveying line begins with the preparation of the salt material. The salt is typically stored in a hopper or silo, from which it is fed into a feeder that regulates the flow rate. The feeder then introduces the salt into the conveying line, where it is entrained by a stream of air generated by a fan or blower. The air velocity is carefully controlled to ensure that the salt particles are fully suspended and transported without settling or clogging the system. The conveying line includes straight sections, bends, and valves that guide the salt to the receiving end. At the destination, a separator—often a cyclone or bag filter—separates the salt from the air. The separated salt is collected in a storage bin or processing vessel, while the air is either filtered and recirculated or released into the environment. The entire process is automated, allowing for precise control of the conveying rate and ensuring consistent performance.
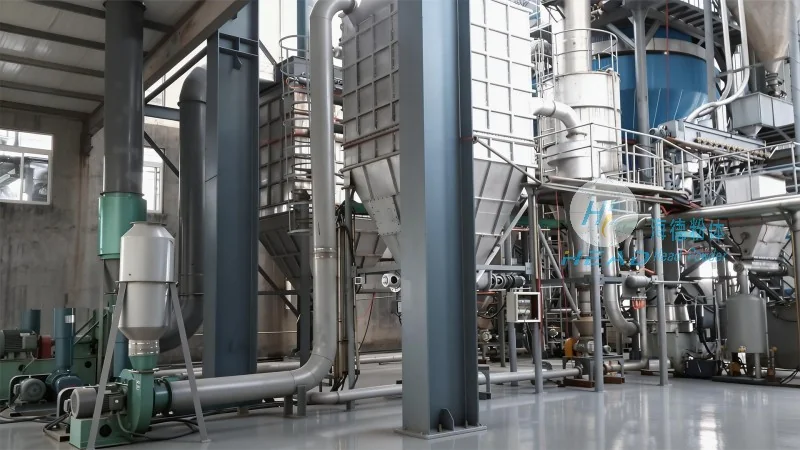
Key Features and Advantages of Industrial Salt Pneumatic Conveying Systems
Industrial salt pneumatic conveying systems offer several distinct advantages over traditional mechanical conveying methods. One of the most significant benefits is the ability to transport salt in a dust-free environment, which is crucial for maintaining product quality and ensuring workplace safety. Unlike belt or screw conveyors, which can generate dust and cause product contamination, pneumatic systems keep the material enclosed, reducing health hazards and improving product purity. Another advantage is the high flexibility in system layout. The conveying lines can be easily reconfigured or extended to accommodate changes in production processes or facility expansions, providing a cost-effective solution for evolving operational needs. The compact design of pneumatic equipment also saves valuable floor space, making it suitable for facilities with limited room for large machinery. Additionally, these systems can handle a wide range of salt types and particle sizes, from fine powders to coarse granules, without requiring major modifications. This versatility makes them adaptable to various applications, including food processing, where product safety is paramount.
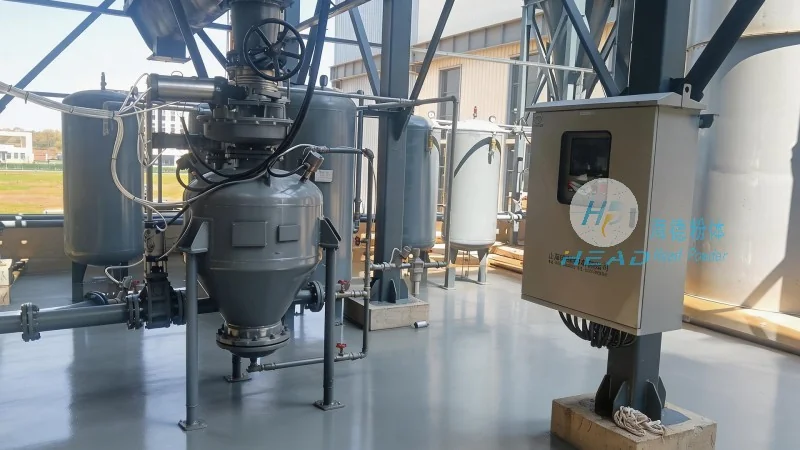
Technical Specifications and Customization Options
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized industrial salt pneumatic conveying systems tailored to the specific needs of each client. The company's engineers work closely with customers to understand their production requirements, material characteristics, and operational constraints, ensuring that the final system meets all performance and safety standards. Technical specifications for these systems typically include parameters such as airflow rate, pressure, conveying distance, and material throughput, which are determined based on the volume of salt to be transported and the distance between the source and destination. The conveying lines are constructed from high-quality materials, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions associated with industrial salt handling. Customization options may include the addition of features like dust collection systems, temperature control units, or automated feeding mechanisms to enhance system efficiency and reliability. By leveraging advanced technology and years of industry experience, Shandong HeadPowder Engineering Co., Ltd. ensures that each system is tailored to the unique needs of the client, providing long-term performance and minimal maintenance. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking reliable industrial salt handling solutions.