

What is a Tonne Bag Quantitative Feeding Powder Pneumatic Conveying Equipment? What are its Design P
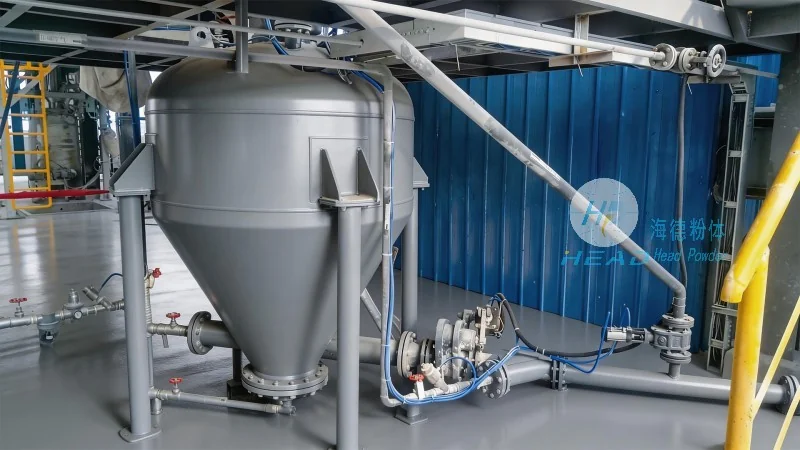
When it comes to efficient and reliable powder handling in industrial applications, the Tonne Bag Quantitative Feeding Pneumatic Conveying Equipment stands out as a sophisticated solution. This equipment is specifically designed to handle bulk powders with precision, ensuring consistent and controlled feeding rates. The system integrates seamlessly with tonne bags, which are widely used for storing and transporting large quantities of powders, making it an ideal choice for industries such as pharmaceuticals, food processing, and chemical manufacturing.
Understanding the Core Functionality of the Equipment
The primary function of this equipment is to provide a quantitative feeding mechanism for powders from tonne bags. By utilizing pneumatic conveying technology, the system draws powder from the bag and transports it to the processing line or storage area. The quantitative feeding feature ensures that the exact amount of powder is delivered as required, minimizing waste and optimizing production efficiency. This is particularly crucial in industries where precise dosage is essential, such as in pharmaceuticals, where accurate dosing can impact product quality and safety.
Design Principles Behind the Pneumatic Conveying System
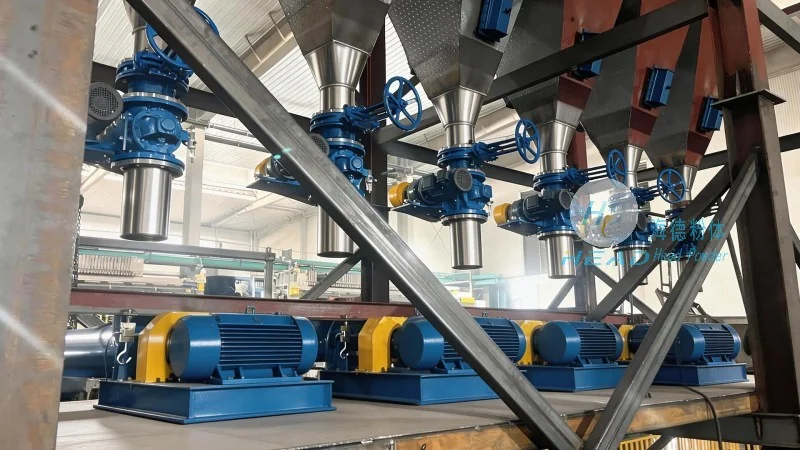
The design of the Tonne Bag Quantitative Feeding Pneumatic Conveying Equipment is based on fundamental principles of fluidization and air movement. The system operates by creating a low-pressure zone that draws air and powder particles into the conveying line. The powder is then suspended in the air stream and transported through the pipeline to the discharge point. The quantitative feeding mechanism is achieved through a combination of control valves, flow meters, and a hopper that regulates the flow rate. The design ensures that the powder is conveyed without caking or segregation, maintaining the integrity of the material throughout the process.
Key Components and Their Roles
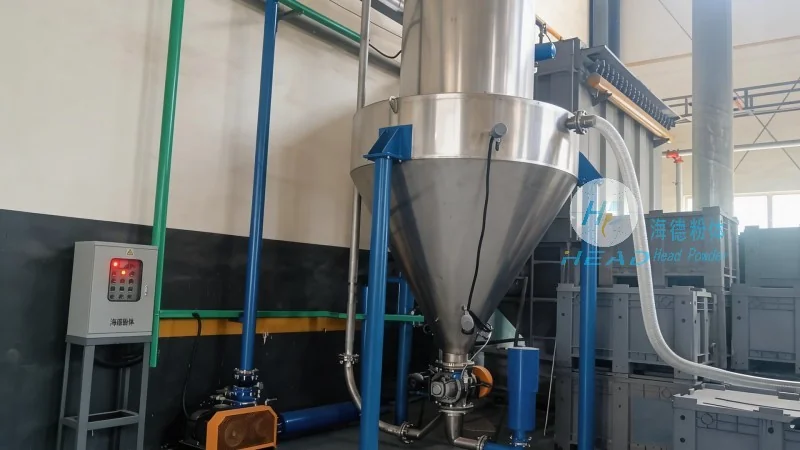
Several key components work together to ensure the smooth operation of the Tonne Bag Quantitative Feeding Pneumatic Conveying Equipment. The tonne bag itself serves as the primary storage container, with a discharge valve at the bottom that allows controlled release of the powder. The feeder unit, often a rotary valve or a screw feeder, regulates the flow of powder from the bag into the conveying line. The air compressor provides the necessary air pressure to drive the conveying process, while the filter and cyclone separator ensure that the air is clean and that any fine particles are removed from the system. The control panel allows operators to adjust the feeding rate and monitor the system's performance in real-time.
Benefits and Applications
The Tonne Bag Quantitative Feeding Pneumatic Conveying Equipment offers numerous benefits to industrial operations. Its ability to handle large quantities of powders efficiently reduces labor costs and improves productivity. The quantitative feeding feature minimizes material waste and ensures consistent product quality, which is critical in industries where batch-to-batch consistency is required. Additionally, the pneumatic conveying system is flexible and can be integrated with existing processing lines, making it a cost-effective solution for upgrading or expanding powder handling capabilities. The equipment is widely used in pharmaceutical manufacturing for handling active pharmaceutical ingredients (APIs), in food processing for handling ingredients like flour and sugar, and in chemical manufacturing for handling various powders and granules.
About HeadPowder: The Manufacturer
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of advanced powder handling equipment. With its headquarters in Shandong, China, the company specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's commitment to innovation and quality has made it a trusted partner for businesses seeking reliable and efficient powder handling solutions. The company's products are known for their durability, precision, and ease of maintenance, ensuring long-term performance and customer satisfaction.