

What is a Cobalt Hydroxide Material Handling System Equipment? And What Are Its Design Principles?
The cobalt hydroxide material handling system is a specialized piece of equipment designed for the efficient transportation and processing of cobalt hydroxide, a critical component in various industrial applications. This system plays a vital role in ensuring the smooth flow of material from production to processing stages, optimizing operational efficiency and safety. Understanding the design principles behind such systems is essential for industries relying on cobalt hydroxide, as it directly impacts performance and reliability.
Key Components of the Cobalt Hydroxide Material Handling System
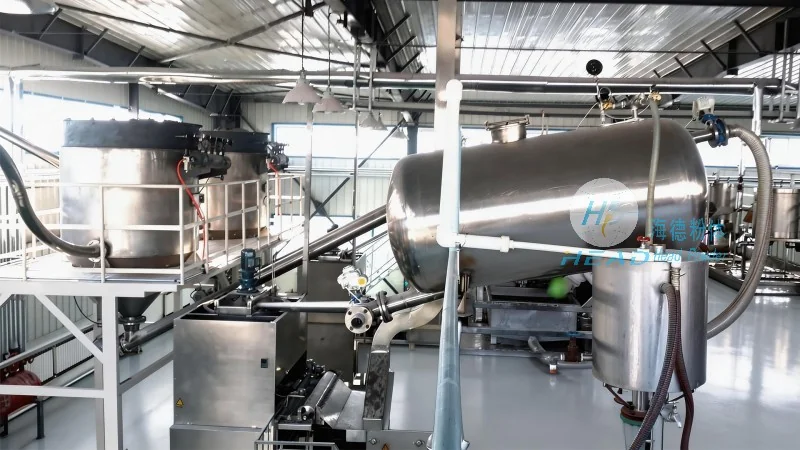
The system typically comprises several key components that work in tandem to facilitate material movement. These include conveyor belts, hoppers, feeders, and control mechanisms. The conveyor belts are engineered to handle the specific properties of cobalt hydroxide, such as its particle size and moisture content, ensuring minimal material degradation during transport. Hoppers are used to store and feed the material into the system, while feeders regulate the flow rate to maintain consistent processing. Control mechanisms, often integrated with sensors, monitor the system's performance and adjust parameters as needed to prevent blockages or overloading.
Design Principles for Optimal Performance
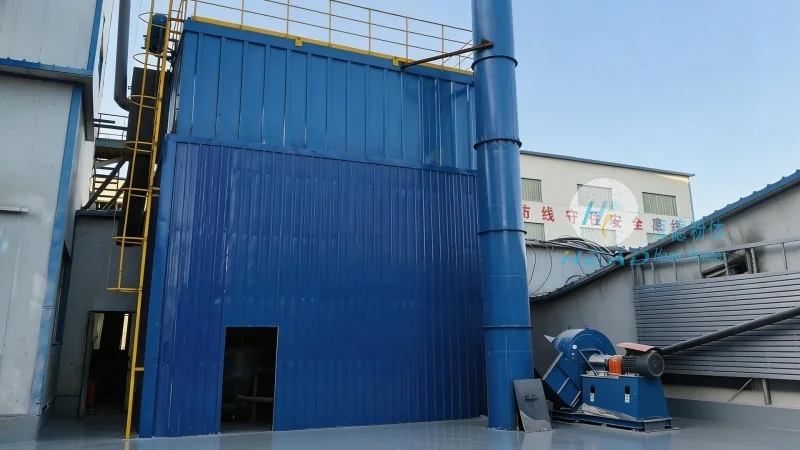
The design of a cobalt hydroxide material handling system is guided by several key principles aimed at maximizing efficiency and safety. First, the system must be designed to handle the material's physical properties, including its density, abrasiveness, and tendency to stick or clump. This involves selecting appropriate materials for the conveyor components, such as high-strength belts and wear-resistant rollers, to minimize wear and tear. Second, the system must prioritize safety, incorporating features like emergency stop buttons, overload protection, and proper ventilation to prevent dust accumulation and ensure operator safety. Third, the design must consider scalability and adaptability, allowing for adjustments to accommodate varying production volumes or changes in material characteristics. Finally, energy efficiency is a critical factor, with the system designed to minimize power consumption while maintaining optimal performance.
Operational Benefits of the Material Handling System
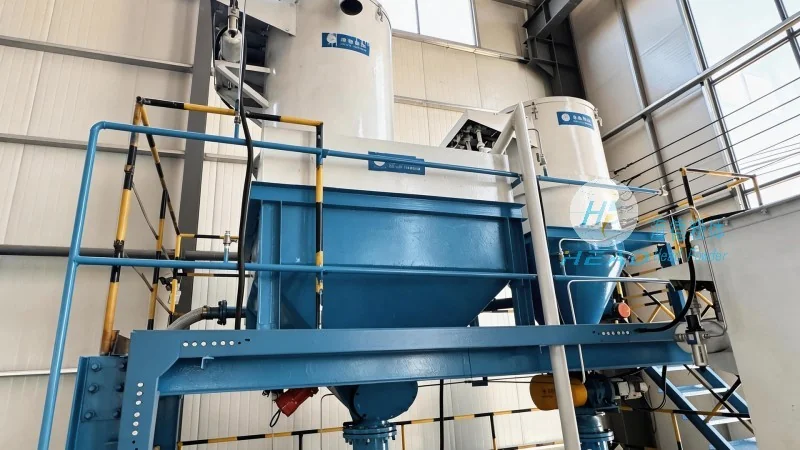
Implementing a cobalt hydroxide material handling system offers numerous operational benefits for industrial facilities. The primary advantage is the significant improvement in material flow efficiency, reducing downtime and increasing throughput. By automating the material transport process, the system minimizes the need for manual handling, which not only speeds up operations but also reduces the risk of accidents and material contamination. Additionally, the system enhances process consistency, ensuring that the material is delivered to the next stage of processing in a uniform manner, which is crucial for maintaining product quality. The integration of sensors and control systems also enables real-time monitoring and data collection, allowing for proactive maintenance and optimization of the system's performance.
Customization and Integration with Existing Facilities
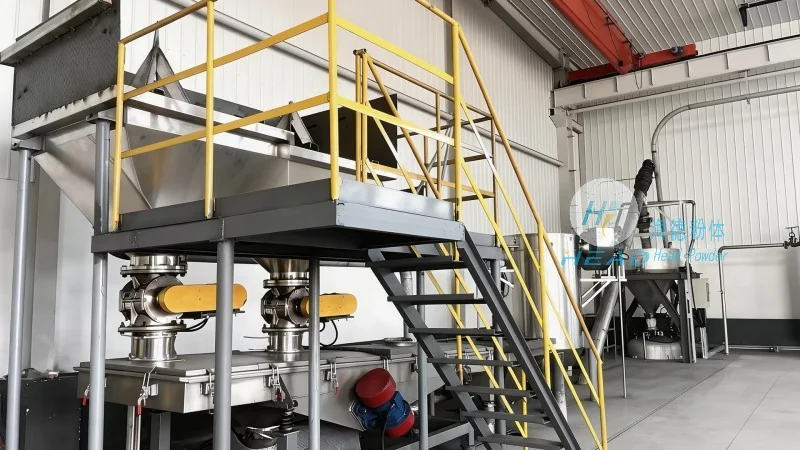
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized cobalt hydroxide material handling systems tailored to the specific needs of each client. The company's approach involves a thorough analysis of the client's production processes, material characteristics, and operational requirements to develop a system that meets their unique needs. The systems are designed to integrate seamlessly with existing facilities, minimizing disruption during installation and ensuring a smooth transition to the new equipment. Customization options include different conveyor lengths, widths, and speeds, as well as the addition of specialized components such as magnetic separators or drying units, depending on the client's specific requirements. The company's team of engineers works closely with clients to ensure that the final system is not only efficient but also cost-effective and easy to maintain.