

What is Corn Cob Material Handling Equipment? And What Are Its Design Principles?
Welcome to the world of corn cob material handling equipment, a specialized field that addresses the unique challenges of transporting and processing corn cob materials. As a leading manufacturer in this industry, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying high-efficiency solutions tailored to the demands of corn processing facilities. This article explores the fundamental aspects of corn cob material handling equipment, including its design principles and operational capabilities.
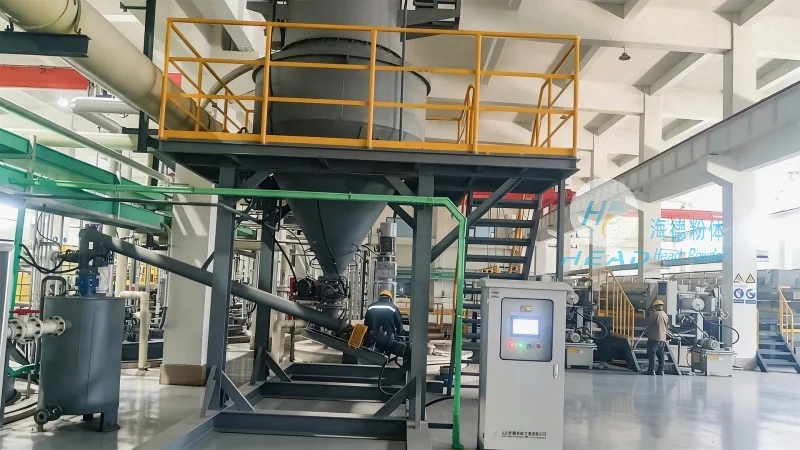
Introduction to Corn Cob Material Handling Equipment
Corn cob material handling equipment is a critical component in the corn processing industry, designed to efficiently transport, store, and process corn cobs from the field to the processing plant. These systems are engineered to handle the bulk, irregular shape, and varying moisture content of corn cobs, ensuring smooth and continuous operation. The equipment plays a pivotal role in optimizing the workflow, reducing labor costs, and enhancing overall productivity in corn processing operations.
Overview of Corn Cob Material Handling Equipment
At the core of corn cob material handling equipment are several key systems, including conveyors, elevators, and storage silos. Conveyors, such as belt conveyors or chain conveyors, are commonly used to transport corn cobs horizontally or at slight inclines. Elevators, particularly bucket elevators or screw conveyors, are employed to lift corn cobs vertically or over longer distances. Storage silos are integrated to temporarily hold corn cobs before further processing or drying. The selection of equipment depends on the specific requirements of the processing plant, including the volume of corn cobs, the available space, and the desired throughput rate.
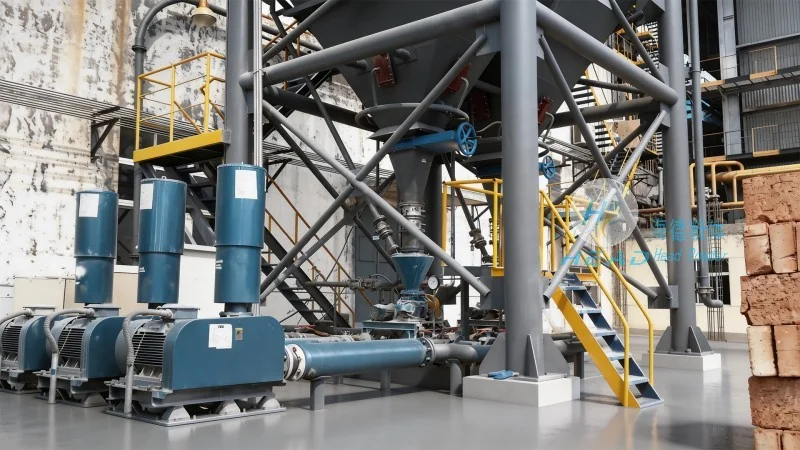
Design Principles of Corn Cob Material Handling Equipment
The design of corn cob material handling equipment is guided by several fundamental principles aimed at maximizing efficiency, durability, and safety. First, the equipment must be robust enough to withstand the abrasive nature of corn cobs, which can cause wear and tear on components over time. This is achieved through the use of high-quality materials, such as stainless steel or reinforced plastic, in the construction of conveyor belts, buckets, and housing. Second, the design prioritizes minimal friction and resistance to ensure smooth and energy-efficient operation. This involves optimizing the shape of the conveyor components and using lubrication systems where appropriate. Third, the equipment is designed for easy maintenance and cleaning, as corn cobs can accumulate in hard-to-reach areas and may require regular cleaning to prevent blockages. Access panels and removable components are often included to facilitate maintenance tasks.
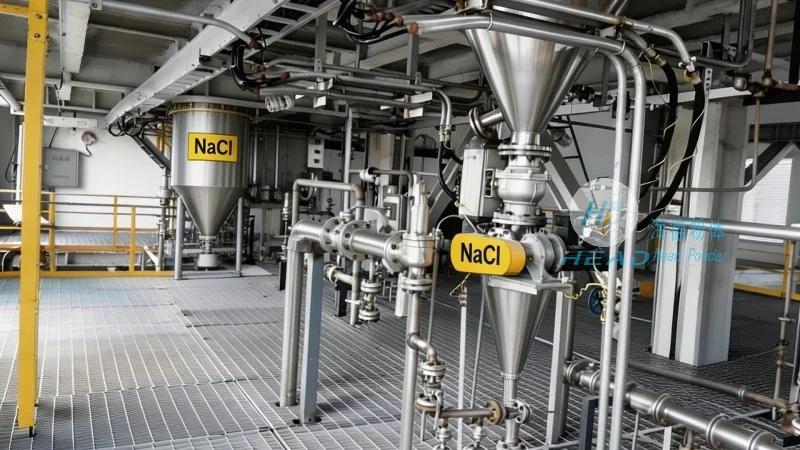
Key Components and Functional Aspects
Several key components contribute to the functionality of corn cob material handling equipment. The feed hopper is the entry point for corn cobs, designed to evenly distribute the material onto the conveyor system. The conveyor system itself, whether belt or chain-driven, is responsible for moving the corn cobs along the intended path. The drive mechanism, typically powered by electric motors, provides the necessary force to move the material. The discharge mechanism, such as a chute or spout, directs the corn cobs to the next stage of processing. Additionally, safety features, such as emergency stop buttons and protective guards, are integrated to prevent accidents and ensure operator safety. The design also considers the need for dust control, as corn cobs can generate significant dust during handling, which may require dust collection systems to maintain a safe working environment.
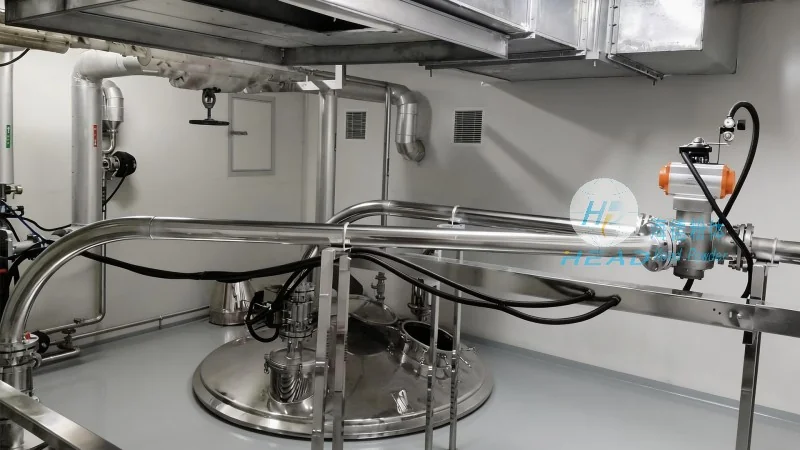
Application Scenarios and Operational Benefits
Corn cob material handling equipment is widely used in various stages of corn processing, from harvesting to drying and storage. In the harvesting stage, equipment is used to collect corn cobs from the field and transport them to the processing plant. During processing, the equipment helps move corn cobs through cleaning, drying, and grinding stages. In storage facilities, the equipment is used to transfer corn cobs from storage silos to processing lines as needed. The operational benefits of using specialized corn cob material handling equipment include increased throughput, reduced labor costs, and improved product quality. By ensuring consistent and efficient material flow, the equipment minimizes downtime and maximizes the overall efficiency of the corn processing operation. Additionally, the equipment helps maintain a clean and organized workspace, reducing the risk of contamination and improving safety standards.
About the Manufacturer: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of corn cob material handling equipment, with a strong presence in the Chinese market and a growing reputation internationally. The company is headquartered in Shandong, China, and specializes in developing customized solutions for the corn processing industry. With years of experience and a team of skilled engineers, Shandong HeadPowder Engineering Co., Ltd. has become a trusted partner for many corn processing facilities worldwide. The company's commitment to quality, innovation, and customer satisfaction has earned it a reputation for producing reliable and efficient equipment that meets the unique needs of its clients. Whether for new construction or retrofitting existing facilities, Shandong HeadPowder Engineering Co., Ltd. offers a range of solutions that enhance the performance and productivity of corn processing operations.