With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling white bean pellets, selecting the appropriate pneumatic conveying manufacturer is a critical decision that impacts operational efficiency, product quality, and overall cost-effectiveness. The choice of manufacturer directly influences how effectively your white bean pellets are transported, processed, and stored, making it essential to evaluate various factors before making a decision. This guide outlines key considerations to help you choose the right manufacturer for your specific needs.
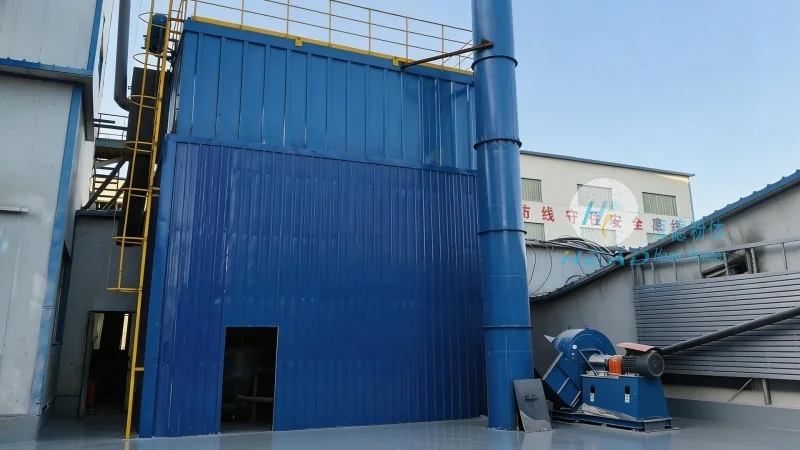
Several critical factors should be considered when selecting a manufacturer for white bean pellet pneumatic conveying systems. First, assess the manufacturer's experience and expertise in handling similar products. A company with a proven track record in processing and conveying white bean pellets will likely offer more reliable solutions tailored to your requirements. Additionally, consider the manufacturer's technical capabilities, including their ability to design customized systems that meet your specific operational parameters, such as material flow rates, pressure requirements, and space constraints.
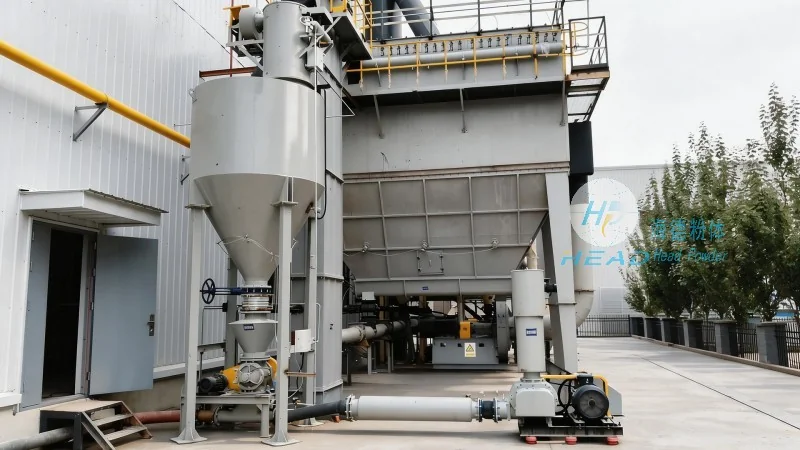
For white bean pellet pneumatic conveying, specific technical specifications are vital. The manufacturer should be able to provide detailed information on system components, such as the type of air movers (e.g., rotary lobe blowers, centrifugal fans), material handling equipment (e.g., hoppers, cyclones), and control systems. A robust design that ensures minimal product degradation, dust control, and energy efficiency is crucial. Moreover, the manufacturer should offer solutions that comply with industry standards and regulations, particularly concerning food safety and environmental impact. This includes features like dust collection systems and material handling equipment that prevent contamination and maintain product integrity.
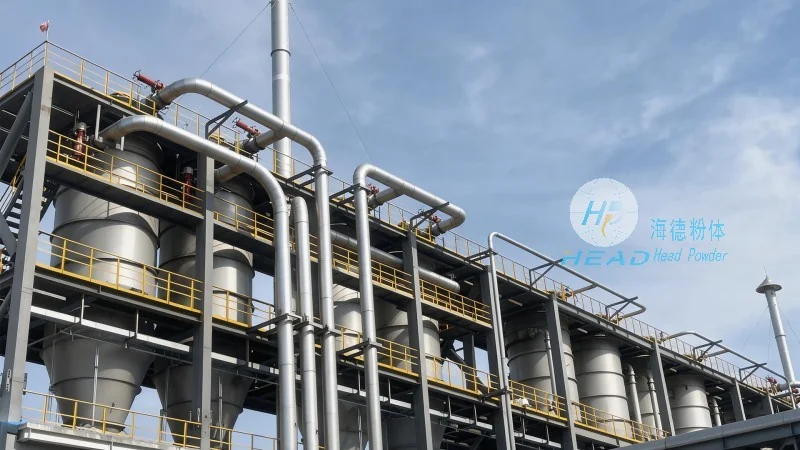
Every white bean pellet processing operation has unique requirements. A reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) specializes in customizing pneumatic conveying systems to meet specific needs. This includes designing systems that optimize material flow, reduce downtime, and enhance overall productivity. After-sales support is equally important. The manufacturer should provide comprehensive support, including installation, training, and ongoing maintenance services. This ensures that your system operates efficiently and any issues are addressed promptly, minimizing disruptions to your production process.
Choosing a manufacturer with a strong commitment to quality assurance is essential. Look for certifications such as ISO standards, which indicate adherence to international quality and safety benchmarks. A reliable manufacturer will also offer warranties on their equipment and provide transparent information about their manufacturing processes and material sourcing. This ensures that the components used in your pneumatic conveying system are durable, efficient, and suitable for handling white bean pellets without compromising performance or product quality.

While cost is a significant factor, it should not be the sole determinant when selecting a pneumatic conveying manufacturer. It is crucial to evaluate the total cost of ownership, including initial investment, operational costs, and maintenance expenses. A high-quality system from a reputable manufacturer like headpowder may have a higher upfront cost but offers long-term benefits such as lower energy consumption, reduced maintenance needs, and extended equipment lifespan. This results in better overall cost-effectiveness and a higher return on investment over time.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top