With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Comprehensive engineering solutions for mineral particle pneumatic conveying represent a sophisticated approach to material handling in industrial applications. This specialized field focuses on the efficient and reliable transport of bulk solid materials through a gas stream, typically air or other gases. The technology is widely utilized across various industries, including mining, chemical processing, and food processing, where the need to move large volumes of mineral particles safely and effectively is paramount.
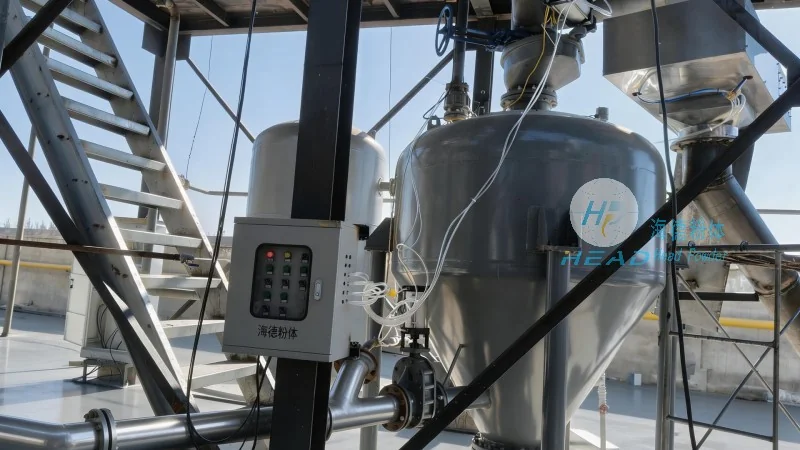
The core of a mineral particle pneumatic conveying system consists of several critical components that work in concert to ensure optimal performance. These components include the material feed hopper, which holds the bulk solid, and the conveying line where the particles are propelled by the gas flow. The system may also incorporate a blower or compressor to generate the necessary air pressure, a filter to capture any particulate matter, and a discharge unit to deliver the material to its final destination. The design of these systems is tailored to the specific characteristics of the mineral particles, such as size, density, and moisture content, as well as the operational requirements of the facility.
Compared to traditional mechanical conveying methods like belt conveyors or screw conveyors, pneumatic conveying offers several distinct advantages. One of the most significant benefits is the ability to transport materials over long distances with minimal maintenance. The enclosed system also prevents dust contamination, which is crucial for maintaining a clean and safe working environment, especially in industries where dust can be hazardous or affect product quality. Additionally, pneumatic conveying systems can handle a wide range of particle sizes and shapes, making them versatile for diverse applications. The flexibility of these systems allows for easy integration into existing production lines and the ability to adapt to changing operational needs.
In the mining sector, pneumatic conveying systems are essential for transporting ore from mines to processing facilities. The ability to handle large volumes of mineral particles efficiently reduces downtime and improves overall productivity. For example, in coal mining operations, pneumatic conveyors can transport coal from the mine face to storage or processing plants with high reliability. Similarly, in mineral processing plants, these systems are used to move raw materials like limestone, sand, or gravel through various stages of production, ensuring a continuous flow of material without the need for manual handling.
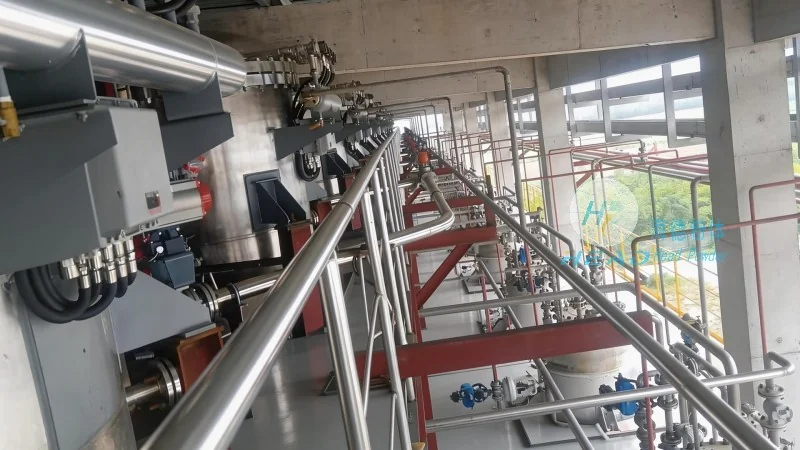
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of comprehensive mineral particle pneumatic conveying systems. With a strong focus on engineering excellence and customer satisfaction, the company has established itself as a leading provider in the industry. The company's team of experienced engineers and technicians brings extensive knowledge in material handling technologies, ensuring that each project is tailored to meet the unique needs of the client. HeadPowder's commitment to quality and innovation is reflected in its state-of-the-art facilities and adherence to international standards in design and construction.
HeadPowder understands that every industrial application has distinct requirements, and therefore, offers customized pneumatic conveying solutions. Whether the client needs a system for short-distance transport within a plant or a long-distance pipeline for interplant material transfer, the company provides tailored designs that optimize performance and cost-effectiveness. The engineering team works closely with clients to assess their specific material characteristics, operational parameters, and budget constraints to develop a system that meets all requirements. This collaborative approach ensures that the final solution is not only efficient but also sustainable and scalable for future growth.
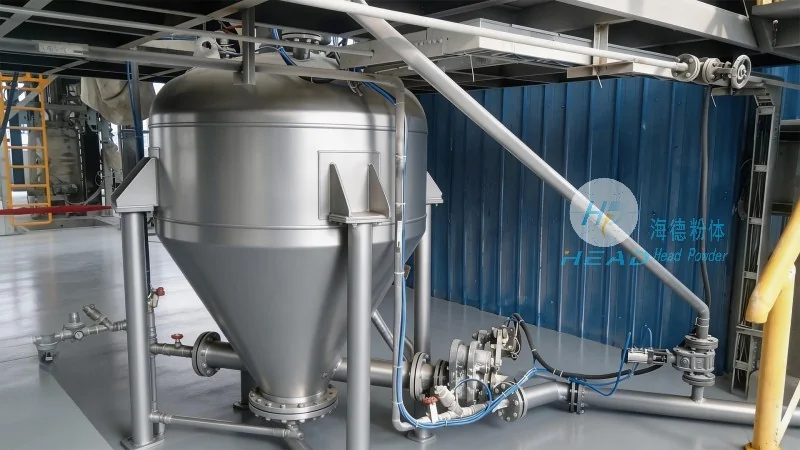
Reliability is a key factor in the success of any pneumatic conveying system, and HeadPowder places a strong emphasis on building systems that are durable and require minimal maintenance. The use of high-quality materials and components, such as corrosion-resistant metals and efficient blower systems, contributes to the longevity of the equipment. Regular maintenance, including filter cleaning and component inspections, is recommended to ensure optimal performance and prevent downtime. HeadPowder also provides comprehensive after-sales support, including technical assistance and spare parts availability, to help clients maintain their systems in top condition.
HeadPowder's pneumatic conveying systems are designed with environmental and safety considerations at the forefront. The enclosed nature of the system minimizes dust emissions, which helps in complying with environmental regulations and maintaining a safe working environment. The company adheres to strict safety standards, ensuring that all equipment is installed and operated in accordance with local and international safety guidelines. This commitment to safety and environmental responsibility aligns with the growing demand for sustainable industrial practices and contributes to the long-term success of the clients' operations.
Comprehensive engineering for mineral particle pneumatic conveying, as provided by Shandong HeadPowder Engineering Co., Ltd., represents a cutting-edge solution for efficient material handling in various industrial sectors. By combining advanced technology with expert engineering, the company delivers systems that enhance productivity, ensure safety, and meet the evolving needs of modern industry. With a strong reputation for quality and reliability, HeadPowder continues to be a trusted partner for businesses seeking to optimize their material transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top