With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk agricultural products like barley, efficient and reliable transportation methods are crucial to maintaining product quality and operational efficiency. Among the various technologies available, pneumatic conveying stands out as a versatile solution for handling barley in bulk, offering advantages that traditional methods may not provide.
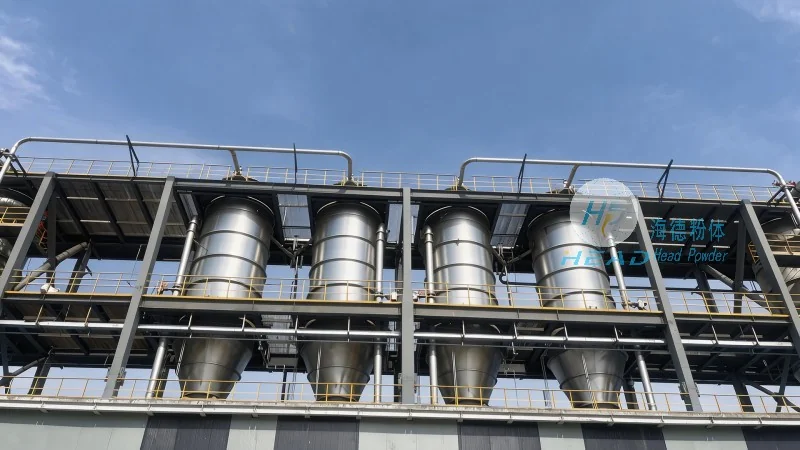
Pneumatic conveying systems utilize air to transport barley particles through a pipeline network. This method is particularly effective for barley due to its ability to handle a wide range of particle sizes and moisture contents without causing damage to the grain. The system operates by creating a pressure differential that moves the barley from the source to the destination, ensuring a continuous and controlled flow. Compared to mechanical conveying systems, pneumatic conveyors reduce the risk of contamination and minimize the need for manual handling, which is essential for maintaining the purity and quality of barley used in food, feed, and brewing industries.
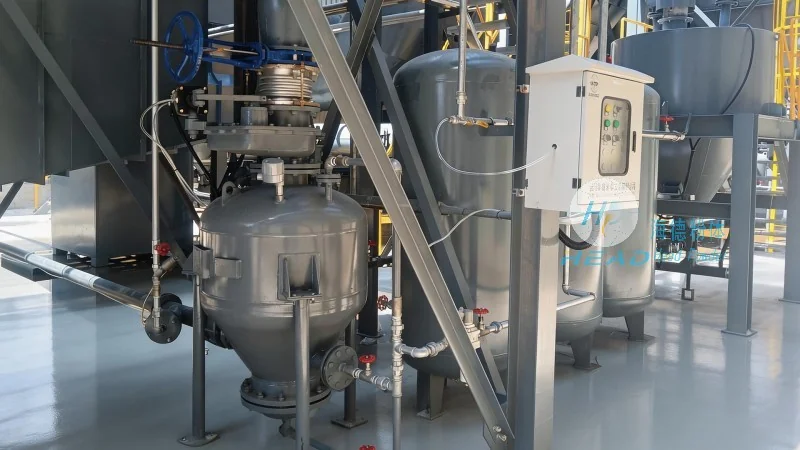
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of barley handling operations. The company’s expertise lies in creating customized systems that optimize the transportation process while ensuring compliance with industry standards. Key features of their pneumatic conveying solutions include:
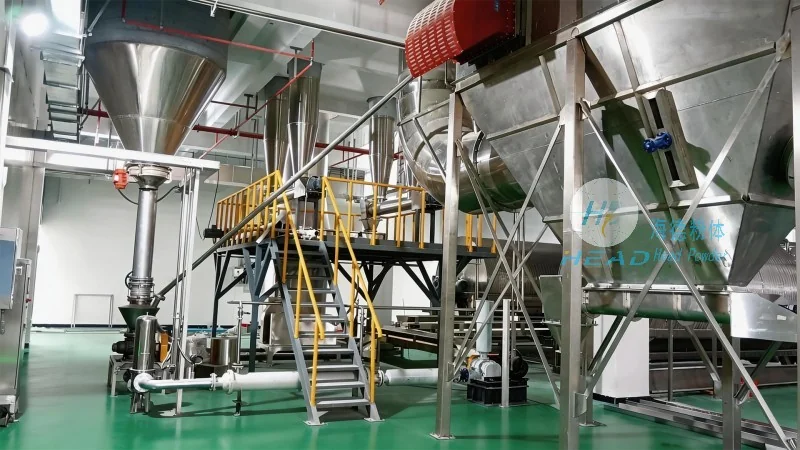
The application of pneumatic conveying in barley handling spans various stages of the supply chain, from storage and processing to distribution. For instance, in grain elevators and storage facilities, pneumatic conveyors are used to move barley from silos to processing lines, ensuring a smooth transition from storage to production. During the brewing process, pneumatic systems are employed to transport barley to mashing tanks, where it is mixed with water to initiate the fermentation process. In feed mills, the technology is used to convey barley to mixing equipment, ensuring uniform distribution of the grain in animal feed formulations.
By implementing pneumatic conveying systems, barley producers and processors can achieve significant benefits, including improved operational efficiency, reduced labor costs, and enhanced product quality. The continuous flow of barley reduces downtime and increases production throughput, while the controlled environment minimizes the risk of spoilage and contamination. Additionally, the system’s ability to handle different barley varieties and processing requirements makes it a versatile solution for diverse applications.
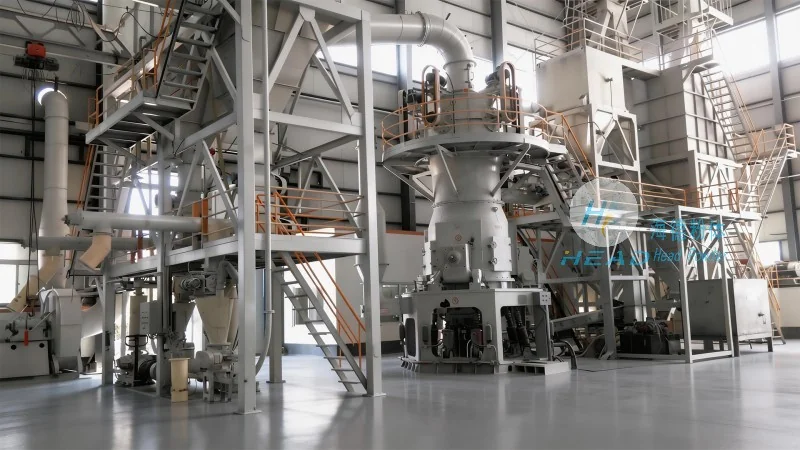
As a trusted partner in bulk material handling, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide advanced pneumatic conveying solutions for the barley industry. With a focus on quality, efficiency, and customer satisfaction, the company’s systems are designed to meet the evolving needs of barley producers and processors, ensuring reliable and sustainable transportation of barley in bulk. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise to deliver tailored solutions that enhance the performance and profitability of barley handling operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top