With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring efficient and reliable transport of pulverized coal, various pneumatic conveying systems have been developed to meet diverse operational needs. These solutions are designed to optimize material handling, reduce operational costs, and enhance overall system performance. This article explores several key approaches to pulvarized coal pneumatic conveying, highlighting the technical aspects and practical considerations for each method.
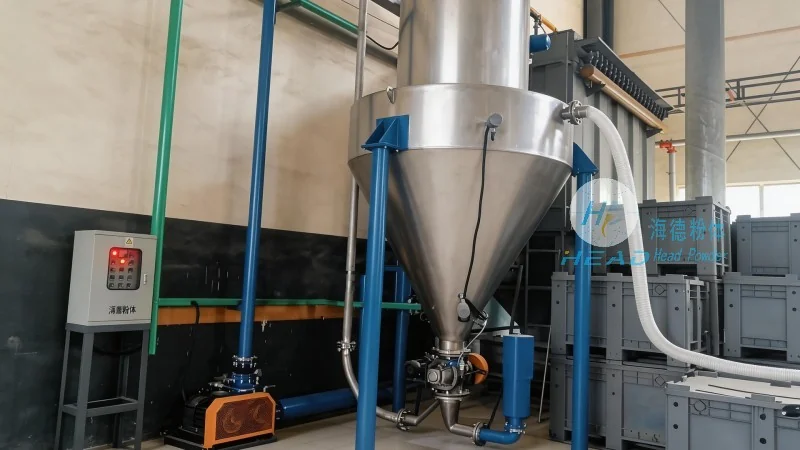
Dilute phase systems are widely used for long-distance and high-capacity coal transport. In this method, coal particles are suspended in a high-velocity air stream, allowing for efficient movement through pipelines. The system typically operates at pressures ranging from low to moderate, making it suitable for applications where energy efficiency and cost-effectiveness are critical. The design of dilute phase conveyors involves careful consideration of air velocity, particle size distribution, and pipeline dimensions to ensure optimal performance and minimize wear on components.
Dense phase conveying offers a more controlled and gentle transport method, particularly beneficial for handling sensitive coal types or when lower air velocities are required. This approach involves operating the system at higher pressures and lower air velocities, which results in a higher concentration of coal particles in the air stream. The result is a slower, more stable flow that reduces the risk of particle degradation and equipment damage. Dense phase systems are often preferred in applications where product quality and equipment longevity are paramount, such as in the transportation of high-value coal or in systems with limited pipeline length.
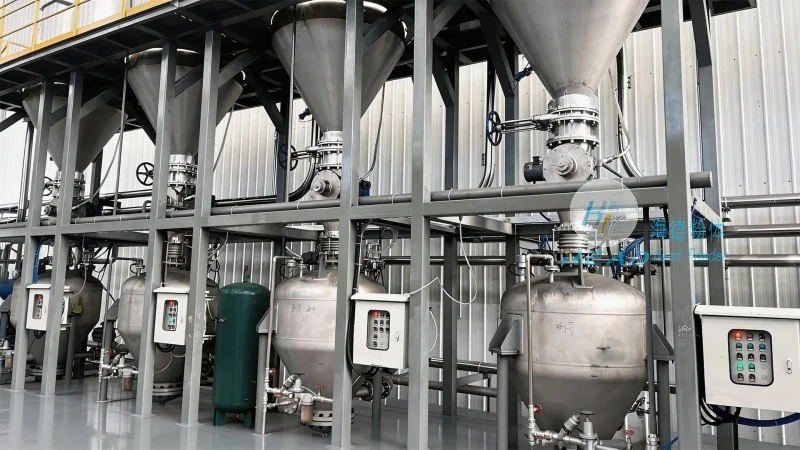
Hybrid systems combine elements of both dilute and dense phase technologies to provide flexibility and adaptability to varying operational conditions. These systems can switch between dilute and dense phase modes based on the specific requirements of the coal handling process. For instance, a hybrid system might use a dilute phase for the initial portion of the pipeline to achieve high throughput, then transition to a dense phase for the final segment to ensure gentle handling and minimal product degradation. The ability to adjust the conveying mode dynamically allows for optimized energy consumption and operational efficiency, making hybrid systems a versatile choice for complex coal transport applications.
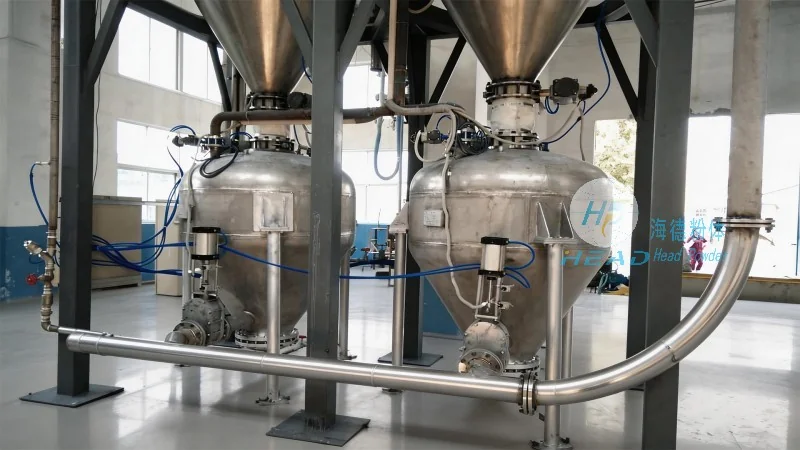
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for the coal and bulk material handling industries. With a focus on innovation and customer-centric design, the company has developed and implemented advanced pneumatic conveying systems tailored to the unique needs of its clients. Headpowder's expertise lies in the integration of cutting-edge technology with practical application, ensuring that each system is optimized for performance, reliability, and cost-effectiveness. The company's commitment to quality and service has established it as a trusted partner in the development of efficient coal transport solutions.
Headpowder is headquartered in Shandong, China, with a dedicated team of engineers and technicians dedicated to delivering high-quality engineering services. The company's facilities are equipped with state-of-the-art equipment and testing capabilities, enabling the design and fabrication of customized pneumatic conveying systems that meet the most stringent industry standards. By leveraging local expertise and resources, headpowder ensures that its solutions are both technologically advanced and economically viable for a wide range of industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top