With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in providing advanced solutions for the efficient and reliable transport of coal ash. With a focus on innovative engineering and robust system design, the company has established itself as a leading provider in the field of pneumatic conveying technology for industrial applications. This article explores the key aspects of coal ash pneumatic conveying systems, highlighting the technical features, operational benefits, and the company's expertise in delivering tailored solutions for various industrial needs.
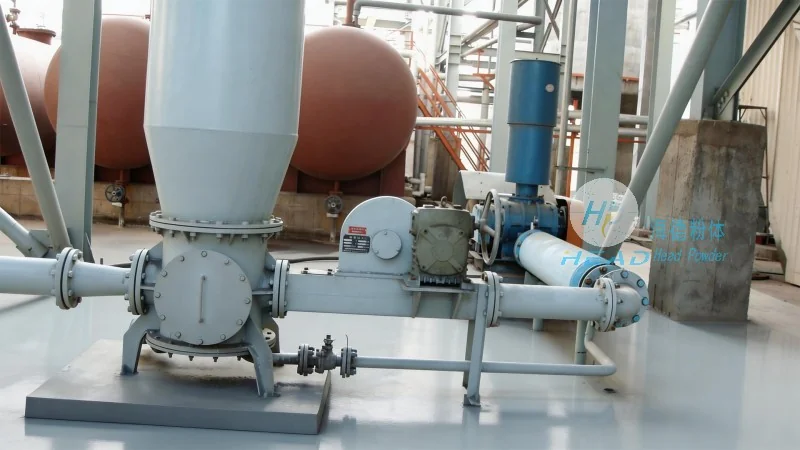
Coal ash, a byproduct of coal combustion in power plants and industrial facilities, requires effective handling and transportation for disposal or reuse. Traditional methods such as belt conveyors or bucket elevators may face challenges with dust generation, material degradation, and operational inefficiencies. Pneumatic conveying offers a superior alternative by utilizing air pressure to transport fine powders like coal ash through pipelines, minimizing environmental impact and ensuring safe handling. The system typically consists of a blower, a hopper for material storage, and a pipeline network that facilitates the movement of ash from the source to the destination, such as storage silos or treatment facilities.
The coal ash pneumatic conveying system developed by headpowder incorporates several critical components that work in harmony to ensure optimal performance. The primary components include a high-efficiency blower or compressor, which generates the necessary air pressure to move the ash through the pipeline. The material hopper, equipped with a feeder or rotary valve, controls the flow of coal ash into the system, preventing blockages and maintaining consistent material feed. The pipeline network, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of coal ash and ensure long-term durability. Additionally, the system may include filters and cyclones to separate air from the ash at the receiving end, allowing for clean air discharge and ash collection.
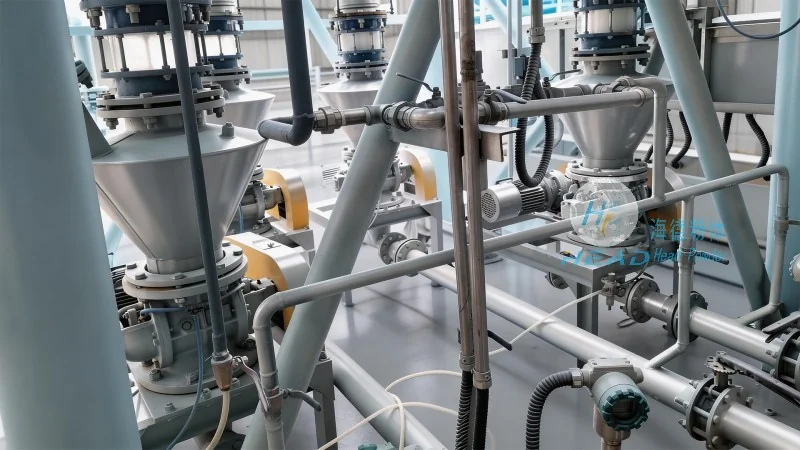
Implementing a pneumatic conveying system for coal ash offers numerous advantages over conventional transport methods. Firstly, it significantly reduces dust emissions, enhancing workplace safety and compliance with environmental regulations. The enclosed pipeline system prevents ash from being released into the environment, minimizing the risk of contamination and improving air quality. Secondly, the system provides a more efficient and flexible method of transporting ash over long distances or through complex layouts, as pipelines can be easily routed around obstacles and integrated into existing infrastructure. Thirdly, pneumatic conveying reduces labor costs by automating the material handling process, eliminating the need for manual loading and unloading of ash. Furthermore, the technology allows for precise control over the flow rate and pressure, ensuring consistent performance and preventing system overloads or blockages. These benefits make pneumatic conveying an ideal solution for power plants and industrial facilities seeking to optimize their ash management processes.
headpowder recognizes that each industrial facility has unique requirements for coal ash handling, and therefore offers customized pneumatic conveying solutions tailored to specific needs. The company works closely with clients to assess their operational parameters, such as ash volume, particle size, and distance to be covered, to design a system that meets both performance and budgetary constraints. Whether for small-scale applications or large-scale power plant operations, the systems can be scaled to accommodate varying throughput rates, from low to high volume. The modular design of the components allows for easy expansion or modification as operational needs evolve, ensuring long-term investment value. Additionally, the company provides comprehensive technical support and maintenance services to ensure the system operates at peak efficiency throughout its lifecycle.
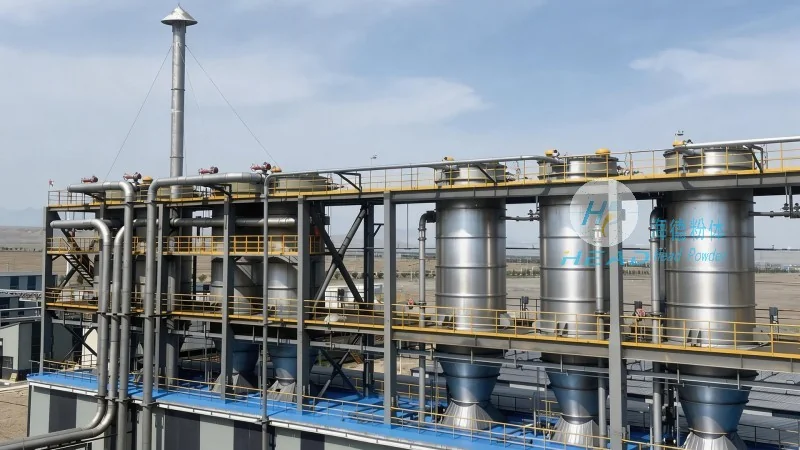
Successful implementation of a coal ash pneumatic conveying system requires careful consideration of several operational factors. Proper material preparation, such as drying and sieving, is essential to ensure consistent particle size and prevent agglomeration, which can lead to system blockages. Regular maintenance of the blower, feeder, and pipeline components is crucial to prevent wear and tear and maintain optimal performance. Monitoring air pressure and flow rates continuously helps identify potential issues early, allowing for timely interventions. Training operators on the proper use and maintenance of the system is also vital to ensure safe and efficient operation. By adhering to these best practices, industrial facilities can maximize the lifespan of their pneumatic conveying equipment and minimize downtime.
Coal ash pneumatic conveying systems, as provided by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated and efficient solution for the transportation of coal ash in industrial settings. By leveraging advanced pneumatic technology, the systems offer significant advantages in terms of safety, environmental compliance, and operational efficiency. With a commitment to customization and long-term support, headpowder continues to be a trusted partner for power plants and industrial facilities seeking to optimize their ash management processes. The company's expertise in engineering and manufacturing ensures that each system is tailored to meet the specific needs of the client, delivering reliable and sustainable solutions for the future.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top