With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Mobile powder pneumatic conveying systems are advanced industrial equipment designed to transport bulk powder materials efficiently and safely. These systems are particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where precise handling of powders is critical. The operation of a mobile system involves several key components and steps that ensure smooth and reliable material transfer.

At the core of a mobile powder pneumatic conveying system are several essential components that work in tandem to facilitate material transport. The primary components include a hopper for material storage, a conveyor line that may be flexible or rigid depending on the system design, a blower or compressor to generate the air flow, and a control system to regulate pressure and flow rates. Additionally, the system may feature filters to capture dust and maintain air quality, as well as valves and regulators to control the direction and speed of material movement. The mobility of these systems is achieved through a robust chassis with wheels or tracks, allowing for easy relocation between different production sites or storage areas. These systems are designed and manufactured by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading provider of industrial material handling solutions.
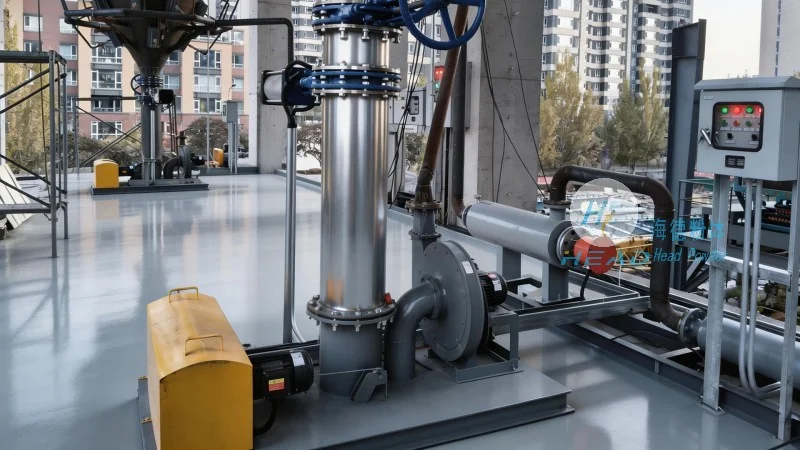
The operation process of a mobile powder pneumatic conveying system begins with the loading of the hopper with the target powder material. Once the hopper is filled, the control system activates the blower, which generates a high-pressure air stream. This air stream is then directed through the conveyor line, creating a vacuum or pressure differential that draws the powder particles into the system. As the air flows through the line, it carries the powder particles along, ensuring that they are transported to the desired destination, such as a processing unit or a storage silo. The system's control panel allows operators to adjust parameters like air pressure and flow rate to optimize the conveying efficiency and prevent material blockages. The mobile design enables quick setup and operation at various locations, making it ideal for temporary or on-site applications where fixed infrastructure may not be available.
The working principle of mobile powder pneumatic conveying systems is based on the fundamental concept of pneumatic transport, where air is used as the medium to move solid particles. In a pressure system, the blower supplies compressed air that forces the powder through the conveyor line, while in a vacuum system, the blower creates a negative pressure that pulls the powder into the line. The efficiency of the system depends on factors such as the particle size, density, and moisture content of the material, as well as the air velocity and pressure. Proper design of the conveyor line, including the use of bends and elbows, is crucial to maintain the flow of material and prevent clogging. The control system monitors the pressure and flow rates in real-time, providing feedback to adjust the operation as needed. This dynamic control ensures that the system operates within optimal parameters, minimizing energy consumption and maximizing material throughput. The mobility of the system also allows for flexible integration with existing production lines, enabling seamless material transfer without the need for extensive modifications to the facility.
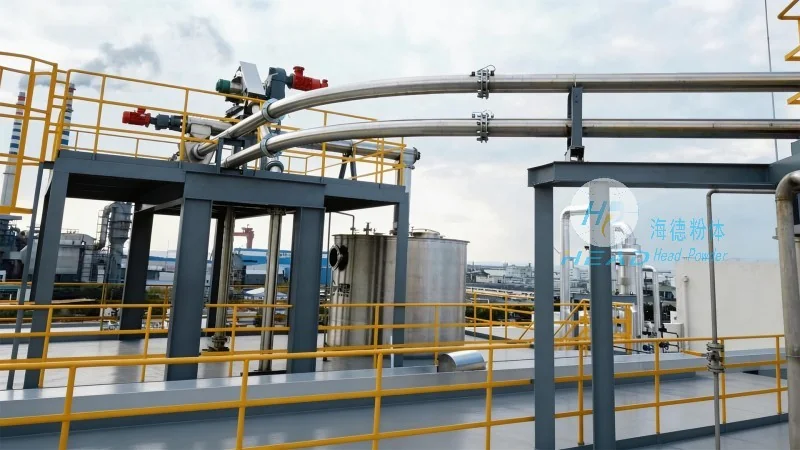
Mobile powder pneumatic conveying systems offer several advantages over traditional bulk material handling methods. Their mobility allows for easy relocation, making them suitable for temporary projects or sites with changing production needs. The systems are also compact and can be installed in confined spaces, reducing the footprint required for material handling. Additionally, the pneumatic transport method minimizes material contamination and degradation, as the powder is not in direct contact with mechanical components. This is particularly important in industries where product purity is paramount, such as pharmaceuticals and food processing. The systems are also capable of handling a wide range of powder types, from fine powders to bulkier materials, with adjustable settings to accommodate different material characteristics. In applications such as pharmaceutical manufacturing, these systems are used to transport active ingredients and excipients to production lines, ensuring precise dosing and consistent quality. In the food industry, they are employed to move ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. The chemical industry also benefits from these systems, as they can handle corrosive or hazardous powders safely, with proper filtration and containment measures.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top