With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The air-driven conveying system for heptahydrate magnesium sulfate material is a specialized solution designed to efficiently transport this specific chemical compound. Developed by Shandong HeadPowder Engineering Co., Ltd., this system leverages pneumatic technology to move the material from one location to another, ensuring high efficiency and minimal loss. The system is particularly suited for industrial applications where the safe and reliable handling of heptahydrate magnesium sulfate is critical.
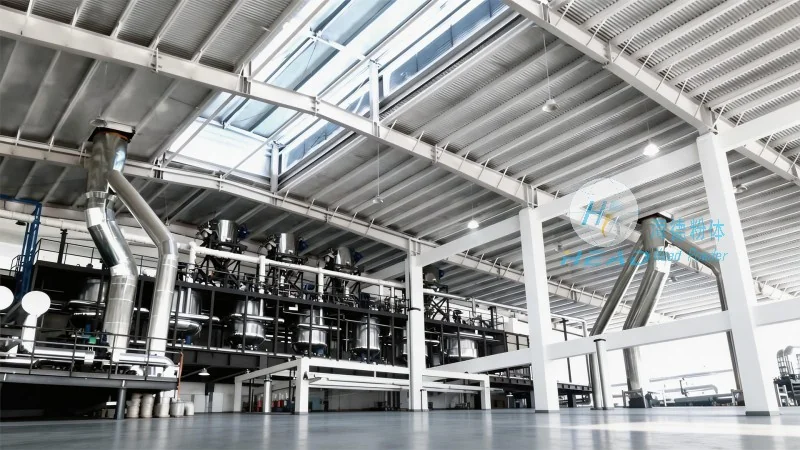
The core principle of the air-driven conveying system involves the use of compressed air to create a flow that propels the heptahydrate magnesium sulfate particles through a pipeline. The system typically consists of a hopper, a rotary airlock valve, a conveying line, and a receiver. As material is fed into the hopper, it is drawn into the conveying line by the air flow. The rotary airlock valve controls the discharge of material from the hopper into the system, preventing backflow and ensuring a consistent feed rate. The compressed air, often supplied by a blower or compressor, provides the necessary pressure to move the material through the pipeline. The receiver at the end of the line collects the material, allowing for its discharge into the next processing stage. This pneumatic method offers advantages such as reduced mechanical wear, lower maintenance requirements, and the ability to handle materials that are difficult to transport via traditional methods.
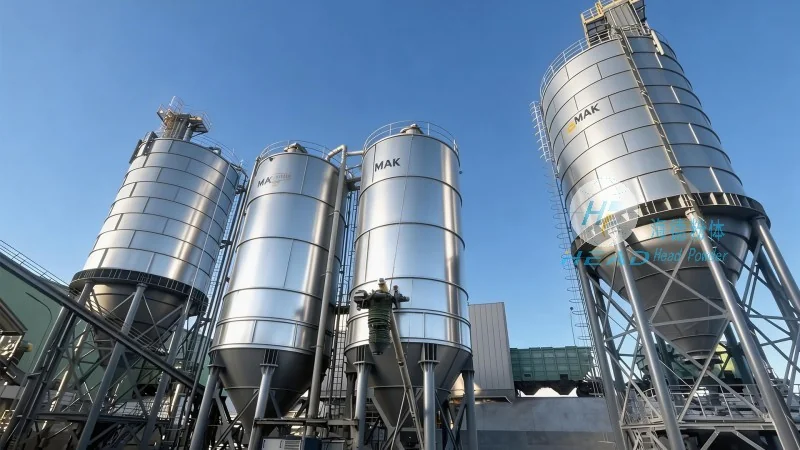
The air-driven conveying system for heptahydrate magnesium sulfate is optimized for specific working environments and operational requirements. One key characteristic is its adaptability to various industrial settings, including chemical plants, pharmaceutical facilities, and mining operations where heptahydrate magnesium sulfate is used as a raw material or intermediate product. The system is designed to handle the unique properties of heptahydrate magnesium sulfate, such as its hygroscopic nature and potential for dust generation. The conveying process is controlled to minimize dust exposure, which is crucial for maintaining a safe working environment and complying with occupational health and safety regulations. Additionally, the system's flexibility allows it to be integrated into existing production lines, reducing downtime and improving overall operational efficiency. The working scene characteristics also include the ability to handle varying material flow rates, from low to high throughput, making it suitable for both small-scale and large-scale production applications. The system's design ensures that it can operate continuously without frequent stops, which is essential for maintaining production schedules and meeting demand.
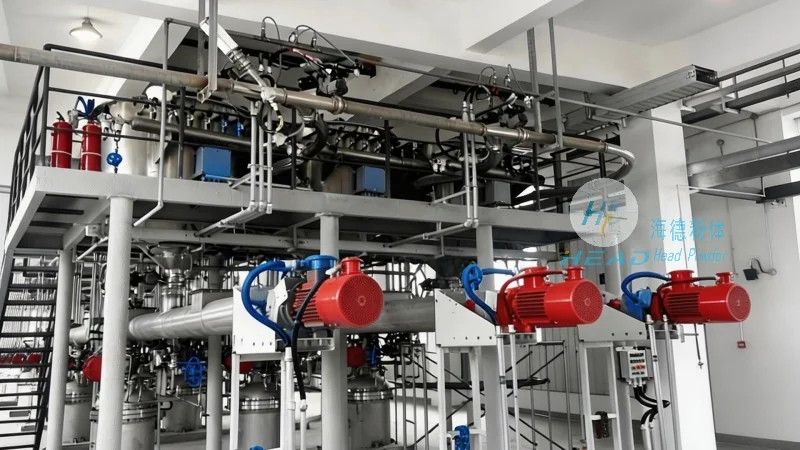
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of engineering solutions for material handling and processing. With a focus on innovative and efficient systems, the company has developed the air-driven conveying system for heptahydrate magnesium sulfate as part of its commitment to delivering high-quality solutions to its clients. The company's expertise lies in understanding the specific needs of industries dealing with chemical compounds and providing tailored solutions that address their unique challenges. Based in Shandong, China, HeadPowder has a strong presence in the domestic and international markets, serving a wide range of clients across various sectors. The company's team of engineers and technicians brings years of experience in designing and implementing material handling systems, ensuring that each project is executed with precision and attention to detail. By leveraging advanced technology and rigorous testing, HeadPowder ensures that its systems meet the highest standards of performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top