With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. The intelligent centralized powder pneumatic conveying equipment is a sophisticated solution that integrates modern technology to optimize the transport of bulk powders efficiently and reliably. This equipment is engineered to meet the diverse needs of industries such as food, pharmaceuticals, chemicals, and manufacturing, where precise and hygienic material handling is critical.
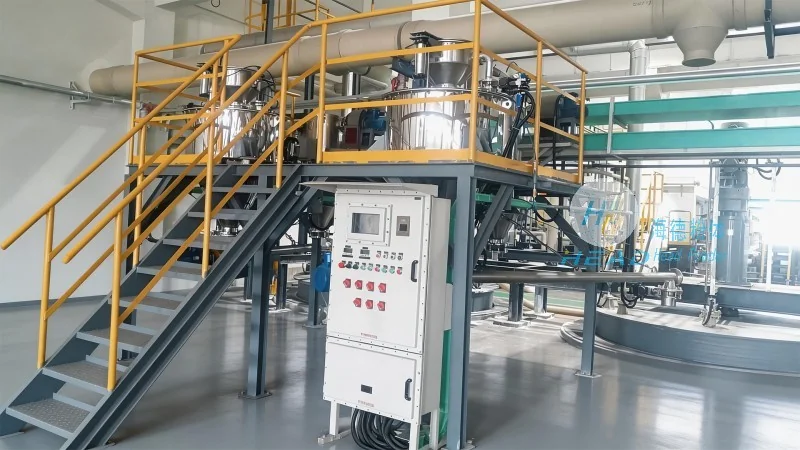
The fundamental principle of the intelligent centralized powder pneumatic conveying system is the use of air as the medium to transport powders through a network of pipes. Unlike traditional mechanical conveying methods, this system utilizes positive or negative pressure to move materials, ensuring minimal product degradation and contamination. The intelligent features embedded in the equipment enhance operational efficiency by automating processes, monitoring performance, and providing real-time data for better decision-making. The system typically includes components like feeders, conveying lines, separation units, and control panels, all coordinated by advanced software to maintain optimal pressure, flow, and material distribution.
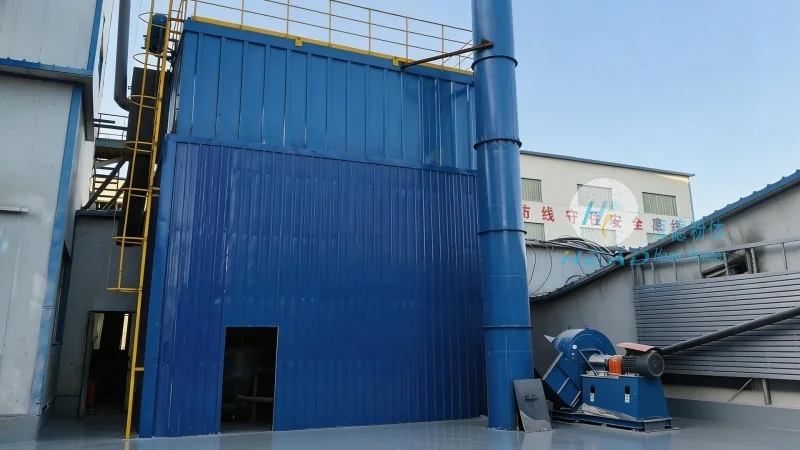
The intelligent centralized powder pneumatic conveying equipment comprises several critical components that work in harmony to achieve seamless material transport. The feeders are responsible for accurately metering the powder into the conveying line, ensuring consistent flow rates. The conveying lines, often made of stainless steel or other corrosion-resistant materials, are designed to withstand the abrasive nature of powders and maintain hygiene standards. The separation units, including cyclones and filters, are crucial for separating the conveyed powder from the air stream, preventing dust emissions and ensuring product purity. The control panels, equipped with user-friendly interfaces, allow operators to monitor and adjust system parameters, such as pressure, temperature, and flow rates, to adapt to varying production demands. Additionally, the system may incorporate sensors and IoT devices to collect data on performance, energy consumption, and maintenance needs, enabling predictive maintenance and reducing downtime.
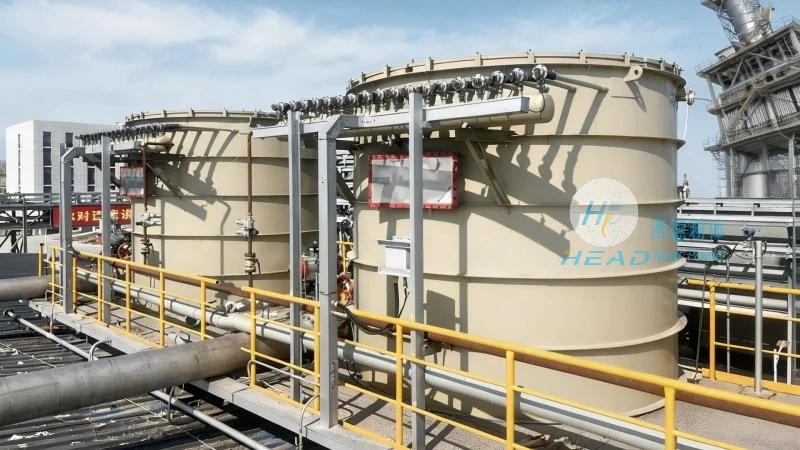
The intelligent centralized powder pneumatic conveying equipment is widely applicable across various industries, each benefiting from its unique features. In the food industry, for example, the system ensures hygienic and contamination-free transport of ingredients like flour, sugar, and spices, maintaining product quality and safety standards. The pharmaceutical sector utilizes this equipment to handle active pharmaceutical ingredients (APIs) and excipients with high precision, minimizing the risk of cross-contamination and ensuring compliance with regulatory requirements. In the chemical industry, the system efficiently transports bulk chemicals, including powders and granules, while maintaining safety protocols and preventing dust explosions. Manufacturing industries, such as plastics and ceramics, benefit from the equipment's ability to handle abrasive and high-volume powders, improving production throughput and reducing labor costs. The key benefits of this equipment include improved process efficiency, reduced material loss, enhanced safety, and lower operational costs due to its automated and intelligent features.
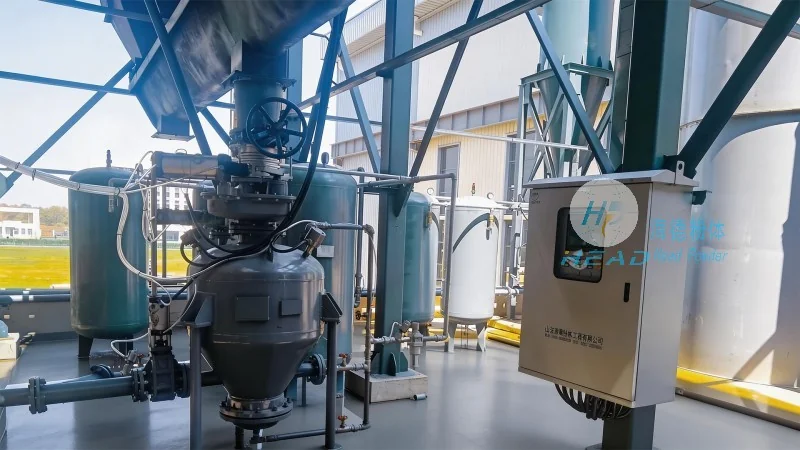
Implementing the intelligent centralized powder pneumatic conveying equipment offers several operational advantages that contribute to overall business success. The system's ability to handle high volumes of powders with minimal human intervention reduces labor costs and improves productivity. The automated control system ensures consistent performance, minimizing variations in material flow and quality. The real-time monitoring and data analysis capabilities enable operators to identify and address issues promptly, reducing downtime and maintenance costs. Performance metrics, such as conveying efficiency, energy consumption per ton of material, and system reliability, are significantly improved compared to traditional methods. The equipment's modular design allows for easy expansion or modification to accommodate changing production needs, providing long-term value and adaptability. Additionally, the system's compliance with international standards, such as FDA and GMP, ensures that it meets the stringent requirements of industries where product safety and quality are paramount.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top