With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for various industrial applications. This article delves into the fundamental principles behind borax powder pneumatic conveying systems and highlights the key characteristics of their operational environments.
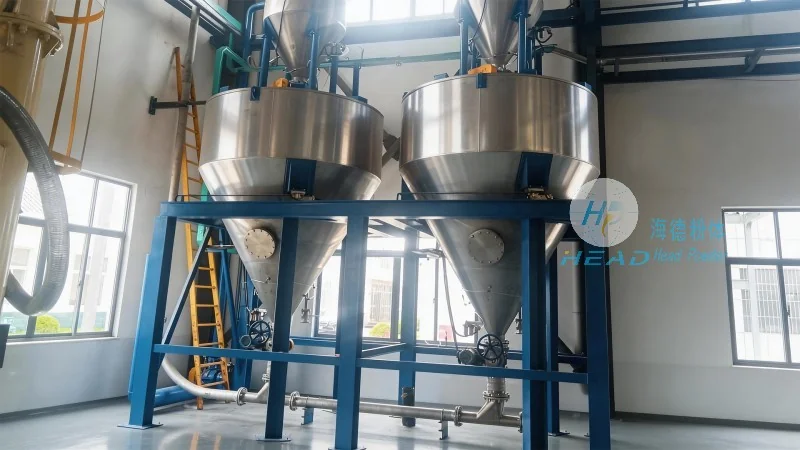
Borax powder pneumatic conveying systems operate on the principle of transporting bulk materials through a pipeline using a gas stream, typically air or a mixture of air and other gases. The system consists of several core components, including a material hopper, a rotary feeder, a venturi or eductor, a pipeline network, and a dust collector or filter system. The process begins when the borax powder is fed into the hopper, where it is then metered by the rotary feeder into the conveying line. As the material enters the venturi, the high-velocity gas stream creates a negative pressure that draws the powder particles into the pipeline, ensuring efficient and continuous transport. The system is designed to maintain consistent flow rates and pressure differentials to prevent blockages and ensure reliable operation. The use of appropriate gas velocities and pipeline diameters is critical to achieving optimal performance, minimizing material degradation, and reducing energy consumption.
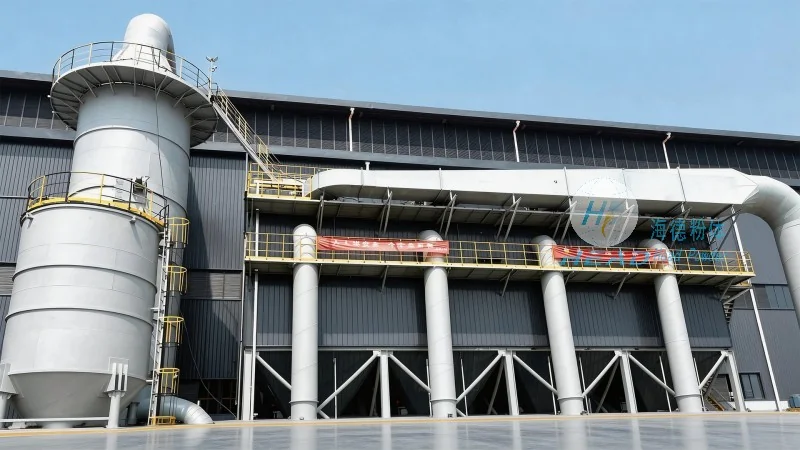
The operational environments for borax powder pneumatic conveying systems vary widely depending on the specific industrial application. These systems are commonly used in chemical processing plants, pharmaceutical manufacturing facilities, and food processing industries where the handling of fine powders requires high precision and minimal contamination. In chemical processing, the systems are often integrated into production lines for the transportation of borax from storage silos to reaction vessels or packaging units. The key characteristics of these working scenes include high cleanliness standards, as borax is a critical raw material in many chemical formulations. The systems must also be capable of handling varying particle sizes and moisture content, which can affect the flow characteristics and system efficiency. In pharmaceutical and food processing applications, the systems are subject to stringent regulatory requirements regarding material purity and equipment hygiene. This necessitates the use of stainless steel components, advanced filtration systems, and automated control mechanisms to ensure compliance with industry standards. Additionally, the working environments may involve multiple processing stages, requiring the integration of multiple conveying lines and material handling equipment to streamline production processes.
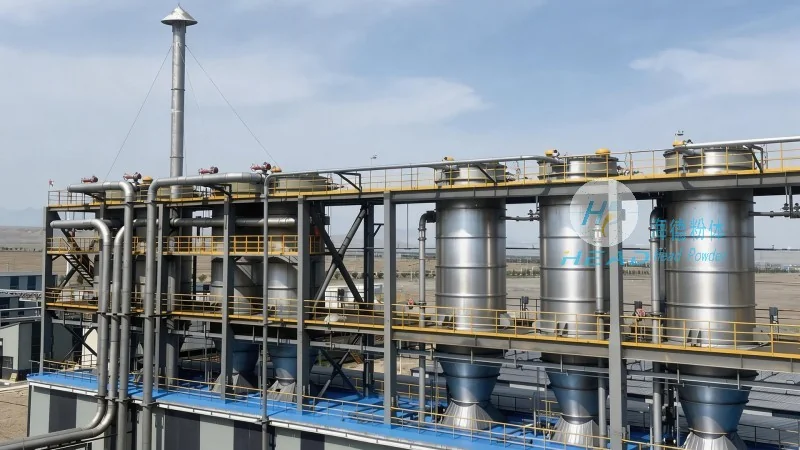
HeadPowder's borax powder pneumatic conveying systems are engineered to provide several key advantages that enhance operational efficiency and product quality. One of the primary benefits is the ability to transport materials over long distances without the need for intermediate storage or manual handling. This reduces the risk of material contamination and improves overall production throughput. The systems also offer flexibility in terms of layout and integration, allowing them to be customized to fit the specific spatial constraints of a facility. Advanced control systems enable real-time monitoring of flow rates, pressure, and temperature, providing operators with immediate feedback and the ability to adjust system parameters as needed. This proactive approach to system management minimizes downtime and ensures consistent performance. Furthermore, the use of energy-efficient designs, such as variable frequency drives and optimized pipeline configurations, helps to reduce operational costs while maintaining high levels of performance. The systems are also designed for easy maintenance and cleaning, with features like quick-release connections and accessible filter components that simplify routine upkeep and extend equipment lifespan.
The practical application of borax powder pneumatic conveying systems can be observed in various industrial settings. For instance, in a chemical plant producing detergents, the system efficiently transports borax from bulk storage to mixing tanks, ensuring precise dosing and consistent product quality. In a pharmaceutical manufacturing facility, the system handles borax powder for the production of antacids and other over-the-counter medications, where contamination control is paramount. The reliability and efficiency of these systems contribute significantly to the overall productivity and cost-effectiveness of these operations. By eliminating manual handling and reducing the risk of material loss or degradation, the systems help to maintain high standards of quality control and regulatory compliance. The impact of these systems extends beyond individual plants, as they support the broader supply chain by ensuring a steady and reliable flow of raw materials to production facilities. This, in turn, enhances the competitiveness of companies operating in industries that rely on borax as a key component.
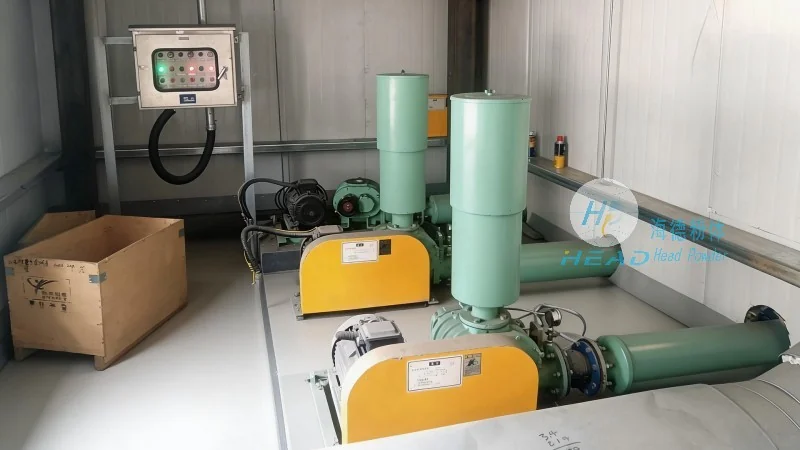
HeadPowder's expertise in designing and implementing borax powder pneumatic conveying systems reflects a commitment to delivering innovative solutions that meet the evolving needs of industrial applications. The principles and characteristics outlined in this article demonstrate the effectiveness of these systems in improving operational efficiency, maintaining product quality, and reducing costs. As industrial processes continue to demand higher precision and reliability, the role of advanced material handling systems like pneumatic conveyors will remain critical. Future developments may focus on integrating more sophisticated control technologies, such as artificial intelligence and machine learning, to optimize system performance and predictive maintenance. Additionally, the adoption of sustainable practices, such as using recycled materials and energy-efficient designs, will likely become more prominent in the design of new systems. HeadPowder remains at the forefront of these advancements, continuing to provide tailored solutions that enhance the competitiveness and sustainability of its clients' operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top