With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pumps, also known as pressure-type pneumatic conveyors, are advanced industrial equipment designed for efficient bulk material transport. These systems are widely used in various industries due to their ability to handle a wide range of materials, including powders, granules, and fine particles. The core principle of bin pump operation involves creating a pressure differential between the hopper and the discharge point, enabling the material to be conveyed through a pipeline network.
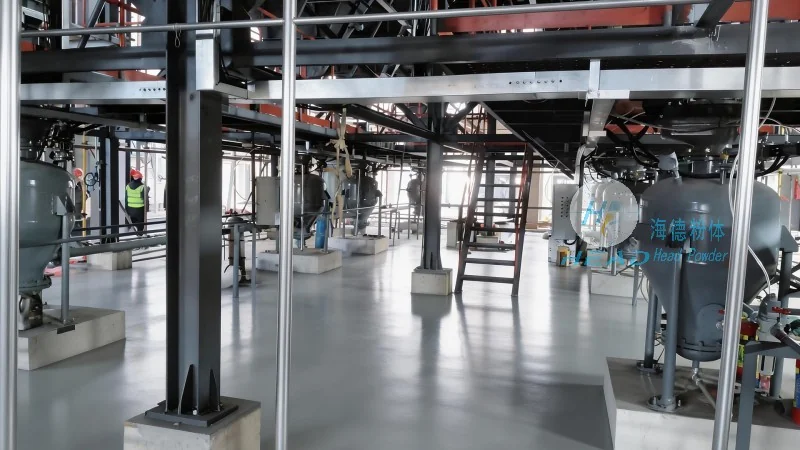
The operation of a bin pump material handling system is based on the principles of fluid dynamics and pneumatic technology. The system typically consists of a hopper where the material is stored, a compressor that generates the necessary air pressure, and a pipeline network that transports the material to the discharge point. When the system is activated, the compressor draws air from the hopper and compresses it, creating a high-pressure air stream. This air stream carries the material particles through the pipeline, ensuring a consistent and controlled flow. The pressure differential between the hopper and the discharge point is maintained by the compressor, which adjusts its output to match the system's requirements. The bin pump's design allows for flexible and adjustable conveying speeds, making it suitable for different material types and application needs.
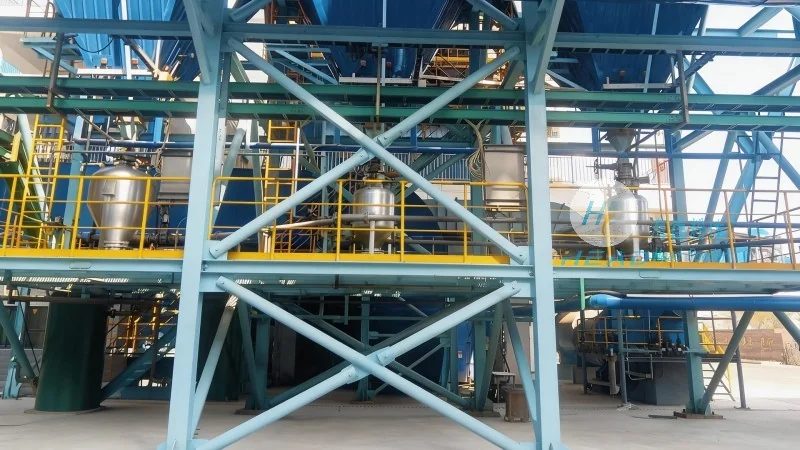
Bin pump material handling systems offer several key features that make them ideal for industrial applications. One of the primary advantages is their ability to handle a wide variety of materials, from fine powders to coarse granules, without causing segregation or degradation. The system's design minimizes material degradation due to its low shear and gentle handling, which is crucial for sensitive materials like pharmaceuticals or food products. Additionally, bin pumps are highly efficient in terms of energy consumption and space utilization. They can transport materials over long distances with minimal energy input, and their compact design allows for installation in limited spaces. The system's flexibility is another significant advantage, as it can be easily integrated with existing infrastructure and adapted to changing production needs. This adaptability makes bin pumps a cost-effective solution for industries requiring versatile material handling solutions.
Bin pump material handling systems are employed in a variety of industrial working scenes, each tailored to specific operational requirements. In the chemical industry, bin pumps are used to transport raw materials and finished products, such as powders and granules, between processing units. The system's ability to handle abrasive and corrosive materials makes it suitable for chemical processing plants. In the food and beverage industry, bin pumps are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and efficient handling. The system's gentle handling and low contamination risk are critical for maintaining product quality and compliance with industry standards. In the mining and minerals industry, bin pumps are used to transport ore and other bulk materials from mines to processing facilities. The system's high capacity and durability make it ideal for heavy-duty applications. Additionally, in the pharmaceutical industry, bin pumps are used to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring precise and controlled handling. The system's ability to maintain a sterile environment and prevent cross-contamination is essential for pharmaceutical production.
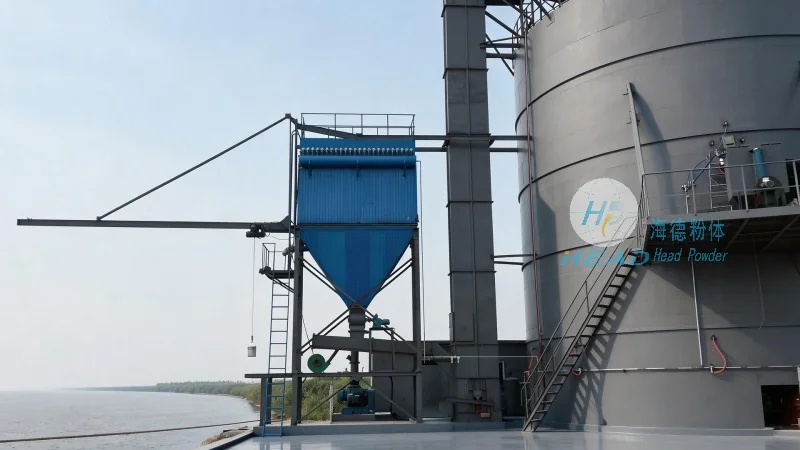
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of bin pump material handling systems. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality industrial equipment. HeadPowder specializes in designing and manufacturing customized bin pump systems that meet the specific needs of various industries. The company's products are known for their reliability, efficiency, and durability, making them a preferred choice for industrial applications. HeadPowder's team of engineers and technicians is dedicated to providing innovative solutions and excellent customer service. The company adheres to international quality standards and continuously invests in research and development to improve its products and stay ahead of industry trends. With a strong commitment to customer satisfaction and quality, HeadPowder has built a reputation as a reliable partner for industries requiring efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top