With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder Engineering, based in Shandong, China, specializes in the design and implementation of efficient material conveying solutions for industrial applications. This article explores the fundamental principles behind sintered ash material conveying systems, detailing their operational mechanisms and the specific characteristics of their working environments.
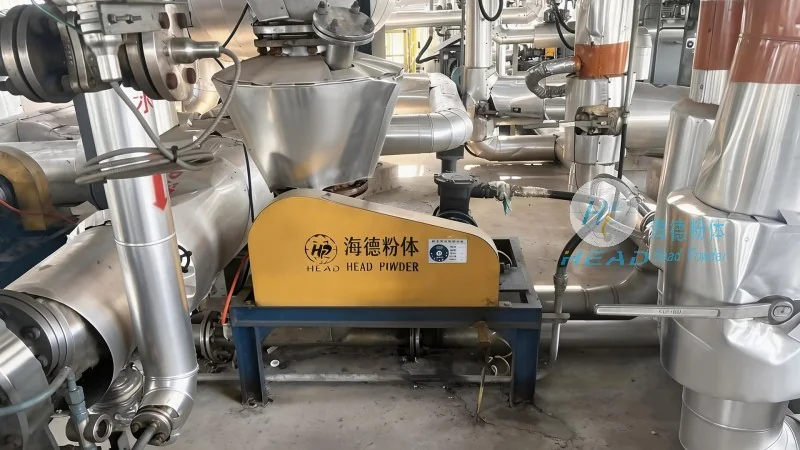
The sintered ash material conveying system typically comprises several key components that work in tandem to ensure reliable material transport. At the core of the system is the conveyor equipment, which may include belt conveyors, screw conveyors, or pneumatic conveying systems, depending on the material properties and process requirements. The system is equipped with a control panel that monitors and regulates the conveying process, ensuring consistent flow rates and preventing blockages or overloads. Additionally, the system may incorporate sensors and safety features to enhance operational safety and efficiency.
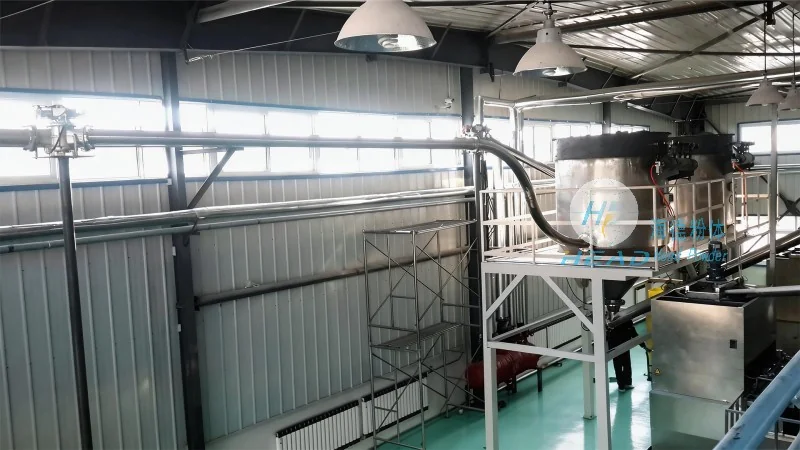
One of the primary characteristics of sintered ash material conveying systems is their ability to handle abrasive and high-volume materials with minimal maintenance. The design of the conveyor components, such as heavy-duty belts and robust housing, is optimized to withstand the harsh conditions associated with sintered ash, which often contains fine particles and can be corrosive. The system's flexibility in accommodating different material types and flow rates makes it suitable for various industrial settings, from steel mills to cement plants.
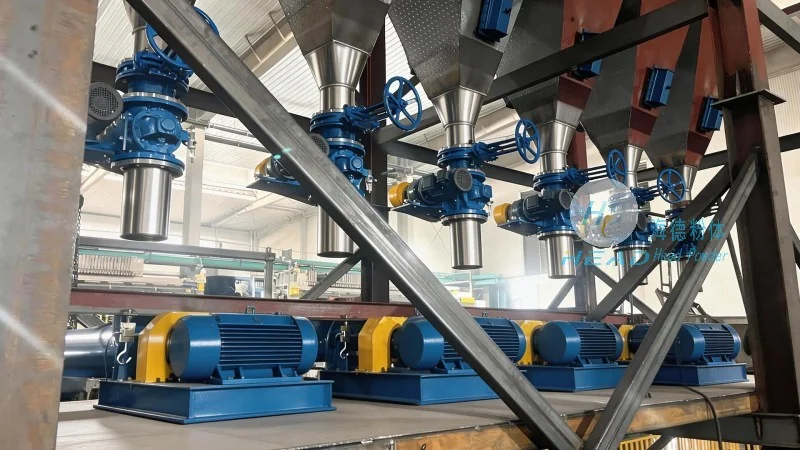
The working scene characteristics of sintered ash material conveying systems are defined by their adaptability to diverse industrial environments. In steel production facilities, for example, these systems are crucial for transporting sintered ash from the sintering process to storage or further processing units. The system's ability to maintain a consistent flow rate under varying load conditions ensures that downstream processes, such as material handling or recycling, operate smoothly. In cement manufacturing, the conveying system efficiently moves sintered ash to the raw material preparation stage, contributing to overall production efficiency. The system's design also minimizes material loss and dust emission, aligning with environmental regulations and operational safety standards.
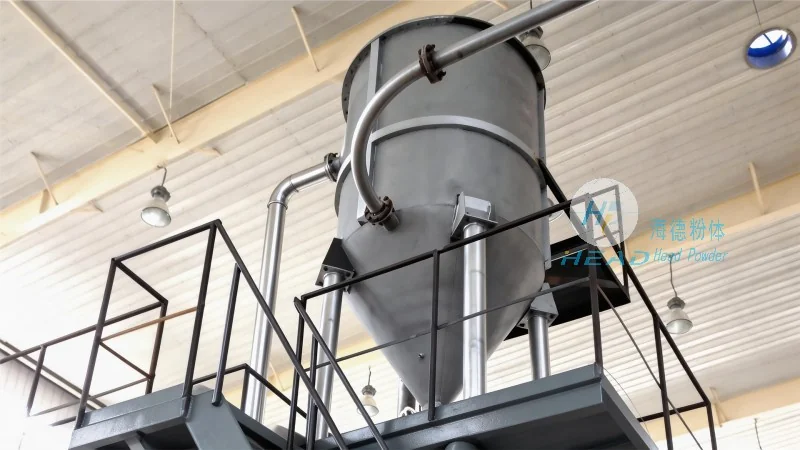
HeadPowder Engineering, with its headquarters in Shandong, China, provides comprehensive solutions for sintered ash material conveying systems, combining advanced technology with practical application expertise. The company's commitment to quality and reliability ensures that its systems meet the demanding requirements of modern industrial operations. By understanding the principles and working characteristics of these systems, industries can optimize their material handling processes, reduce operational costs, and enhance overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top