

Principles and Working Scene Characteristics of Sugar Material Conveying Systems
For sugar processing facilities, the efficient and reliable transportation of sugar materials is a critical operational requirement. The sugar material conveying system plays a pivotal role in ensuring smooth production workflows, from raw sugar handling to final product packaging. Understanding the principles and characteristics of these systems is essential for optimizing plant performance and maintaining consistent quality standards.
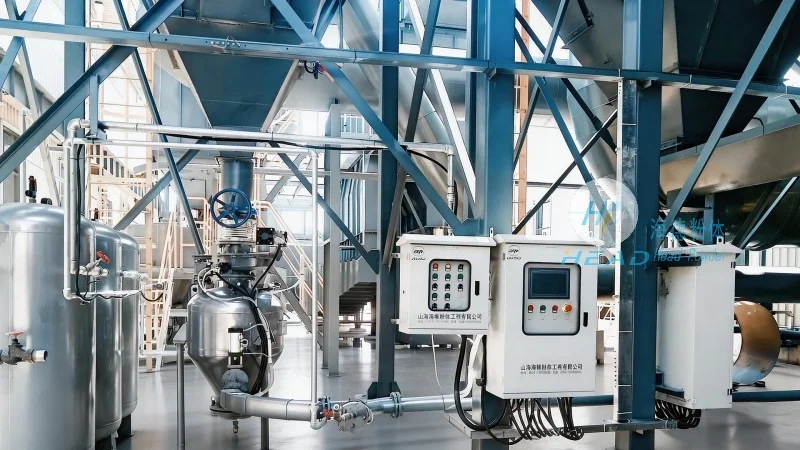
Overview of Sugar Material Conveying Systems
The sugar material conveying system is designed to handle various forms of sugar, including raw sugar, refined sugar, and sugar derivatives. These systems are engineered to transport bulk materials over long distances or vertical heights with minimal loss and maximum efficiency. Key components typically include feeders, conveyors, elevators, and control systems that work in tandem to manage the flow of sugar through the processing plant.
Core Principles of Operation
The fundamental principle of sugar material conveying systems is to maintain a consistent and controlled flow of material. This involves precise control of speed, pressure, and temperature to prevent caking, bridging, or degradation of the sugar product. Advanced control systems often integrate sensors and feedback mechanisms to adjust operational parameters in real-time, ensuring optimal performance under varying load conditions. For instance, in raw sugar handling, the system must accommodate high moisture content and abrasive properties, requiring robust materials of construction and specialized sealing technologies.
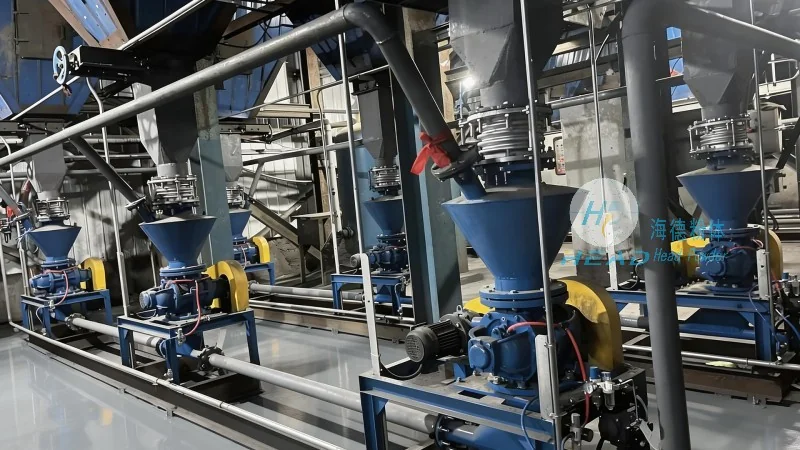
Working Scene Characteristics
The working scene characteristics of sugar material conveying systems are shaped by the specific demands of the processing environment. In industrial sugar plants, these systems operate in high-temperature and high-humidity conditions, often with continuous 24/7 operation. The design must account for factors such as dust generation, material variability, and the need for easy maintenance and cleaning. In addition, the system must be compatible with downstream processing equipment, such as refining units or packaging lines, ensuring seamless integration and minimal downtime. The working scene also includes considerations for safety, as sugar dust can be a fire hazard, and the system must incorporate explosion-proof features and dust suppression measures to mitigate risks.
Application Scenarios in Sugar Processing
Sugar material conveying systems are widely used across different stages of sugar production. In the raw sugar processing stage, the system handles large volumes of raw sugar from storage silos to the refining equipment. During the refining process, it transports refined sugar from crystallizers to drying ovens or packaging stations. For sugar derivatives like sugar syrups or molasses, specialized conveying systems are employed to manage viscous and sticky materials, often using screw conveyors or pneumatic systems to prevent blockages. Each application scenario requires tailored solutions to address unique material properties and operational constraints.
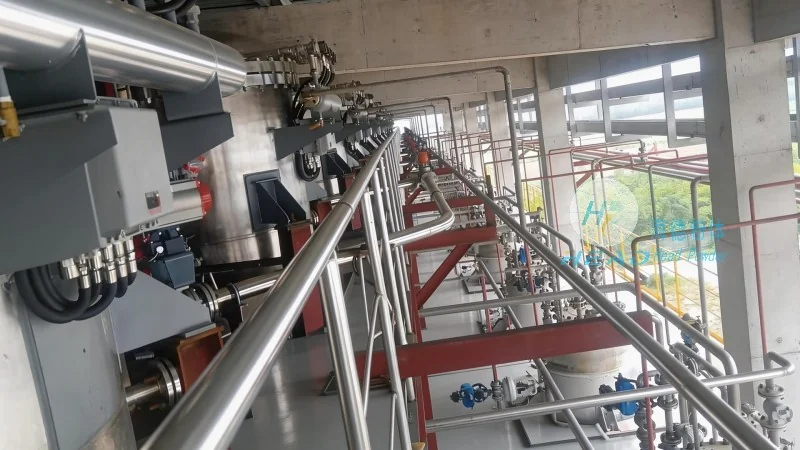
Technical Advancements and Efficiency
Modern sugar material conveying systems incorporate advanced technologies to enhance efficiency and reduce operational costs. Automated control systems, equipped with IoT sensors, enable real-time monitoring and predictive maintenance, minimizing downtime and extending equipment lifespan. Energy-efficient designs, such as variable speed drives and optimized conveyor layouts, reduce power consumption while maintaining performance. Additionally, the use of high-quality materials, such as stainless steel and food-grade plastics, ensures compliance with hygiene standards and prevents contamination of the sugar product. These advancements not only improve operational efficiency but also contribute to environmental sustainability by reducing waste and energy usage.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of specialized conveying systems for the sugar industry. With a strong presence in China, the company has built a reputation for delivering high-quality, customized solutions tailored to the unique needs of sugar processing facilities. HeadPowder’s expertise lies in designing and manufacturing systems that meet stringent industry standards, ensuring reliability, durability, and optimal performance. The company’s commitment to innovation and customer satisfaction has made it a trusted partner for sugar manufacturers worldwide.